
Key Takeaways
The question behind OEE on an SMT line: where the line loses time and good boards, from changeovers, short stops at feeders and nozzles, and rework.
The platforms start from different places: material flow and traceability, a full MES for complex routings, machine data across SMT vendors, or a light MES focused on OEE and downtime.
How to read this page: the five platforms are listed alphabetically, not ranked. Each comes with the trade-off you accept when you choose it, including Fabrico, which publishes this page.
Measuring OEE on an SMT line looks simple until you try it: the line runs at the pace of its bottleneck, short stops hide inside "running", and a reworked board still leaves the line. The platforms below handle that in different ways, and they also differ in what else they take on, from material verification to full order routing. This page puts their focus and their trade-offs side by side. For the wider market, see our comparison of the best OEE software.
Starting point: what the platform was built to solve first on an electronics line.
Machine data: how stops, counts and reasons reach the system.
Material and traceability: whether the platform verifies reels and records genealogy, or leaves that to other systems.
What the rollout asks of the plant: a line by line start, or a broader MES project.
Where it fits: plants where material flow and traceability around the machines are the main concern.
Cogiscan is known for its track, trace and control middleware, which connects SMT machines and follows material around them. OEE comes from the same connectivity layer.
Strengths:
A focus on material flow, so setup and material waits become visible.
Traceability built around the machines on the line.
Trade-off: the focus is material control. If your biggest losses are stops and their reasons, ask in the demo how stop reasons are captured and where the follow-up work is recorded.
Where it fits: high-mix plants with complex, non-linear routings that want a full MES.
Critical Manufacturing is an MES built for high-tech industries. It handles routings where a board passes through SMT, manual insertion, wave soldering and coating, and OEE is part of that wider system.
Strengths:
Complex routings and process flows in one system.
OEE inside a full MES, next to orders and process data.
Trade-off: a full MES is a larger project than measuring line performance. Plan for the scope, the integration and the change it asks of the plant.
Where it fits: plants that want OEE, downtime tracking and production monitoring on their SMT and manual lines first, and intend to keep their ERP.
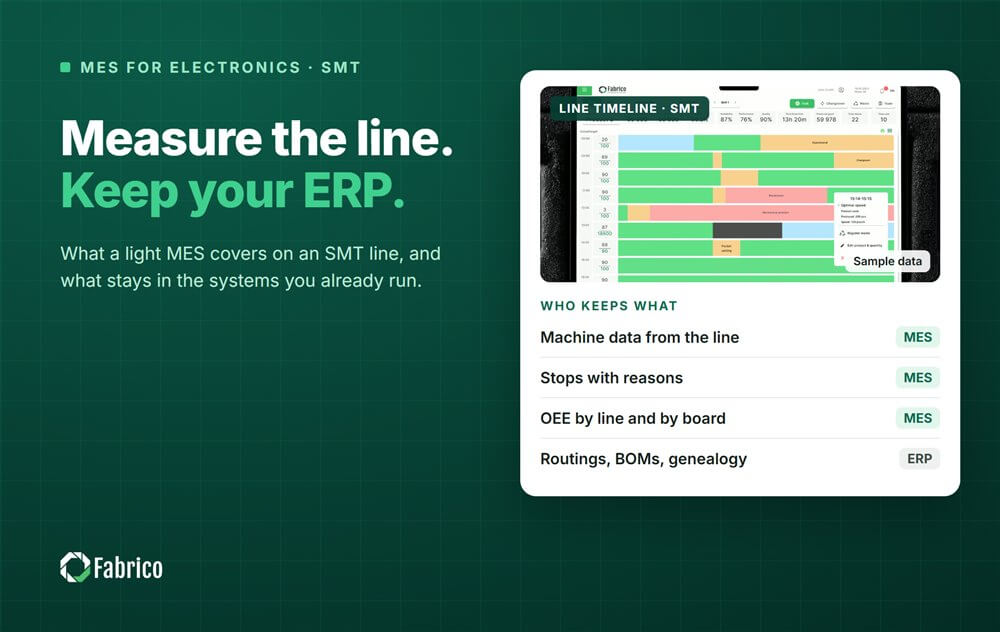
Fabrico is a light MES: machine data collection, production monitoring, OEE and downtime analytics, and integration with SAP and other ERP systems, with maintenance built in. It records stops and counts from the PLC or an IoT device, operators add the reason, and the team opens the work order from the logged stop, on the same machine record. A camera can cover manual stations such as rework benches and hand assembly.
Strengths:
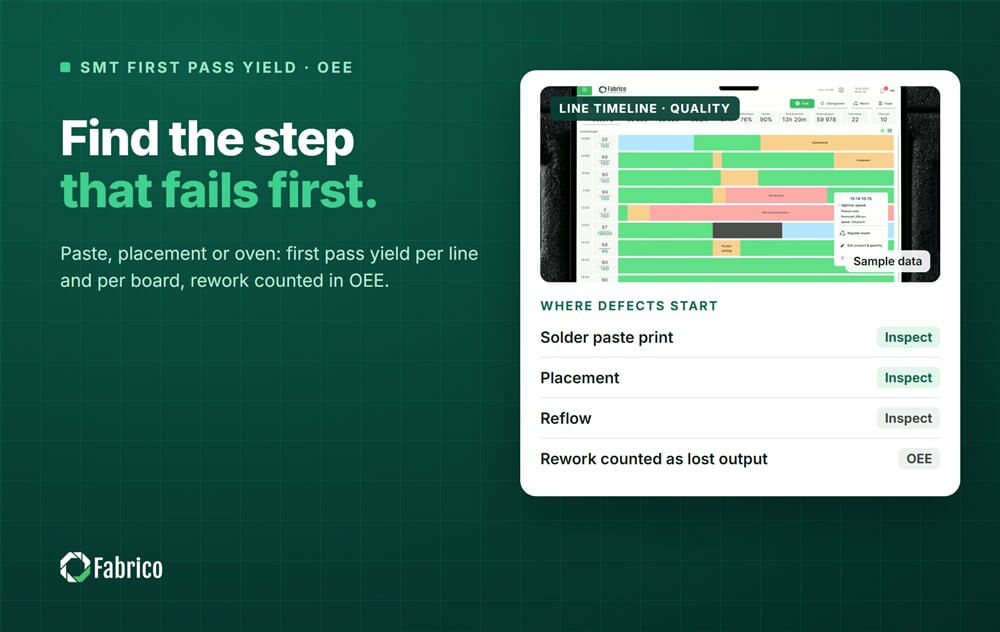
OEE and downtime by line and by board, with stop reasons the operators recognise.
Machines without a readable PLC, and manual stations, can be covered by IoT devices or cameras.
Production and maintenance on one asset registry.
Trade-off: Fabrico is not a material verification or genealogy system. Job dispatching, BOMs, routings and genealogy stay in your ERP and in the machines' own records. Installing the devices and connecting the machines takes about one month; full rollout across the lines you choose takes 3 to 4 months.
Where it fits: electronics, automotive and medical device plants where traceability comes first.
iTAC is an MES for electronics, automotive and medical device plants, built around traceability, lot tracking and process interlocking.
Strengths:
Traceability and process interlocking across the line.
An enterprise MES scope for plants with strict process requirements.
Trade-off: an enterprise-grade system is a larger rollout. Ask how long the first line takes and what it needs from your team.
Where it fits: large EMS providers running SMT machines from several vendors.
Valor, now part of Siemens, collects SMT machine data from many machine brands and presents it in one view. It also covers material verification, so the right reel is loaded in the right slot.
Strengths:
Machine data from mixed-vendor SMT lines in one place.
Material verification at setup.
Trade-off: it is a broad suite; ask which modules you need for OEE alone and what a rollout looks like at your size.
| Platform | Starting point | Material and traceability | Typical plant |
|---|---|---|---|
| Cogiscan | Material flow around the machines | Core focus | Plants where material is the bottleneck |
| Critical Manufacturing | Full MES for complex routings | Part of the MES | High-mix, complex process flows |
| Fabrico | OEE, downtime and monitoring by line | Stays in the ERP and the machines | Plants that keep their ERP and start line by line |
| iTAC | MES built around traceability | Part of the MES | Automotive, EMS and medical electronics |
| Siemens (Valor) | SMT machine data across vendors | Material verification at setup | Large EMS with mixed-vendor lines |
How is OEE calculated for a whole SMT line, against which bottleneck?
How do short stops at feeders and nozzles reach the system, and who adds the reason?
Where are reworked boards counted?
What stays in our ERP, and what does the platform take over?
For the measurement itself, our OEE guide for electronics manufacturing explains how to measure the SMT line as one constraint, and our guide to MES for electronics manufacturing explains what a light MES covers.
Request a demo to see OEE and downtime on your own SMT lines.
 Login
 Blog