
CNC machining cells look highly automated and data rich, yet many manufacturers still struggle to explain why OEE is stuck at the same level month after month. Spindles are cutting, parts are shipping, but scrap, minor stops and tool issues quietly erode performance. If you only look at spindle time from the controller, your OEE picture will always be incomplete.
This article explains how to measure OEE in CNC environments using spindle time and value-added time, how to factor in tool changes and offsets, and what a manufacturing execution system adds beyond raw controller data. It is written for people who buy MES and OEE software: plant leaders who need numbers they can trust and a way to turn those numbers into action.
OEE in assembly lines is usually tied to line rate and takt time. CNC cells behave differently. They run a mix of parts, each with its own program, cycle time, tooling and changeover pattern. A single machining center might run short prototypes in the morning and long production batches in the afternoon. Downtime is not only about breakdowns, it is about offsets, probing cycles, tool changes and NC edits.
That complexity is exactly why many manufacturers start their OEE journey in CNC machining and quickly hit a ceiling. They pull data from the controller, see when the spindle is running or stopped, and calculate availability from that. It creates a baseline, but it blurs the line between value-added cutting and everything else that happens in the cycle.
To design an OEE program that actually improves machining performance, you need a more precise view of time: spindle time, value-added time and the losses that separate the two.
Most CNC controllers expose straightforward signals: cycle start, cycle stop, spindle on or off, feed hold, alarm status. These are useful, but they are not the same thing as value-added time.
From an OEE perspective, spindle time is a good starting point for availability, but it can hide several issues:
With raw spindle signals alone, it is hard to distinguish a program that is well optimized from one that wastes several minutes per cycle. That is why many operations leaders complement controller signals with part level and loss level context from an MES.
There are two common ways manufacturers use spindle time in OEE for machining:
In this approach, availability is calculated from machine state: running (spindle on), idle or stopped. This highlights unplanned stops, delays and long changeovers. It is useful when breakdowns, setups or waiting for material dominate the loss picture.
Here, performance is based on how the actual spindle-on time per part compares to the standard for that part. This reveals cycle creep, NC edits and conservative feed overrides. It is essential in high-mix CNC cells where the machine appears busy, but throughput is below plan.
The controller alone can provide the states you need for both methods. However, it does not tell you why a performance gap appears, when it started, on which product, or how much loss is due to a changeover versus tool wear.
For that, you need an OEE and MES layer that turns raw signals into structured events, parts and reasons. The article How to approach OEE tracking explores this in more depth.
Spindle time is not always equal to value-added time. Measuring value-added time requires you to separate necessary cutting from avoidable loss inside the cycle.
Typical non value-added elements inside a CNC cycle include:
An MES with real-time OEE transforms cycle data into a model of value-added and non value-added segments by combining:
The result is more than a single spindle time metric. You gain a view of where value is created and where it is lost. This allows plant managers and process engineers to focus improvement work on specific operations, tools and programs instead of debating machine utilization in general terms.
Tooling is the heart of CNC productivity. Tool changes, presetting, breakages and offsets all influence OEE, but they often show up as small losses scattered across the shift.
Typical tooling related losses include:
If you rely only on controller states, these losses appear as generic “stop” or “feed hold” time. You see that OEE is lower than planned, but you cannot tell whether the problem is scheduling or tooling.
An MES that reads controller data and enriches it with operator input and maintenance actions lets you:
In Fabrico, for example, tooling events are not just states in a chart. They become structured losses that can create follow-up tasks in the platform for production, process engineering and maintenance teams. This is where an OEE platform with a built-in maintenance management layer is especially useful.
CNC controllers are very good at telling you what is happening at the machine right now. An MES like Fabrico builds on that foundation and answers a different set of questions:
Fabrico connects directly to CNC controllers and PLCs, then adds:
For operations teams that want to scale OEE across multiple cells and plants, this approach also solves a data management problem. Instead of building plant-specific spreadsheets, you use a common data model for machines, operations, losses and actions. The article How OEE software benefits from unified data and intelligence explains why this matters when you move beyond a pilot.
Capturing CNC data is useful only if it drives decisions and actions. Fabrico is designed to turn every recorded loss into something a team can act on, either on the shop floor today or through structured improvement work.
Typical use cases in CNC environments include:
The built-in maintenance capabilities keep technicians, supervisors and CI leaders in the same platform. This reduces the gap between discovering a loss, assigning responsibility and verifying that the fix worked.
For plant and operations leaders planning or evaluating an MES and OEE project in CNC machining, a phased approach often works best.
Connect your CNC controllers to the platform, validate that states like running, idle, alarm and program end are mapped correctly, and confirm that spindle time and cycle counts are accurate. This is your OEE foundation.
Create a clean list of products, operations and standard cycle times. Even if standards are approximate at first, they are essential for spotting performance gaps and value-added versus non value-added segments.
Introduce a simple reason tree for stops and speed losses: setups, tooling, material, quality and maintenance. As you gain insights, refine the reasons to capture the patterns you care about, such as offset adjustments or tool presetting.
Use Fabrico to turn frequent or high impact losses into tasks for production, engineering or maintenance. This is where the platform moves beyond dashboards to real change on the floor.
Once the model works in one machining cell, apply the same structure to other machines and sites. The article How to choose OEE software for manufacturing offers criteria to evaluate platforms for multi-site rollouts.
Fabrico is a cloud-based MES and OEE platform designed for manufacturers who need more than basic machine monitoring. It connects directly to CNC controllers, captures production and downtime data from the machines and transforms it into real-time OEE and loss visibility.
Key capabilities for CNC environments include:
For plant managers, operations directors, production managers and maintenance heads, this combination of OEE, production context and maintenance in a single platform reduces the effort required to maintain an accurate view of CNC performance across the factory.
If you are planning to improve OEE in CNC machining cells, consider how far you can get with controller signals alone and where you need the richer context of an MES. The right platform will help you move from spindle time to value-added time, from generic downtime to actionable loss categories and from reports to concrete actions that protect output.
Request a demo to see how Fabrico collects CNC data, visualizes OEE in real time and connects it with actions for production and maintenance teams.
If you would like to discuss your CNC environment, data sources and OEE objectives in more detail, Contact us.
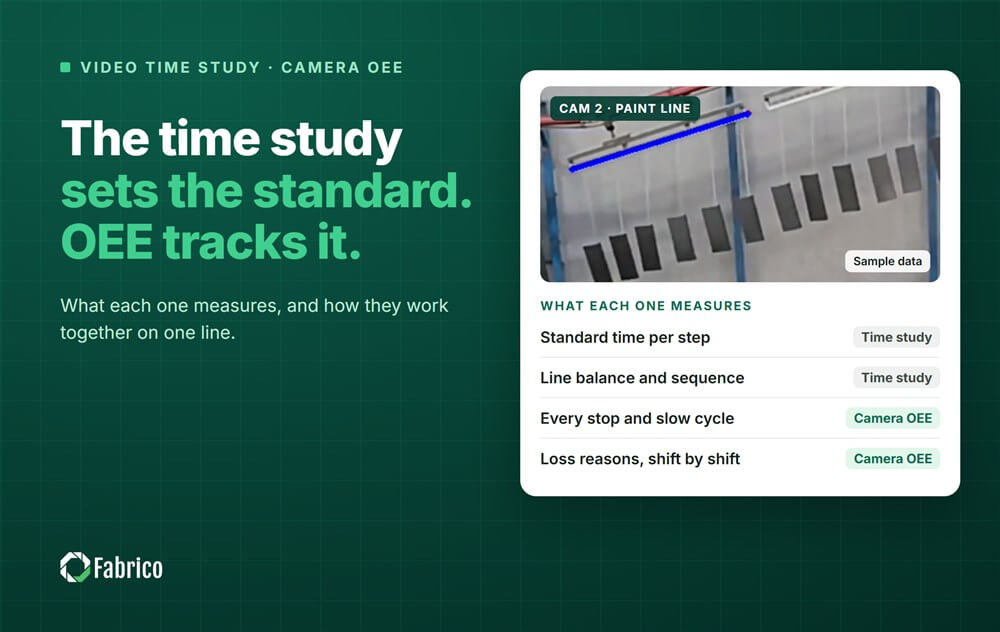
On a CNC cell, spindle data shows that the machine stopped, not why. A camera over the cell shows the operator waiting for a program, a fixture or a first-off check, and Fabrico's camera-based OEE software puts that clip next to the spindle signal in the same OEE timeline.
See how Fabrico unifies OEE and maintenance in one platform.
Request a demo






 Login
 Blog