


 Login
 Blog
Cannery Software: What a Canned Food Plant Needs First

In short: cannery software is a stack of separate products. A canned food plant runs retort control and recording for the thermal process, scheduled process files from its process authority, seam inspection records in QA, an ERP for lots and pack contracts, a warehouse system for bright stock, and an OEE or light MES layer for the filling, seaming and labelling lines. Buy the floor layer first when the question is lost hours, not missing records.
- Retort records and scheduled processes are regulated records for low-acid canned foods in the US. They stay in the retort control system and the process authority's files.
- OEE and light MES answer a different question: why the seamer, the steriliser infeed or the labeller stood still.
- Pack season changes everything. Lines run around the clock for weeks, and raw supply gaps can cost more than any machine fault.
- Bright stock is labelled weeks later, so the labeller needs a separate OEE from the filling line.
A cannery runs on a promise made in a lab. The process authority sets a time and temperature for each product and can size, and the retort room has to deliver it, batch after batch. Everything around that promise, from the filler to the pallet, is ordinary line work that loses ordinary hours.
Vegetable, tomato, bean, soup, fish and pet food canneries comparing cannery software or canning software all face the same first question: which piece to buy first.
Fabrico builds the OEE and light MES layer. It is not a retort control system and not a process authority tool, and this page keeps that line clear.
The cannery software stack: which system owns which record
A canned food plant buys software for two very different reasons. Some systems exist because the thermal process must be controlled and proven. Others exist because the plant must make more cans per hour. Mixing the two up is an expensive buying mistake.
| System | What it does in a cannery | Owner | Fabrico? |
|---|---|---|---|
| Retort control and recording | Runs each batch retort or continuous steriliser to time, temperature and pressure, and records it | Thermal process lead, QA | No |
| Process authority files | Scheduled processes for each product and can size, deviation reviews | Process authority, QA | No |
| Seam inspection records | Double seam teardowns and visual checks per seamer head | QA lab | No |
| ERP | Lots, grower and pack contracts, can and lid stock, costing | Finance, supply chain | No |
| Warehouse system (WMS) | Bright stock in store, holds, release, picking | Logistics, QA | No |
| Quality system (QMS) | HACCP plans, holds, audits, complaints | QA, food safety | No |
| OEE and light MES | Stops, counts and losses at depal, filler, seamer, retort infeed and labeller | Operations, CI | Yes, this is Fabrico |
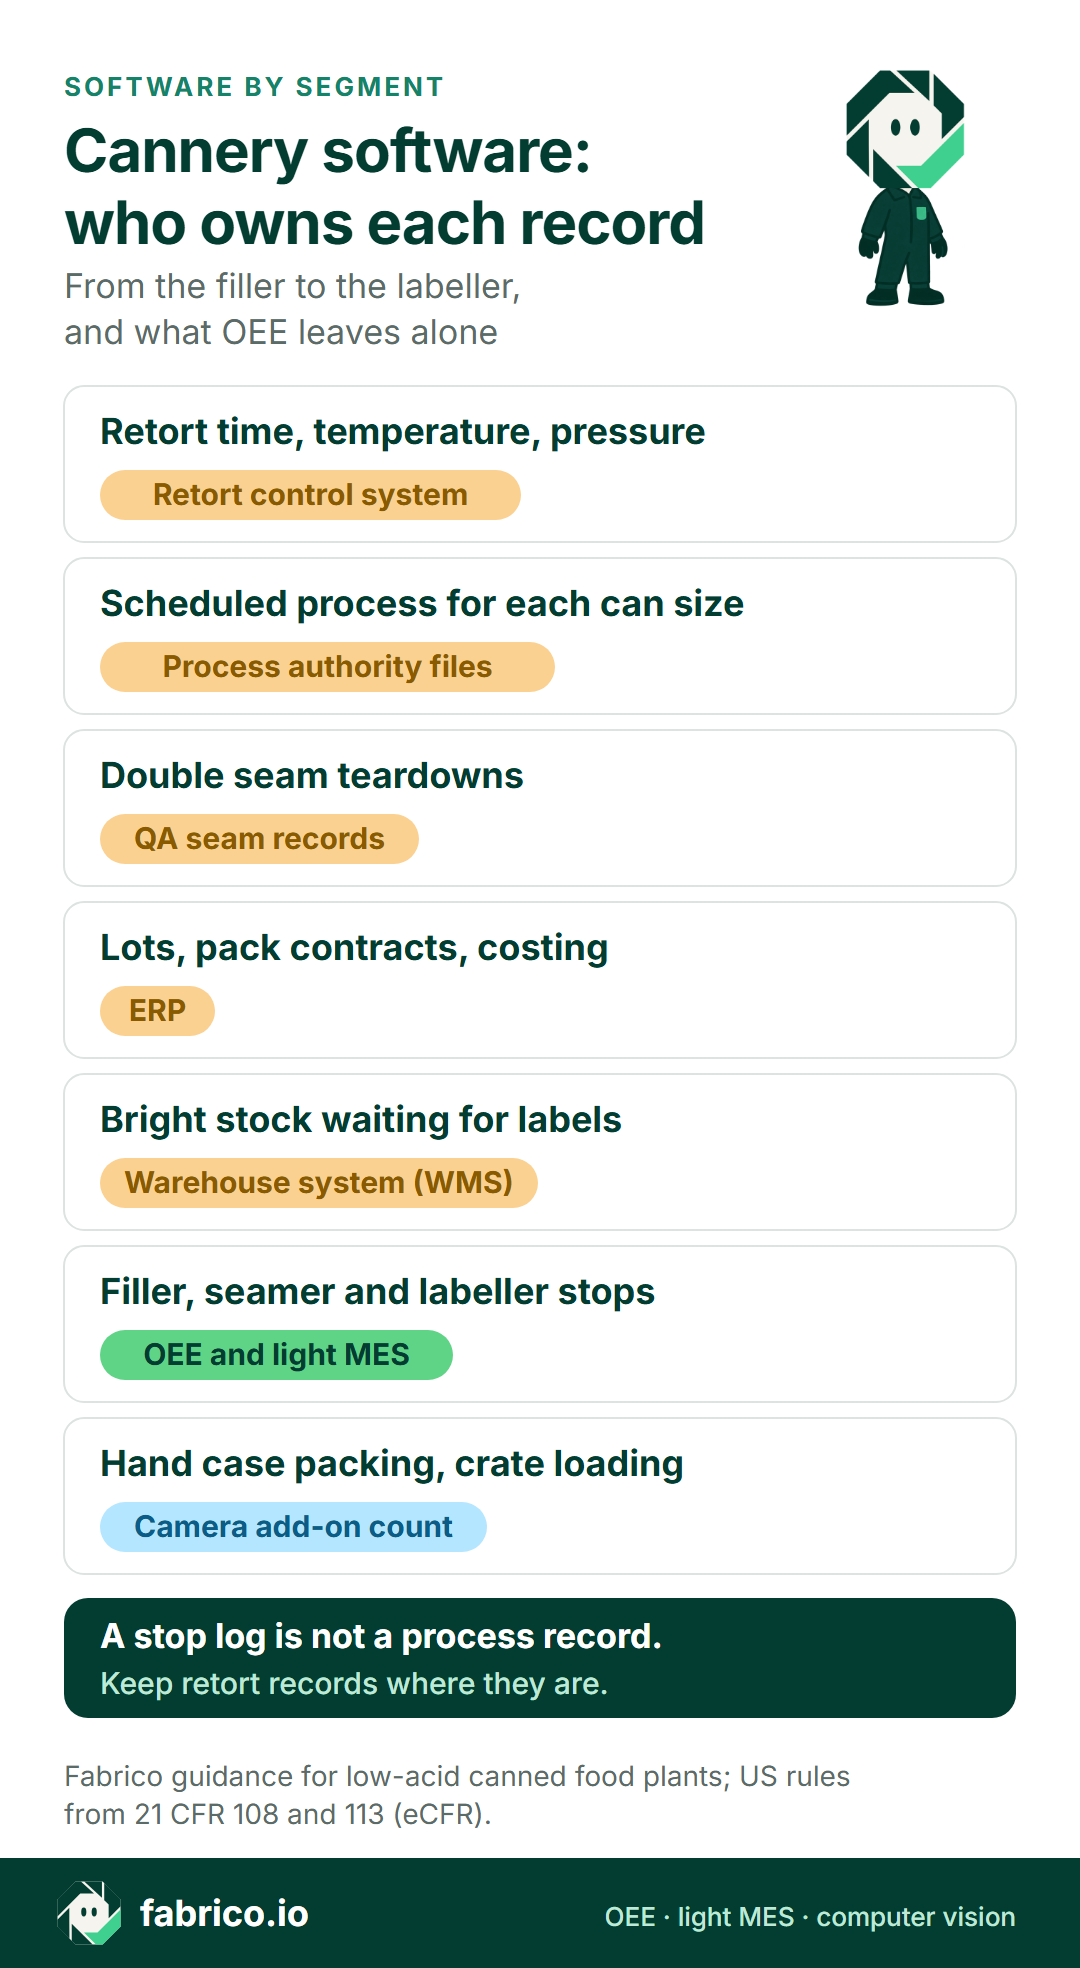
Text version of this infographic
- Cannery software card: retort time, temperature and pressure belong to the retort control system, scheduled processes to process authority files, double seam teardowns to QA, lots to the ERP, bright stock to a WMS, and filler, seamer and labeller stops to OEE and light MES.
Retort control and recording
This is the system the plant cannot run without. On batch retorts it drives the come-up, hold and cooling of each load and records the result. On a continuous rotary steriliser it holds reel speed and temperatures across the shells. It is bought with the retort equipment or from a thermal process specialist, and it is validated for that job. Treat it as a separate product category from anything on this page's floor layer.
Process authority files and seam QA
The process authority's studies and the scheduled process for each product and can size usually sit with the authority and QA, along with deviation reviews. Double seam teardowns sit in the QA lab, often in seam scope software. Both are records an inspector may ask for, so their owner is QA, not operations.
ERP and warehouse: pack contracts and bright stock
The ERP holds grower and pack contracts, can and lid stock, lots and costing. The warehouse system holds bright stock: filled, sterilised cans stored unlabelled until an order says which label goes on. Holds and release after a deviation also need a home here, so ask how the ERP and WMS mark a held lot.
If you make your own cans, the can-making line needs its own asset in any line software, so empty can shortages do not hide inside the filling line.
OEE and light MES: lost cans by station
This layer reads the depalletiser, filler, seamer and labeller signals, and asks the operator why the line stood. Each number on a canning line comes from a different system, as the map below shows.
Which links between systems matter
The ERP sends products, can sizes and orders to the OEE layer, which sends back run hours, stop minutes and good cans. The retort control system keeps its own records. At most, its run state can tell the OEE layer that the retort area blocked the seamer. Ask each vendor who builds each link, and make sure no link copies a process record into a system that was never validated for it.
What the US rules ask of a low-acid cannery, and where those records live
The US rules for low-acid canned foods are written out clearly, so they show exactly which records a cannery must keep. Plants outside the US work under their own national and EU rules, so ask your process authority which ones apply.
- Registration. Under 21 CFR 108.35(c)(1), a commercial processor of thermally processed low-acid foods in hermetically sealed containers must register with the FDA on Form FDA 2541 not later than 10 days after first so engaging.
- Process filing. Under 108.35(c)(2), the processor must, not later than 60 days after registration and prior to the packing of a new product, give the FDA its scheduled processes, including the type of retort or other thermal processing equipment, for each low-acid food in each container size.
- Who sets the process. 21 CFR 113.83 says scheduled processes for low-acid foods shall be established by qualified persons.
- At the retort. 21 CFR 113.87 says operating processes and retort venting procedures for each product and container size shall either be posted in a conspicuous place near the processing equipment or be made readily available to the retort or processing system operator.
Note what 21 CFR 113.3 means by a scheduled process: the process selected by the processor as adequate under the conditions of manufacture. That is a thermal process decision. OEE software has no part in it.
So a stop log is not a process record. If a vendor of line software offers to hold your retort records, ask who validated that system and who your process authority is. Seam check intervals and process records under 113.60 and 113.100 are covered in computer vision for canned food lines.
One line in 108.35 shows how seasonal canning is. A registered processor must notify the FDA after it stops packing, but that notice is not required for a temporary cessation necessitated by the seasonal character of the plant's production.
Line losses on a canning line, briefly
On a can-filling line the losses gather in a few places. The depalletiser runs out of empty cans or lids. The filler waits for product from the blancher or cooker, and in pack season raw supply gaps often stop the line longer than any fault. The seamer stops for lid feed and transfer jams, then for the seam checks that follow. On batch retort lines, crates wait for a free retort and the seamer is blocked. On a continuous rotary steriliser, a temperature drop can hold the whole line. Off season, can size and recipe changes take over. The station rules are in OEE for food canning lines, and the seamer in can seamer OEE.
Which cannery software to buy first
Pick the row that hurts most this season. Rows three to five are compliance and QA buys, and they go first if an audit finding is open. Rows one and two are where most canneries lose cans without a record.
| What went wrong | Start with | Why |
|---|---|---|
| Nobody can say where last night's hours went | OEE and light MES on one line | Stops and counts come from the seamer and filler signals |
| The seamer stops when the retorts are full | OEE with a 'blocked by retort' code | It moves the loss to the retort area where it belongs |
| Retort charts are on paper | A retort control and recording system | A regulated process record needs a validated system |
| A new product needs a process | Your process authority | Under 113.83, qualified persons set scheduled processes |
| Seam teardown results live in a binder | Seam inspection software in the QA lab | Seam records belong to QA |
| Bright stock is hard to find and release | A WMS | Holds, locations and release are its job |
| Lots and grower contracts in spreadsheets | An ERP | Lots and costing need one home |
Two timing rules help. Buy before pack season, not in it, because nobody has time to learn a system while tomatoes arrive by the truckload. And start the floor layer on the line where the seamer paces, then add the labeller.
Bring a seamer stop sheet and one retort log to a demo, and we will show what Fabrico fills and what stays in your process systems.
What the OEE layer shows in pack season
The light MES sets the ideal rate at the machine that paces the line, in cans a minute per can size: usually the seamer, or the reel on a continuous rotary steriliser. The operator tags the reason at the line: no product, lid jam, check after jam, blocked by retort. The camera add-on fits crate unloading after batch retorts or hand case packing, where no machine count exists; the FMCG camera guide covers how those counts work.
Worked example: one held lot after a steriliser deviation
An invented case, from no real plant. A temperature drop on the continuous steriliser puts one lot of diced tomato on hold. QA must show the process record for that lot, the deviation review, which pallets of bright stock are held and when the line stopped, and each answer sits in a different system.
| System | What it holds for this lot | Where the hand-off can break |
|---|---|---|
| Retort control and recording | Temperatures and reel speed for the affected cans | Clock not matched to the lot code times |
| Process authority files | Scheduled process, deviation review, release decision | Review on paper, filed away from the lot |
| ERP | Lot code, can and lid lots, the pack contract | Lot split across two shifts by hand |
| WMS | Bright stock pallets of the lot, hold and release | Pallets moved before the hold was set |
| OEE and light MES | Stops, the hold's start and end, can counts | Holds no process or lot record, only run data |
The trace breaks where the steriliser record, the lot code and the pallets use different clocks. Fabrico plays no part in the trace; it supplies only when the line stopped and how many cans it counted. The OEE maths for a canning line shift is in OEE for food canning lines.
Eight questions to put to a cannery software vendor before pack season
Ask them of every vendor on the shortlist, with last season's seamer stop sheets and retort logs on the table.
| Ask | How to test the answer |
|---|---|
| Can it hold an ideal rate per can size, set at the seamer or the steriliser reel? | Ask for two can sizes on one line with two rates, and see where each rate is set. |
| How does it model a batch retort room next to a continuous line? | Ask to see the retorts as a separate asset, and a 'blocked by retort' code that charges the seamer's lost time to them. |
| What does it claim to record about the thermal process? | The right answer for an OEE tool is line stops only. Retort records stay in the validated retort control system. |
| How is a seam check after a jam coded? | Ask for the jam and the check as separate reasons, so QA time is not hidden inside the fault. |
| Which ERP fields does the line read? | Products, can sizes and orders in; good cans out. Ask who keeps the link. |
| How does labelling of bright stock get a separate OEE? | Ask to set up the labeller with its own shifts and count, weeks after the cans were filled. |
| Who owns the link to the retort control system? | Ask whether the line layer reads only the retort's run state, and who maintains that link. |
| How does a held lot show up after a deviation? | Ask which system marks the hold, the ERP, the WMS or the QMS, and what the OEE layer shows: the stop time only. |
Fabrico in a cannery: the line side, and nothing in the retort records
Fabrico is a cloud OEE and light MES platform. For a canned food buyer, three things set it apart from a retort or QA system:
- Retort area losses in cans: seamer stops caused by full retorts or a steriliser hold get separate reason codes, so the retort room's effect on the line shows in cans and money, while the thermal process records stay where they are.
- Pack season reasons: seasonal crews tag stops at the line on a tablet or phone, from a short list that splits raw supply gaps from machine faults.
- Bright stock and hand stations: the labeller is set up as a separate line with its own shifts, and the camera add-on counts crates or hand-packed cases where no machine count exists. Its video is streamed on request, not stored in Fabrico.
Generic platform facts, from loss pricing to apps and exports, sit on the MES and OEE software page and the computer vision add-on page.
What Fabrico does not do: retort control or recording, scheduled processes or deviation reviews, double seam inspection, fill weight control, label or code inspection, lot genealogy and batch records. Those stay in your retort system, with your process authority, in the QA lab and in the ERP. The pack season run plan stays with your planners and the ERP.
What cannery teams ask next
What is cannery software, in one line?
It is the set of systems a canned food plant runs: retort control, process files, QA records, ERP, warehouse and OEE. Each one owns a different record.
Does OEE software replace retort records?
No. Retort records belong in the validated retort control and recording system. OEE software times the line stops around the retort and shows what they cost.
Can one vendor cover retort records and line OEE?
Ask for both parts separately. The retort records must sit in a system validated for the thermal process, with your process authority's agreement. The line layer only needs the retort's run state, to book a seamer stop as blocked by retort.
Should raw supply gaps count against the line?
Yes, as stop time inside planned production, but in a separate reason group. Then the receiving and peeling side can see its share of lost cans.
Which system marks a held lot after a deviation?
The QMS, ERP or WMS, whichever your QA team names as the owner. The line layer shows only the stop time the hold caused.
Does Fabrico check double seams?
No. Double seam teardowns and visual seam checks belong to the QA lab and its records. Fabrico can time the line stop while a check runs.
Want to see a pack-season shift in cans and money? Book a demo with one shift's retort log and the seamer stop sheet that goes with it.
Related articles








Real Fabrico tiles, sample data.