

The tray sealer on the fresh meat line cycles with three trays in a four-tray tool. One tray is missing because the denester dropped two stuck together and the operator pulled them out. The sealer never stopped, so the OEE report shows nothing wrong, yet a quarter of that cycle was lost.
Tray sealers close pre-formed trays with a lidding film, usually after flushing a modified atmosphere (MAP) into the tray. This guide covers the stations and their stops, how to measure each OEE factor in trays rather than cycles, tool changes, seal and gas rejects, and how to classify washdown time so the numbers stay honest.
A typical MAP tray line runs from the tray denester to filling (by hand, by depositor or from a weigher), the sealer infeed that places trays in the tool, the sealing station with gas flush and lidding film, film skeleton rewind, the outfeed, the checkweigher and the labeller.
| Station | Typical stops and losses | OEE factor |
|---|---|---|
| Tray denester | Trays stuck together, double trays, tray not dropped, magazine empty | Short stop, Performance |
| Filling | Tray not filled, product on the flange | Performance, Quality |
| Infeed to the tool | Tray misplaced or tipped, gripper fault | Short stop |
| Sealing tool | Seal temperature, tool fault, film not cut | Availability, Quality |
| Gas flush | Gas supply low, gas mix out of range | Availability, Quality |
| Lidding film | Reel end, film break, skeleton rewind full or torn | Availability or short stop |
| Tool change | New tray size or format | Availability |
| Washdown | Cleaning between products or at the end of the day | Planned or Availability, by type |
A tray sealer works in cycles, and each cycle seals as many trays as the tool has cavities. The rated speed is cycles a minute times trays per cycle, set per tool and tray: a deeper tray or a different film may need a longer cycle. Count output in trays, not cycles.
Then an empty cavity becomes visible. If the infeed delivers three trays to a four-tray tool, the cycle runs and the PLC shows no stop, but a quarter of that cycle is lost. That loss sits in Performance. Count cycles instead of trays and it disappears.
The denester is the first source of short stops. Trays that nest too tightly, warped trays, static and a magazine that runs empty all lead to missed or double trays. A double tray that reaches the tool can jam it or seal badly, so many lines have an operator pull doubles out by hand, which then shows up as empty cavities.
Filling causes the other tray handling losses. Product on the flange is the most common one, because it sits exactly where the seal has to go. On hand-loaded lines the loading area often sets the sealer's real speed. That is a line balance question, measured in trays a minute at the sealer, and a process to improve, never a reason to judge the people loading.
A MAP tray is good only if the seal holds and the gas inside is right. The main rejects are leaking seals, wrinkled or incomplete seals, product or juice trapped in the seal, film not cut cleanly and trays with gas readings out of range.
Many plants check seal integrity and gas mix by sampling, with leak tests and a gas analyser on trays taken off the line. If the test destroys the tray, count it in Quality, and count a batch held and reworked after a failed test as a Quality loss too. When rejects rise after a restart, a tool change or with one product, look at seal temperature, tool alignment and product on the flange first. More in our guide to the OEE Quality factor.
A tool change for a new tray size is usually the tray sealer's longest changeover. The tool comes out, the new one goes in, and film width, heating, gas settings and the infeed have to match the new tray. On many machines the tool is heavy and moved on a trolley.
Measure from the last good tray of the old format to the first good tray of the new one at rated speed. Then apply SMED: preheat the next tool where the machine allows it, stage the film reel and the trolley before the stop, and record settings per tool. Set a standard per tool change and track each minute over it.
Washdown is where tray sealer OEE gets argued about most. Decide the rule by type, write it down and apply it before the first shift, so nobody reclassifies after the fact.
| Type of clean | When it happens | How to treat it in OEE |
|---|---|---|
| End of day sanitation | Scheduled after production ends | Outside planned production time |
| Scheduled clean between products | Planned inside the production window | Planned at its standard; minutes over it are an Availability loss |
| Allergen changeover clean | Between allergen classes, validated | Planned at its validated standard, never shortened to win OEE |
| Unplanned clean | After a burst pack, a spill or contamination | Unplanned Availability loss with a reason code |
| Quick flange or tool wipe | During the run, a minute or two | Short stop |
The rule that keeps it honest: inside the planned production window, a stopped machine is unplanned downtime unless the stop is a registered planned type. Our guide to planned and unplanned downtime definitions covers the rule, and allergen changeover validation explains why the validated clean is not up for negotiation.
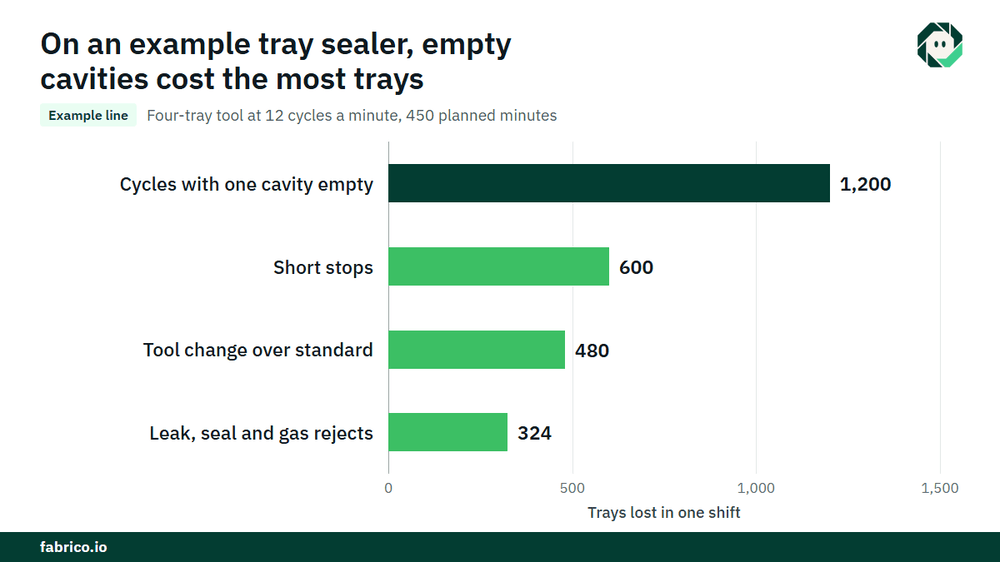
Sample line (illustrative numbers, not a customer): a tray sealer with a four-tray tool at 12 cycles a minute, rated at 12 x 4 = 48 trays a minute. The shift has 480 minutes; a 30 minute scheduled clean between products runs at its standard, so planned production time is 450 minutes.
The tool change overran its standard by 10 minutes: 10 x 48 = 480 trays, or $192 at $0.40 a tray (€192 at €0.40). The empty cavities never stopped the machine and cost more than twice as much.
The sealer PLC knows its cycles, temperatures, gas and film faults. It does not see a double tray pulled out by hand, a tray tipped at the infeed or product on a flange. Where a camera watches the denester or the tool infeed, the clip shows what happened before the stop, and the operator confirms the reason in one tap. The camera does not judge the seal: seal integrity stays with the leak test and the gas analyser.
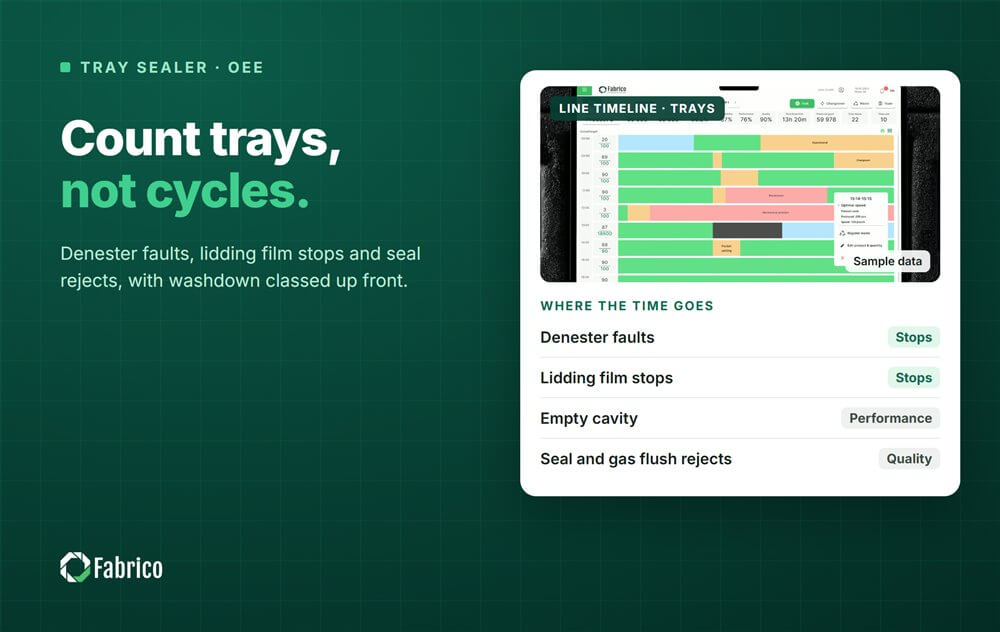
Fabrico is a computer vision enabled Manufacturing Performance Platform. OEE and light MES come first: automatic downtime logging at the sealer and the denester, OEE live by line and shift, and washdown recorded by the type the plant defined.
You start on one line, with a baseline and a decision date agreed in advance. There is no free plan and there are no tiers: each plant gets a quote. See how stops are logged and coded on our downtime tracking page.
Count in trays. Availability is run time over planned production time, Performance is trays sealed over cycles a minute times trays per cycle times run time, and Quality is good trays over trays sealed.
It depends on the type. End of day sanitation sits outside planned time, a scheduled clean counts as planned at its standard, and an unplanned clean after a spill is an Availability loss. Write the rule down before the first shift.
Product or juice on the flange, seal temperature, tool alignment or wear, and film quality are the usual causes. Check whether leaks follow restarts, tool changes or one product.
Yes. A cycle that seals three trays in a four-tray tool lost a quarter of its output, and that loss belongs in Performance.
There is no general figure; it depends on the machine and the tool. Measure your own changes to the first good tray at rated speed and set a standard per tool.
Bring one line and its current downtime log. We will show its stops, empty cavities and washdown time, priced in money.
 Login
 Blog