


 Login
 Blog
OEE Units: Should You Count Bottles, Cases or Pallets?

Key takeaways
- The unit does not change OEE. Mixing units does.
- Count each machine in its natural unit: bottles at the filler, cases at the packer, layers at the palletiser.
- Line OEE: good output at the line end, in filler bottles.
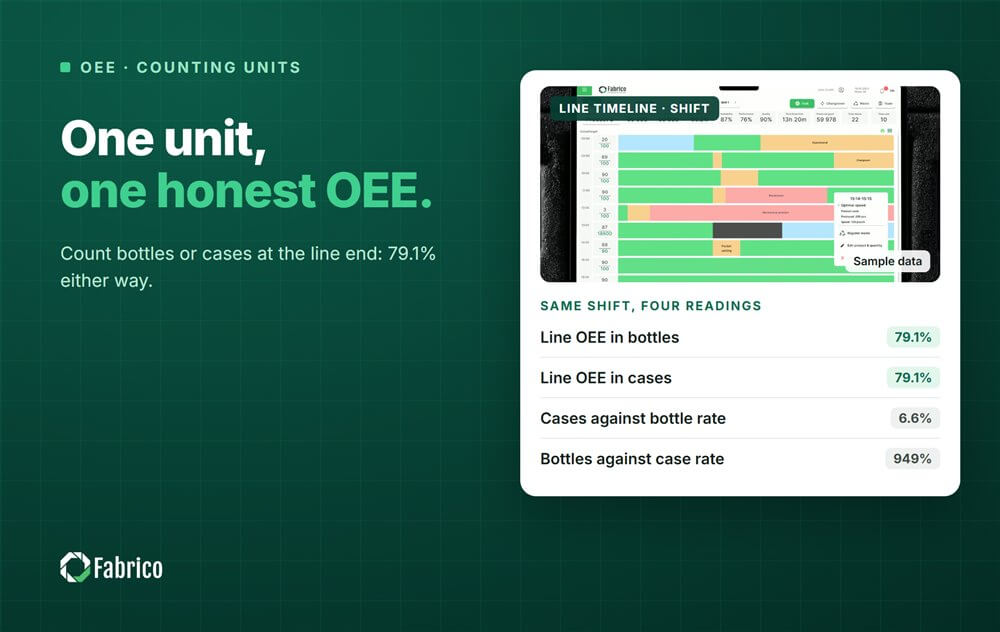
- In the worked example, a unit mix-up shows 6.6% or 949% for a line that really ran at 79.1%.
Fabrico, OEE and light MES (manufacturing execution system) software with AI cameras, logs stops automatically and shows OEE per machine and per line.
Below: the natural unit of each machine, how to convert, a worked shift in two units, and the mix-ups that break the number.
Does the unit change the OEE?
No, if you are consistent. OEE = good count x ideal cycle time / planned production time. If you count cases, the ideal cycle time must be the time for one case. If you count bottles, it must be the time for one bottle.
It goes wrong when the count and the rate come from different units. Our OEE calculation guide shows the base formula.
What is the natural unit of each machine?
| Machine | Natural unit | Convert to bottles |
|---|---|---|
| Filler, capper, labeller | Bottle | x 1 |
| Shrink wrapper | Pack | x bottles per pack |
| Case packer | Case | x bottles per case |
| Palletiser | Layer | x cases per layer x bottles per case |
Keep the natural unit for each machine's own OEE. That is how its crew thinks and how its counter works. Use the converted unit only when you add machines together.
What does a worked example in bottles and in cases show?
Sample line (illustrative numbers, not a customer): a filler rated at 300 bottles a minute feeds a case packer that packs 12 bottles a case. The line rate is 25 cases a minute, and planned time is 450 minutes.
- Possible output = 450 x 300 = 135,000 bottles, or 450 x 25 = 11,250 cases.
- The filler makes 108,000 good bottles: filler OEE = 108,000 / 135,000 = 80.0%.
- The line ships 8,900 good cases: 8,900 / 11,250 = 79.1% line OEE.
- In bottles: 8,900 x 12 = 106,800, and 106,800 / 135,000 = 79.1%. Same answer.
The 1,200 bottles between the filler and the cases are in the buffer, damaged on the conveyor, or rejected at the packer. Track that gap on its own. Our OEE quality guide covers how rejects lower Quality.
The packer's own OEE uses its own rated speed, not the line rate. Packers are usually built faster than the filler, so they can catch up after a stop.
What happens when you mix units? A worked example
Same Sample line:
- Cases counted against the bottle rate: 8,900 / 135,000 = 6.6%. The line looks broken.
- Bottles counted against the case rate: 106,800 / 11,250 = 949%. The line looks impossible.
- A 24-pack run against the 12-pack case rate: the packer seems to run at half speed when it works normally. A 6-pack would seem to run at double speed.
Extreme numbers get caught. The dangerous mix-up is the subtle one: a case rate that is right for one format and used for all of them. It looks believable and is wrong every time the format changes. Our ideal cycle time guide explains rates per product.
Which unit should the line OEE use?
The unit of the bottleneck. On most food and drink packaging lines, the filler sets the pace. The machines around it are built faster so they can recover after a stop.
- Find the bottleneck of the line, usually the filler.
- Count good output at the end of the line, because only product that reaches the end can ship.
- Convert it to the bottleneck's unit with the pack count of the running product.
- Divide by planned time x the bottleneck's rated speed.
Our guide to finding the real constraint on linked packaging lines covers step 1.
What about lines that run different bottle sizes?
A 330 ml bottle and a 1 litre bottle are not the same unit of work. Keep counting bottles, but give each product its own rated speed and add the ideal time per product. Litres help in finance reports, but they hide that small sizes run at a different speed.
What mistakes do plants make with OEE units?
- A count in cases against a rated speed in bottles.
- One pack count for every format.
- Counting at the filler and calling it line output.
- Changing the unit halfway through a year, so the trend breaks.
Where Fabrico fits
Fabrico is a computer vision enabled Manufacturing Performance Platform. OEE and light MES come first. Automatic downtime logging per machine and OEE live by line and shift show every machine on one screen.
- OEE live by line and shift, per machine and for the whole line.
- Automatic downtime logging, so each stop sits on the machine that caused it.
- Losses ranked by money, so stops on the filler and the packer compete fairly.
Where a stop is in doubt, a camera clip is evidence for what happened, and the operator confirms the reason. You start on one line, with a baseline and a decision date agreed in advance. There is no free plan and there are no tiers: each plant gets a quote.
Frequently asked questions
Does OEE depend on the unit you count?
No, as long as the count and the rated speed use the same unit. Bottles against a bottle rate and cases against a case rate give the same OEE. The problems start when the count comes in one unit and the rate in another, which can happen quietly after a format change.
Should a packaging line count bottles or cases?
Each machine in its own unit for its own OEE: bottles at the filler, cases at the packer. For line OEE, convert good output at the end of the line into the bottleneck's unit, which is usually the filler's bottles. Then every machine is compared on the same scale.
Why is my OEE far above 100% or close to zero?
A unit mix-up is a common cause, for example cases counted against a bottle rate. Check that the count and the rated speed come from the same unit. Also check the rated speed itself, because an ideal speed set too slow is another frequent reason for numbers over 100%.
Can I use litres or kilograms for OEE?
For finance reports, yes, because they add up across sizes. For the line itself, count units and give each product its own rated speed. Small sizes rarely run at the same speed as large ones, and litres would hide that difference completely.
Where should good output be counted?
At the end of the line, where product is ready to ship. Counting at the filler misses losses at the packer, the palletiser and on the conveyors in between. Keep the filler count as well, because the gap between the two counts is a loss worth tracking.
See your line in one unit in a demo
Bring one line and its product list with pack counts. We will show each machine's OEE and the line figure in the same unit.
Latest from our blog


Real Fabrico tiles, sample data.