


 Login
 Blog
Rice Mill Software: Billing and Stock vs Mill Floor Monitoring

In short: rice mill software is not one product. A mill buys billing and stock software for paddy purchase, invoices and godown stock, a weighbridge system at the gate, QA records for moisture, head rice and brokens, the colour sorter's own controls, and an OEE or light MES layer that shows when the husker, whitener, polisher and bagging line were running or stopped. Buy the one that fixes the problem costing you most this season.
- If rice mill management software means billing, paddy procurement and stock to you, that is an ERP category, not production monitoring.
- Head rice yield and broken percentage live in QA and process records, not in a stop log.
- Machine running and stop time, and the OEE of the packing line from 1 kg pouches to 50 kg bags, are the floor layer. That is where Fabrico sits.
- Parboiling and drying set the pace in harvest months, so buy before the paddy arrives, not during it.
A rice mill earns its margin twice. Once when paddy is bought at the right moisture and price, and once when that paddy leaves the mill as whole, white, sorted kernels in the right bag. Software is sold for both moments, and the two kinds rarely talk to each other.
If you searched for rice mill software to print bills, track paddy from farmers and agents, and see godown stock, you are shopping for a billing and stock system. If you want to know why the whitener stood idle for two hours on the night shift, or why the 25 kg bagger packs fewer bags than its nameplate says, you need production monitoring. This page maps both, works one milling shift through to money, and ends with a plan for this week and this quarter.
Fabrico makes the second kind: OEE and light MES for the mill floor and the packing hall.
Rice mill software, system by system
Each system below holds a record that someone in the mill must answer for: the accountant for the farmer's payment, QA for the broken count in an export lot, the shift in charge for lost hours. Keep that owner in mind when a vendor promises to cover several rows.
| System | What it does in a rice mill | Owner |
|---|---|---|
| Billing, procurement and stock | Paddy purchase from farmers or agents, moisture deductions, invoices and tax, stock of paddy, rice, bran and husk | Accounts, purchase |
| Weighbridge software | Gross and tare per truck at the gate, the slip that billing uses | Stores, gate |
| QA lab records | Intake moisture, head rice and broken percentage per sample, chalky and discoloured grains | QA |
| Machine and dryer controls | PLC or HMI on the parboiling boiler, dryers, huskers and whiteners | Process, maintenance |
| Colour sorter software | Ejector settings, reject rates and cleaning cycles inside the optical sorter | Sorter vendor, QA |
| Stock module or WMS | Finished bags by grade, brand and lot, godown location, dispatch | Stores, logistics |
| OEE and light MES | Run and stop time at the husker, whitener, polisher, sorter and packers; bagging line OEE | Operations, CI |
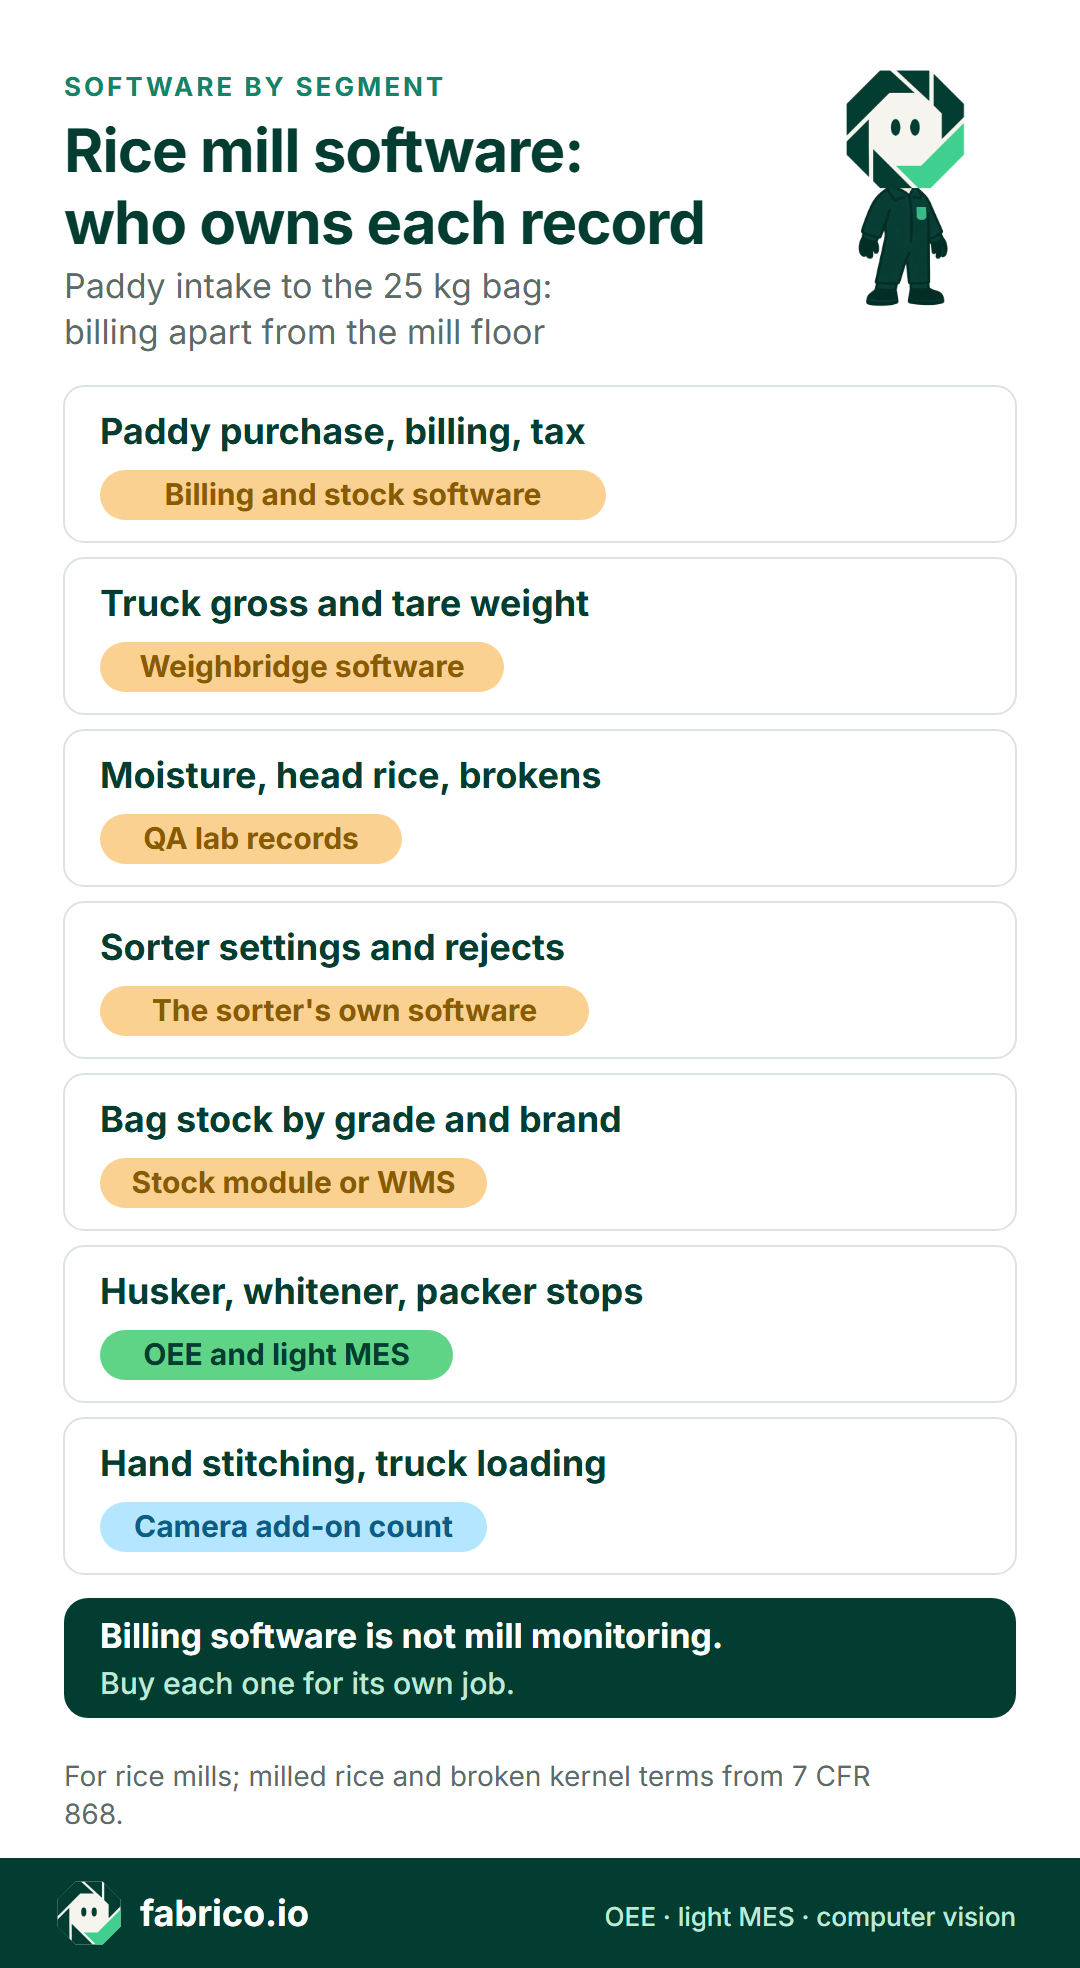
Text version of this infographic
- Paddy purchase, billing and tax: billing and stock software.
- Truck gross and tare weight: weighbridge software.
- Moisture, head rice and brokens: QA lab records.
- Sorter settings and rejects: the sorter's own software.
- Bag stock by grade and brand: stock module or WMS.
- Husker, whitener and packer stops: OEE and light MES.
- Hand stitching and truck loading: camera add-on count.
- Footer: billing software is not mill monitoring. Buy each one for its own job.
Billing, procurement and stock: what most rice mill software lists mean
This is the system a small mill buys first, and for good reason. It turns a weighbridge slip and a moisture reading into a purchase bill, keeps farmer and agent accounts, raises sales invoices with GST or VAT, and tracks how many quintals of paddy, how many bags of rice and how much bran and husk sit in the godown. Some packages add hulling-on-charge for custom milling. Judge it on invoices, GST returns and stock reports, not on the mill floor.
QA records: head rice and brokens
The US grade rules show what the mill is selling. Under 7 CFR 868.301, milled rice is rice from which the hulls and at least the outer bran layers have been removed: the husker takes the hull, the whitener and polisher take the bran. Whole kernels earn the price. The USDA Economic Research Service notes that brokens sell at a considerable discount to whole-kernel rice, and that care is needed through drying, storage and milling to keep them down. The same page notes that parboiling makes rice less likely to break during milling, so a parboiled lot that still breaks points to soaking, steaming or drying. 7 CFR 868.302 defines broken kernels as kernels of rice which are less than three-fourths of whole kernels.
Mill type moves these numbers a long way. A 2025 paper by Bangladesh Rice Research Institute engineers, in the Journal of Agricultural Machinery and Bioresources Engineering, notes that some compact rice mills reach only 55% or less milling recovery with 30% head rice, while commercial mills can reach 65% milling recovery with 55% head rice. These results come from samples in the lab, and they belong in QA records next to the intake moisture.
Machine controls and the colour sorter
The parboiling boiler, the dryers and the sorter each come with their own controls. The optical colour sorter is a separate product with its own software for ejector settings and reject rates. None of these is a mill-wide record of lost hours, but their run signals are the raw material for one.
OEE and light MES: lost hours by machine
This layer reads whether each main machine is running and asks the operator why it stopped. In a rice mill the useful machines to connect are the husker, the whitener and polisher line, the colour sorter, and every packing machine, because those are where hours vanish without a note in any register. From those records come availability, performance and quality per machine and shift, and the money a shift lost.
What you see: a shift timeline, unclassified time waiting for a reason, and the operator's line-down screen, on sample lines rather than a rice mill. Book a demo.
Plays from YouTube. Google may set cookies when you press play. Privacy policy.
How records move between rice mill systems
Two links matter more than the rest. Billing sends the packing order down to the floor, so the bagging line knows which brand and bag size it should be running. The floor sends back run hours, stop minutes and bags packed, so stock and production figures agree at the end of the shift. The sorter and dryer controls stay closed. At most, their run state tells the OEE layer when they stopped the line.
The same links decide how fast QA answers an export buyer who finds too many brokens in a lot of parboiled 25 kg bags. Paddy lots, soak and dryer batches, exit moisture, head rice results and bag codes must line up. In most mills the trace breaks in one of five places:
- paddy from several trucks mixed in one bin;
- the batch number never written on the dryer sheet;
- dryer exit moisture read by shift, not by batch;
- the head rice sample taken after the lot was bagged;
- the lot code printed by shift, not by lot.
Each break has the same cure: one lot code and one clock, from the bin to the bag.
Where a rice mill loses hours
The global stakes are large. The FAO Cereal Supply and Demand Brief of 6 November 2026 expects rice production to fall by 2.5 percent to 552.0 million tonnes (milled equivalent), citing poor producer margins and El Niño-related weather. When the crop is smaller, every tonne a mill can buy and turn into whole kernels counts for more.
In harvest months the parboiling and drying side sets the pace: soaked paddy waits for a steamer, steamed paddy waits for a free dryer, and the milling section runs out of feed. In the mill, rubber roll changes on the husker, screen and stone changes on the whitener, and sorter cleaning cycles take time that rarely reaches a register. In the packing hall the losses move again: film or bag supply, stitching heads, checkweigher rejects and bag size changes. For packing stops in detail, see VFFS bagger stops and palletizer OEE. Feed mills fight the same bagging losses; see OEE for animal feed mills.
Mill size sets the scale. A rice milling factsheet from Assam Agricultural University puts two-stage mills, with rubber roll hulling and a steel whitener, at 0.5 to 1 ton per hour of paddy input. The IRRI compact rice mill page makes the point from the other side: compared with the old husking mills, which cause high grain breakage, a compact mill can achieve at least a 5% increase in milling recovery. Larger commercial lines are rated well above 1 ton an hour, so each lost minute moves more paddy.
Rice mill failure modes
| Loss | Early sign in line data | Fix |
|---|---|---|
| Milling starved by the dryer | Husker stops booked as "no feed", clustered at the end of each dryer batch | Take the dryer's run state as a signal, stagger dryer batches, keep a buffer bin above the husker |
| Rubber roll wear on the husker | Speed drifting down over days, then a long stop for the roll change | Change rolls on a tonnage count, keep a set ready, time the change |
| Whitener screen and stone changes | Change minutes vary between crews, restarts slow | One written change sheet, timed and reviewed; see changeover time |
| Sorter cleaning cycles | Short sorter stops at regular intervals, booked as jams | Book cleaning as its own planned reason, check the cycle with the sorter vendor |
| Running below rated throughput | Tonnes per hour under the rating with no stops booked | Compare with the maker's rating; see reduced speed loss vs minor stops |
| Bagger stitching and film stops | Many stops under two minutes on one packer, rising with a new film or bag lot | Log stops by film or bag lot, set needles and thread on a count |
| Re-sorting milled rice | Tonnes sent back through the sorter rising on one shift | Check sorter settings and whitener pressure with QA |
Worked example: what one milling shift costs
Sample figures for illustration only. A parboiled rice mill runs a husker, whitener and polisher line rated at 6 tonnes of paddy an hour, or 100 kg a minute, on 8-hour shifts. The line counts paddy through a flow scale at the husker. Our OEE calculation guide shows each formula step by step.
| Step | Figure | How it is worked out |
|---|---|---|
| Planned production time | 450 min | 480 min shift minus 30 min planned: breaks 15, the sorter's scheduled cleaning cycles 15 |
| Stops | 90 min | No feed from the dryer 35, rubber roll change 25, whitener screen 15, elevator chokes 15 |
| Run time | 360 min | 450 minus 90 |
| Availability (A) | 80.0% | 360 / 450 |
| Ideal paddy in run time | 36.0 t | 360 min x 100 kg |
| Paddy milled | 32.4 t | From the flow scale |
| Performance (P) | 90.0% | 32.4 / 36.0 |
| Good first pass | 31.752 t | 32.4 t minus 2% of output sent back through the sorter, counted in paddy-equivalent tonnes: 0.648 t |
| Quality (Q) | 98.0% | 31.752 / 32.4 |
| OEE | 70.6% | 0.80 x 0.90 x 0.98 = 0.7056; check: 31.752 / (450 x 0.1 = 45.0 t) |
The sorter's cleaning cycles are planned, so they sit in the 30 planned minutes, not in availability. All tonnes are paddy-equivalent: the 0.648 t re-sorted is about 0.42 t of milled rice at 65% recovery. It is not lost product but capacity spent twice, valued below as if it had milled new paddy.
The gap to a perfect shift is 45.0 minus 31.752, or 13.248 tonnes of paddy. By loss: 9.0 t to the 90 stopped minutes, 3.6 t to slow running and 0.648 t to re-sorting. At a sample contribution of EUR 40 per tonne of paddy milled, after the paddy cost, the whole gap is worth EUR 529.92 a shift. Nobody recovers all of it, so price the part a team can act on.
Say the mill takes the dryer's run state as a signal, staggers its batches and keeps a set of rubber rolls ready. This is a harvest-month shift, so dryer starvation falls from 35 to 10 minutes and the roll change from 25 to 10: 40 minutes come back. At the shift's own speed and quality that is 40 x 100 kg x 0.90 x 0.98 = 3,528 kg of paddy. Outside harvest the mill runs stored, dried paddy, so only the 15 roll-change minutes come back: 15 x 100 kg x 0.90 x 0.98 = 1,323 kg a shift.
A month here is 42 shifts: 2 shifts a day on 21 working days. The year assumes 4 harvest months, milling all year from stored paddy, and a mill that can sell every extra tonne. At EUR 40 a tonne:
- Per harvest shift: 3.528 t x EUR 40 = EUR 141.12, or EUR 5,927.04 a harvest month.
- Per shift in other months: 1.323 t x EUR 40 = EUR 52.92, or EUR 2,222.64 a month.
- Per year, at 504 shifts (42 x 12): 4 x EUR 5,927.04 + 8 x EUR 2,222.64 = EUR 23,708.16 + EUR 17,781.12 = EUR 41,489.28.
- New OEE on a harvest shift: 35.28 t / 45.0 t = 78.4%, with availability up from 80.0% to 88.9%.
Head rice is the other lever. Where the lab reports head rice against paddy, one point of yield on the shift's 32.4 t is 324 kg moving between the whole-kernel price and the broken discount.
Which rice mill software to buy first
A mill needs its billing system before anything else, because nobody can run without paying farmers. After that, the order depends on what is leaking.
| What hurts most | Start with | Why |
|---|---|---|
| Bills, agent accounts and tax returns done by hand | Billing and stock software | It is the money record of the mill |
| Paddy and rice stock never match the books | A stock module or WMS | Bag counts by lot and godown need one home |
| Export buyers reject lots for brokens | QA records and process work on drying and milling | Brokens start in drying and milling settings |
| Milling section idle for hours with no reason logged | OEE and light MES on the husker and whitener | Machine signals time the stops; operators add the reason |
| Bagging line packs far below its rated bags a minute | OEE on the packing line | Splits film, stitching, weigher and changeover losses |
| Discoloured or foreign grains in finished bags | The sorter vendor's service and settings | Sorting quality is the sorter's job |
Book a demo to see how a husker's stops, a bagger's counts and the money they cost appear on one shift timeline.
Rice mill management software: questions to ask any vendor
| Ask | How to test the answer |
|---|---|
| Is this billing and stock software, or does it record machine time? | Ask to see a whitener stop from last night. If the demo only shows invoices, it is the first kind. |
| How are moisture deductions calculated on a purchase bill? | Give a slip with a moisture reading and check the bill against your own rule. |
| Which billing fields does the floor layer read? | Brands, bag sizes and packing orders in; bags packed out. Ask who keeps that link. |
| Can it set a rated speed per bag size on one packer? | Ask for 5 kg and 25 kg on the same machine, each with its own bags a minute. |
| How does a sorter cleaning cycle show up? | Ask for it as its own reason, apart from a jam, so the sorter's planned time is visible. |
| How are parboiling batches and dryers modelled? | Ask to see them as separate assets, so a full dryer shows as the reason the mill starved. |
What to do this week and this quarter
This week, for the mill or production manager:
- Add up last week's stop minutes on the husker and whitener by cause: no feed, roll change, screen change, sorter cleaning, breakdowns.
- Time one rubber roll change, from stop to rated throughput.
- Write down the rated tonnes per hour for the milling line and the rated bags a minute for each packer and bag size.
- Ask QA for the last month's head rice results by shift and by dryer batch.
This quarter:
- Put a run signal on the husker, the whitener and the main bagger, and take the dryer's run state so starvation is booked as its own reason.
- Agree 8 to 12 stop reasons with the crews, in their own words.
- Price one tonne of paddy milled with accounts, as in the worked example.
- Set a target on the largest loss, such as halving dryer starvation, and review it weekly.
- Send run hours and bags packed to the billing and stock software.
Fabrico in a rice mill
Fabrico is a cloud OEE and light MES platform. In a rice mill it does three jobs:
- Machine running and stop time: the husker, whitener and polisher, sorter and dryers report run state from a PLC, sensor or counter. Operators choose why it stopped on a tablet or phone: roll change, screen change, sorter cleaning, no feed from the dryer.
- Bagging line OEE: each packer gets a rated speed per bag size, so a 1 kg pouch line and a 50 kg bag line are judged on their own numbers, with changeovers, film and stitching stops kept apart.
- Data out: run hours, stop minutes and bags packed leave through a REST API, webhooks, or Excel and CSV export, for billing and stock software to use.
Where bags are stitched or loaded by hand and no machine count exists, the camera add-on counts output. Where a camera covers the station, the video for the minute of a stop can be opened from the shift timeline, streamed on request and not stored in Fabrico. The computer vision add-on page and the FMCG camera guide explain how those counts work. Platform details sit on the MES and OEE software page.
Billing, weighbridge slips, moisture testing, head rice results and sorter settings stay in the billing software, the QA lab and the sorter. Quality inspection is not part of Fabrico. Production planning and scheduling are not part of Fabrico today. For the wider food plant map, see food manufacturing software.
Questions rice mill managers ask
Is rice mill billing software the same as production software?
No. Billing software handles paddy purchase, invoices, tax and stock. Production software records when the machines ran and why they stopped. A mill can need both, and they are bought from different kinds of vendors.
Where does head rice yield belong?
In QA records. Head rice and broken percentage come from lab samples. OEE software counts bags packed and the time the line ran, so it shows output lost to stops, not kernels lost to breakage.
Which machine should a rice mill connect first?
Start where the mill usually waits: the whitener line if milling starves, or the main bagger if finished rice piles up before packing. Add the husker and sorter once the first machine's reasons are trusted.
Does a small rice mill need OEE at all?
Only when lost hours cost more than the software. A mill with one shift and one bagger can start with a paper stop register for a month, then decide whether a digital one would pay.
Does Fabrico work alongside a colour sorter?
Yes, as a reader. It can take the sorter's run state to time its stops and cleaning cycles. Sorter settings, ejectors and reject rates stay in the sorter's own software.
Want to see where milling hours go? Book a demo to see a husker and bagger shift as run time, stops and money lost.
Related articles
Latest from our blog


Real Fabrico tiles, sample data.