


 Login
 Blog
Packaging Manufacturing Software: What Each System Does and What to Buy First

In short: packaging manufacturing software is not one product. A packaging plant can run up to seven kinds: OEE and line monitoring, MES, ERP, planning and scheduling, quality, maintenance and warehouse.
- Your pain is lines that stop, run slow or waste material, and nobody can say why: start with line data, OEE and stop reasons, such as a light MES.
- Your pain is quoting, job costing or stock: buy an industry ERP for packaging first.
- Fabrico is a light MES with OEE. It is not an ERP, and it does no estimating, scheduling or warehouse work.
- Buy in the order of your biggest loss, and give each number one owner system.
Search for packaging manufacturing software and you get ERP suites, MES products, inspection apps and design tools on one page. They do different jobs.
This page is a map for a plant or operations manager. It says what each kind of software does, which problem tells you that you need it, and what to buy first.
We sell Fabrico, a light MES with OEE, so we mark clearly where it fits and who should buy something else.
The seven kinds of software a packaging plant runs
The names overlap and suppliers bundle them in different ways, but the jobs underneath stay much the same.
| Software | What it does | You need it when |
|---|---|---|
| OEE and production monitoring | Reads the line: stops, speed, counts, good output, by line and shift | Lines stop or run slow and the reasons are guesses |
| MES | Runs and records the job on the floor: what ran, where, how many, with which material | The office learns what happened on the floor a day later, from paper |
| ERP (in print and packaging often called MIS) | Estimates, quotes, orders, purchasing, stock, job costing, invoices | Quotes take days, or you cannot say which jobs made money |
| Planning and scheduling | Puts jobs in order on each machine, against capacity and due dates | Due dates slip, or changeovers pile up because similar jobs are not grouped |
| Quality | Specs, checks, test results, complaints and corrective actions | Customer audits and complaints take too long to answer |
| Maintenance | Work orders, planned upkeep, spare parts | Planned jobs get missed and spares are not there when needed |
| Warehouse | Locations, reels, pallets, picking and dispatch | People walk the aisles looking for stock the system says you have |
A light MES covers the OEE and MES rows for the lines, without the project of a full suite. Our guide to light MES explains the difference.
The split between business systems and floor systems is not our idea. ISA-95 is the standard behind it, and ISA says of it: "It organizes technology and business processes into layers".
In that model, running the business sits at level 4 and MES sits at level 3, above the machines and their controls.
Where a light MES with OEE fits
An ERP knows what a job should take, and the line knows what it took. A light MES with OEE shows that gap in five numbers.
- Downtime: stops, each with a start, an end and a reason, such as jams, faults, or waiting for board, film or pallets.
- Speed loss: the line runs, but below the rated speed for this product. Very short stops land here too, see our guide to micro-stops.
- Changeovers: from the last good pack of one job to the first good pack of the next. With short runs, this can be one of the biggest losses in a converting plant.
- Waste: setup waste and running waste, counted apart if you can.
- Good count: what you can ship, against what the line could have made.
OEE puts these into one figure: availability x performance x quality. The OEE calculation guide has the formulas in full.
For more depth, see our pages on MES for packaging manufacturers and on OEE software for packaging lines.
Worked example: one folder-gluer, one shift
Example data, not a customer. A folder-gluer runs cartons at a rated speed of 200 a minute for this job.
The shift is 480 minutes with a 30 minute break, so planned time is 450 minutes.
| Item (example data) | Value |
|---|---|
| 2 job changes, 40 minutes each | 80 minutes |
| Waiting for board and pallets | 20 minutes |
| Jams and faults | 30 minutes |
| Run time | 450 - 130 = 320 minutes |
| Cartons made | 54,400 |
| Waste | 1,088 |
| Good cartons | 53,312 |
- Availability: 320 / 450 = 71.1%.
- Performance: 54,400 / (320 x 200 = 64,000) = 85.0%.
- Quality: 53,312 / 54,400 = 98.0%.
- OEE: 0.711 x 0.850 x 0.980 = 59.2%. Check: 53,312 good cartons / (450 x 200 = 90,000) = 59.2%.
What this shift tells you
Stops took 130 minutes, and a careful shift log would show most of them. Slow running took another 48 minutes, and a job ticket does not show that.
Now say each job change drops from 40 to 30 minutes, and all else stays the same. Run time becomes 340 minutes, so at the same 170 cartons a minute the line makes 57,800, and about 56,644 are good.
That is about 3,300 more good cartons in the shift, and OEE goes to about 62.9%. It only pays if there are orders to fill the time, so put your own margin on it with the field guide to pricing a stopped hour.
Industry ERPs for packaging: what they cover
Packaging and converting has its own ERP products, built around things like board grades, reel widths and tooling.
Software Connect, in a roundup of packaging ERP updated in September 2026, sums up the category like this: "It connects quoting, inventory, scheduling, production, and shipping into one system".
Here is how some of these products are described, on their own sites or by that roundup. We read each page on 10 November 2026.
| Product | Described as | Whose words |
|---|---|---|
| ePS CommandCore | ERP foundation: "Estimating, orders, materials, tooling & costing" | Its own site |
| Amtech EnCore | "For corrugated and folding carton manufacturers connecting estimating, scheduling, plant operations" | Its own site |
| Advantive Advantzware | "tailored solutions for corrugated and folding cartons" | Software Connect |
| ePS Packaging Suite, powered by Radius | "an ERP and MIS platform built for flexible packaging manufacturers" | Software Connect |
| Amtech Label Traxx | "an ERP with a built-in MIS platform for label and tag manufacturers" | Software Connect |
| DELMIAWorks | "designed specifically for discrete manufacturing industries like plastic packaging companies" | Software Connect |
This is a sample to show the shape of the category, not a ranking and not advice to buy any of them. We have not tested these products, so ask each supplier directly about anything not quoted here.
Some of these suites also list shop floor parts of their own. The ePS page, for example, lists "Machine data capture, waste tracking, closed-loop control" under its control systems.
So the question is often not ERP or MES. It is which system you trust for the line numbers, and how soon you need them.
What to buy first
Buy in the order of your biggest loss, not in the order of the sales calls you get. Start from the symptom.
| If this is your week | Start with |
|---|---|
| Lines stop and run slow, and the shift log says "various" | OEE and line monitoring, such as a light MES |
| Waste is high, and you cannot say on which job, machine or shift | Line data with waste and good count per job |
| The plan changes three times a day, and nobody trusts the run rates in it | Line data first, then scheduling fed with real rates |
| Quotes are slow, prices are guesses, and you find out a job lost money after it shipped | An industry ERP for packaging |
| Orders live in spreadsheets, and stock on the screen does not match stock on the floor | ERP, then warehouse |
| Customers audit you, and each complaint takes days of paper to answer | Quality, with lot tracking in ERP or MES |
| The same machine breaks every month, and planned upkeep slips | Maintenance software |
Our first rule of thumb: measure before you plan. A scheduling tool fed with wrong speeds and wrong changeover times gives a neat plan that the floor cannot keep.
Our second: do not start the biggest project to fix the smallest problem. An ERP replacement usually touches the whole company, so it is a slow way to find out why line 3 stops.
How to choose: three checks
- Ask where each number comes from. A stop time typed in at the end of the shift is a memory. A stop time from the machine signal is a measurement.
- Check the machine side. Some packaging machines follow PackML, which OMAC calls "The automation standard that makes it easier to transfer and retrieve consistent machine data." Ask every supplier how they read your older machines too.
- Decide who owns each number. Good count in the ERP and good count on the line screen must not disagree, so pick one source.
Who should buy something else
- Your pain is estimating, quoting and job costing. You need a packaging ERP first. Fabrico does none of this.
- You need stock, reels and pallets under control. That is ERP inventory or a warehouse system.
- You need a finite schedule across corrugators, presses or lines. Buy a scheduling tool or a suite that has one. Planning and scheduling are not part of Fabrico today.
- Your lines already report stops, speed and waste you trust. Then line data is not your gap, so spend the money where the gap is.
In all of these, Fabrico is the wrong first buy.
Common mistakes
- Hiding changeovers in planned time. OEE looks better, and what may be the biggest loss in a short-run plant drops out of view.
- One rated speed for every product. Set it per product and pack size, or the performance figure means little.
Where Fabrico fits, and where it stops
Fabrico is a cloud-based light MES with OEE. On the map above, it sits in the row that reads the line.
- Stops: they come from the machine signal, through a PLC or a Fabrico IoT device. The operator adds the reason on a tablet or phone.
- OEE: availability, performance and quality per line and shift, so speed loss and waste sit next to downtime.
- Changeovers: a changeover shows up as a stop with its reason, so you can see its time.
- Parts: AI cameras (an add-on) count parts. You can open the camera video for that minute.
- Camera video: in the standard setup it is streamed, not stored in Fabrico.
- Maintenance: a maintenance module exists, as a complement.
What Fabrico does not do: it is not an ERP or a warehouse system, and it does no estimating, quoting or job costing. Production planning and scheduling are not part of Fabrico today.
Ficosota (also a Fabrico investor) raised OEE from 53.1% to 59.6% on 16 lines, June to September 2026, with monthly good output up 23.2%. That is one company, not a benchmark for your plant.
See the MES and OEE overview for the screens.
Want to see it on lines like yours? Book a demo or Contact us.
What people ask next
Is a packaging ERP the same as an MES?
No. The ERP runs the business side (quotes, orders, stock and cost), while an MES runs and records the work on the floor.
Some packaging suites sell both, so ask what each module records and where its numbers come from. Our guide to MES software covers the full scope.
My ERP has a shop floor module. Do I still need OEE software?
Check one shift by hand. If the module's stop minutes match what the machine did, short stops included, you may not need more.
If operators type the times in at the end of a job, expect it to miss short stops and slow running.
Which OEE software is best for a packaging plant?
That depends on your machines, your line speeds and how much you want to connect. Our review of OEE software compares the options.
Should a small converter start with ERP or with line data?
Start where the money leaks. If you lose it in quoting and costing, ERP comes first, and if you lose it in stopped and slow lines, line data comes first.
Line data is usually the smaller project of the two, and you can try it on one line.
Packaging lines losing hours you cannot name? Book a demo or Contact us.
Related articles
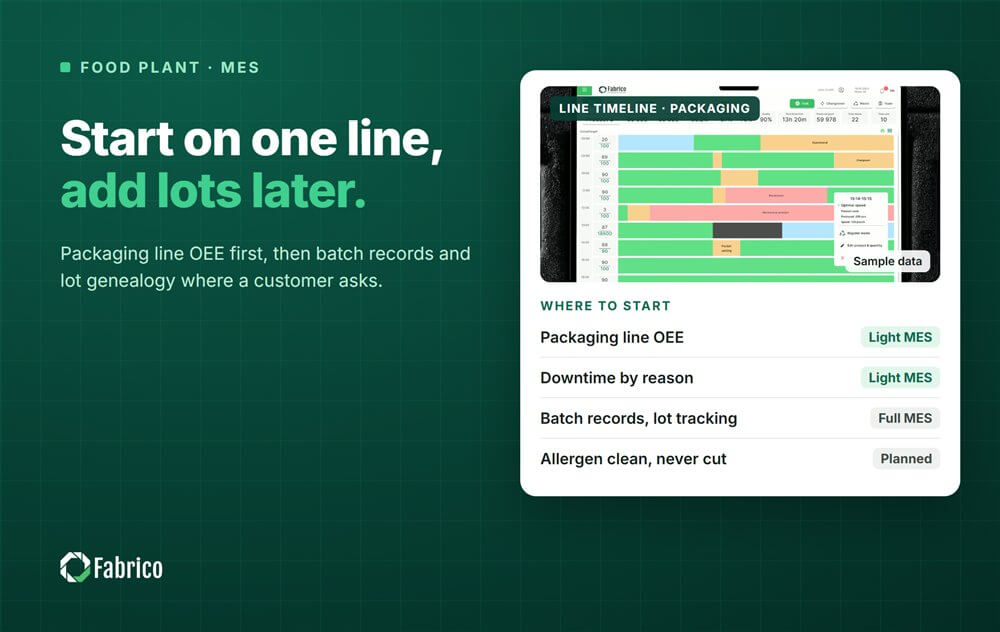

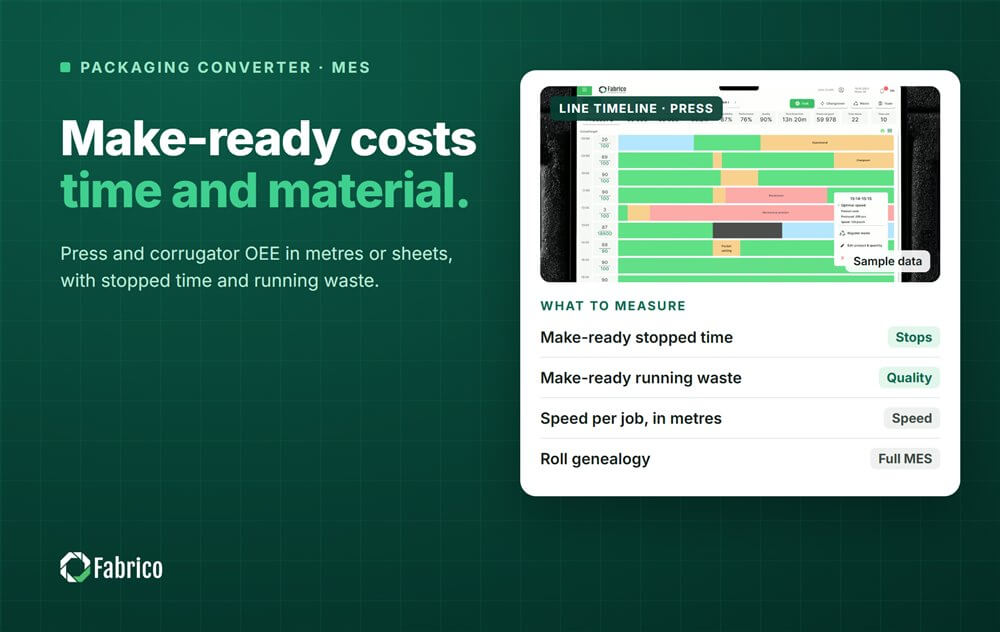


Real Fabrico tiles, sample data.