


 Login
 Blog
Rice Mill Software: Billing and Stock vs Mill Floor Monitoring

In short: rice mill software is not one product. A mill buys billing and stock software for paddy purchase, invoices and godown stock, a weighbridge system at the gate, QA records for moisture, head rice and brokens, the colour sorter's own controls, and an OEE or light MES layer that shows when the husker, whitener, polisher and bagging line were running or stopped. Buy the one that fixes the problem costing you most this season.
- If rice mill management software means billing, paddy procurement and stock to you, that is an ERP category, not production monitoring.
- Head rice yield and broken percentage live in QA and process records. OEE software does not measure them.
- Machine running and stop time, and the OEE of the packing line from 1 kg pouches to 50 kg bags, are the floor layer. That is where Fabrico sits.
- Parboiling and drying set the pace in harvest months, so buy before the paddy arrives, not during it.
A rice mill earns its margin twice. Once when paddy is bought at the right moisture and price, and once when that paddy leaves the mill as whole, white, sorted kernels in the right bag. Software is sold for both moments, and the two kinds rarely talk to each other.
If you searched for rice mill software to print bills, track paddy from farmers and agents, and see godown stock, you are shopping for a billing and stock system. If you want to know why the whitener stood idle for two hours on the night shift, or why the 25 kg bagger packs fewer bags than its nameplate says, you need production monitoring. This page maps both, so you can buy the right one first.
Fabrico makes the second kind: OEE and light MES for the mill floor and the packing hall. It does not do billing, procurement or yield testing, and the map below says who does.
Rice mill software, system by system
Each system below holds a record that someone in the mill must answer for: the accountant for the farmer's payment, QA for the broken count in an export lot, the shift in charge for lost hours. Keep that owner in mind when a vendor promises to cover several rows.
| System | What it does in a rice mill | Owner | Fabrico? |
|---|---|---|---|
| Billing, procurement and stock | Paddy purchase from farmers or agents, moisture deductions, invoices and tax, stock of paddy, rice, bran and husk | Accounts, purchase | No |
| Weighbridge software | Gross and tare per truck at the gate, the slip that billing uses | Stores, gate | No |
| QA lab records | Intake moisture, head rice and broken percentage per sample, chalky and discoloured grains | QA | No |
| Machine and dryer controls | PLC or HMI on the parboiling boiler, dryers, huskers and whiteners | Process, maintenance | Reads run signals only |
| Colour sorter software | Ejector settings, reject rates and cleaning cycles inside the optical sorter | Sorter vendor, QA | No |
| Stock module or WMS | Finished bags by grade, brand and lot, godown location, dispatch | Stores, logistics | No |
| OEE and light MES | Run and stop time at the husker, whitener, polisher, sorter and packers; bagging line OEE | Operations, CI | Yes, this is Fabrico |
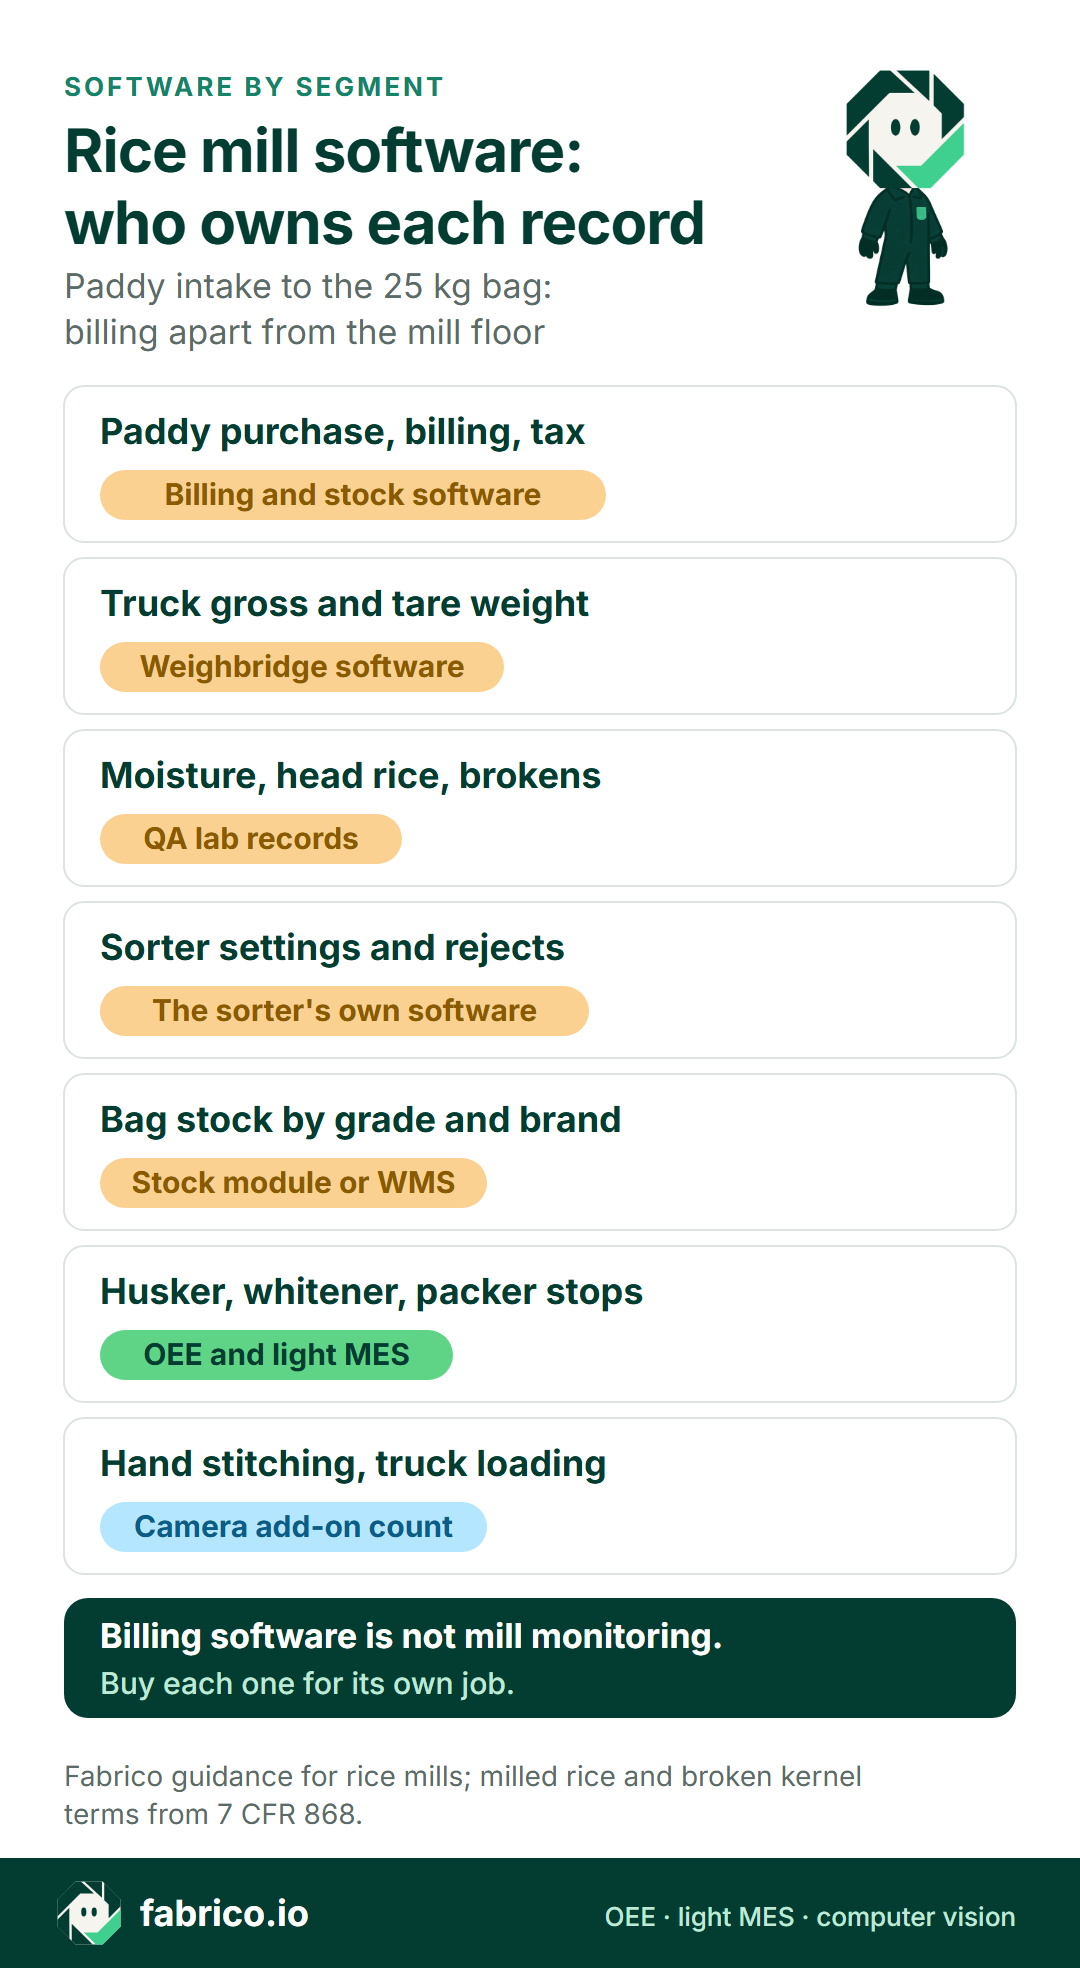
Text version of this infographic
- Paddy purchase, billing and tax: billing and stock software.
- Truck gross and tare weight: weighbridge software.
- Moisture, head rice and brokens: QA lab records.
- Sorter settings and rejects: the sorter's own software.
- Bag stock by grade and brand: stock module or WMS.
- Husker, whitener and packer stops: OEE and light MES.
- Hand stitching and truck loading: camera add-on count.
- Footer: billing software is not mill monitoring. Buy each one for its own job.
Billing, procurement and stock: what most rice mill software lists mean
This is the system a small mill buys first, and for good reason. It turns a weighbridge slip and a moisture reading into a purchase bill, keeps farmer and agent accounts, and tracks how many quintals of paddy, how many bags of rice and how much bran and husk sit in the godown. Some packages add hulling-on-charge for custom milling. It is accounting and stock software. Judge it on invoices, tax returns and stock reports, not on the mill floor.
QA records: head rice and brokens
The US grade rules show what the mill is selling. Under 7 CFR 868.301, milled rice is rice from which the hulls and at least the outer bran layers have been removed: the husker takes the hull, the whitener and polisher take the bran. Whole kernels earn the price. The USDA Economic Research Service notes that brokens sell at a considerable discount to whole-kernel rice, and that care is needed through drying, storage and milling to keep them down. US grade rules in 7 CFR 868.302 define broken kernels as kernels of rice which are less than three-fourths of whole kernels. These results come from samples in the lab, and they belong in QA records next to the intake moisture, whatever the grading machines on the floor do.
Machine controls and the colour sorter
The parboiling boiler, the dryers and the sorter each come with their own controls. The optical colour sorter is a separate product with its own software for ejector settings and reject rates. None of these is a mill-wide record of lost hours, but their run signals are the raw material for one.
OEE and light MES: lost hours by machine
This layer reads whether each main machine is running and asks the operator why it stopped. In a rice mill the useful machines to connect are the husker, the whitener and polisher line, the colour sorter, and every packing machine, because those are where hours vanish without a note in any register.
How records move between rice mill systems
Two links matter more than the rest. Billing sends the packing order down to the floor, so the bagging line knows which brand and bag size it should be running. The floor sends back run hours, stop minutes and bags packed, so stock and production figures agree at the end of the shift. The sorter and dryer controls stay closed. At most, their run state tells the OEE layer when they stopped the line.
Where a rice mill loses hours, briefly
In harvest months the parboiling and drying side sets the pace: soaked paddy waits for a steamer, steamed paddy waits for a free dryer, and the milling section runs out of feed. In the mill, rubber roll changes on the husker, screen and stone changes on the whitener, and sorter cleaning cycles take time that rarely reaches a register. In the packing hall the losses move again: film or bag supply, stitching heads, checkweigher rejects and the change from 1 kg pouches to 25 kg or 50 kg bags. Yield and brokens are a different loss, measured in the lab. For packing stops in detail, see VFFS bagger stops and palletizer OEE. A worked mill shift with bagging is in OEE for animal feed mills.
Which rice mill software to buy first
A mill needs its billing system before anything else, because nobody can run without paying farmers. After that, the order depends on what is leaking.
| What hurts most | Start with | Why |
|---|---|---|
| Bills, agent accounts and tax returns done by hand | Billing and stock software | It is the money record of the mill |
| Paddy and rice stock never match the books | A stock module or WMS | Bag counts by lot and godown need one home |
| Export buyers reject lots for brokens | QA records and process work on drying and milling | Brokens are a yield problem, measured in the lab |
| Milling section idle for hours with no reason logged | OEE and light MES on the husker and whitener | Machine signals time the stops; operators add the reason |
| Bagging line packs far below its rated bags a minute | OEE on the packing line | Splits film, stitching, weigher and changeover losses |
| Discoloured or foreign grains in finished bags | The sorter vendor's service and settings | Sorting quality is the sorter's job |
Bring one week of husker and packing stop notes, and a sample bag-size change, to a Fabrico demo, and we will show what the floor layer fills and what stays in billing and QA.
Worked example: one export lot of parboiled rice, traced
An invented case, from no real mill. A buyer's inspector finds too many broken kernels in a lot of parboiled 25 kg bags and asks for the history. Parboiling should help, since the USDA notes it makes rice less likely to break during milling, so QA must show where it went wrong: which paddy went in, how it was soaked and dried, what the lab measured, and which bags carry that lot.
| Record | Held in | Where the hand-off breaks |
|---|---|---|
| Paddy lots and suppliers | Billing and stock software | Paddy from several trucks mixed in one bin |
| Soak and steam times | Boiler HMI or a paper log | Batch number never written on the dryer sheet |
| Dryer exit moisture | QA lab records | Readings by shift, not by batch |
| Head rice and broken percentage | QA lab records | Sample taken after the lot was bagged |
| Bags of the lot and their godown | Stock module or WMS | Lot code printed by shift, not by lot |
| Run and stop times, bags packed | OEE and light MES | Holds no lot or yield record, only run data |
The trace breaks where bins, batches and bag codes use different numbers. Fabrico is not part of the trace; it supplies only when the machines ran, when they stopped, and how many bags the line counted. The OEE maths for a mill line with a bagger is shown in OEE for animal feed mills.
Rice mill management software: questions to ask any vendor
Put these to each vendor on the shortlist, with a week of mill registers and one season's purchase bills on the table.
| Ask | How to test the answer |
|---|---|
| Is this billing and stock software, or does it record machine time? | Ask to see a whitener stop from last night. If the demo only shows invoices, it is the first kind. |
| How are moisture deductions calculated on a purchase bill? | Give a slip with a moisture reading and check the bill against your own rule. |
| Where do head rice and broken results live? | They should sit with QA samples by lot, not inside a stop log. |
| Can it set a rated speed per bag size on one packer? | Ask for 5 kg and 25 kg on the same machine, each with its own bags a minute. |
| How does a sorter cleaning cycle show up? | Ask for it as its own reason, apart from a jam, so the sorter's planned time is visible. |
| Which billing fields does the floor layer read? | Brands, bag sizes and packing orders in; bags packed out. Ask who keeps that link. |
| How are parboiling batches and dryers modelled? | Ask to see them as separate assets, so a full dryer shows as the reason the mill starved. |
Where Fabrico fits in a rice mill
Fabrico is a cloud OEE and light MES platform. In a rice mill it does three jobs:
- Machine running and stop time: the husker, whitener and polisher, sorter and dryers report run state from a PLC, sensor or counter. Operators choose why it stopped on a tablet or phone: roll change, screen change, sorter cleaning, no feed from the dryer.
- Bagging line OEE: each packer gets a rated speed per bag size, so a 1 kg pouch line and a 50 kg bag line are judged on their own numbers, with changeovers, film and stitching stops kept apart.
- Data out: run hours, stop minutes and bags packed leave through a REST API, webhooks, or Excel and CSV export, for billing and stock software to use.
Where bags are stitched or loaded by hand and no machine count exists, the camera add-on counts output. Its video can be opened for a moment on the shift timeline, streamed on request and not stored in Fabrico. The computer vision add-on page and the FMCG camera guide explain how those counts work. Platform details sit on the MES and OEE software page.
What Fabrico does not do: paddy purchase, billing or tax, weighbridge slips, moisture testing, head rice or broken measurement, sorter control, and grading or inspection of any kind. Those stay in your billing software, the QA lab and the sorter. The milling plan stays with your mill manager and the billing and stock system. For the wider food plant map, see food manufacturing software.
What people ask next
Is rice mill billing software the same as production software?
No. Billing software handles paddy purchase, invoices, tax and stock. Production software records when the machines ran and why they stopped. A mill can need both, and they are bought from different kinds of vendors.
Can OEE software measure head rice yield?
No. Head rice and broken percentage come from lab samples and belong in QA records. OEE software counts bags packed and the time the line ran, so it can show output lost to stops, not kernels lost to breakage.
Which machine should a rice mill connect first?
Start where the mill usually waits: the whitener line if milling starves, or the main bagger if finished rice piles up before packing. Add the husker and sorter once the first machine's reasons are trusted.
Does a small rice mill need OEE at all?
Only when lost hours cost more than the software. A mill with one shift and one bagger can start with a paper stop register for a month, then decide whether a digital one would pay.
Does Fabrico work alongside a colour sorter?
Yes, as a reader. It can take the sorter's run state to time its stops and cleaning cycles. Sorter settings, ejectors and reject rates stay in the sorter's own software.
Does Fabrico handle paddy purchase or GST billing?
No. Purchase bills, agent accounts and tax returns stay in your billing and stock software. Fabrico can send it bags packed and run hours.
Want to see a mill shift as run time and stops? Book a demo with one week of husker and bagger registers.
Related articles
Latest from our blog


Real Fabrico tiles, sample data.