Login
CNC plant: OEE 20% to 62% in three months, no PLC changes
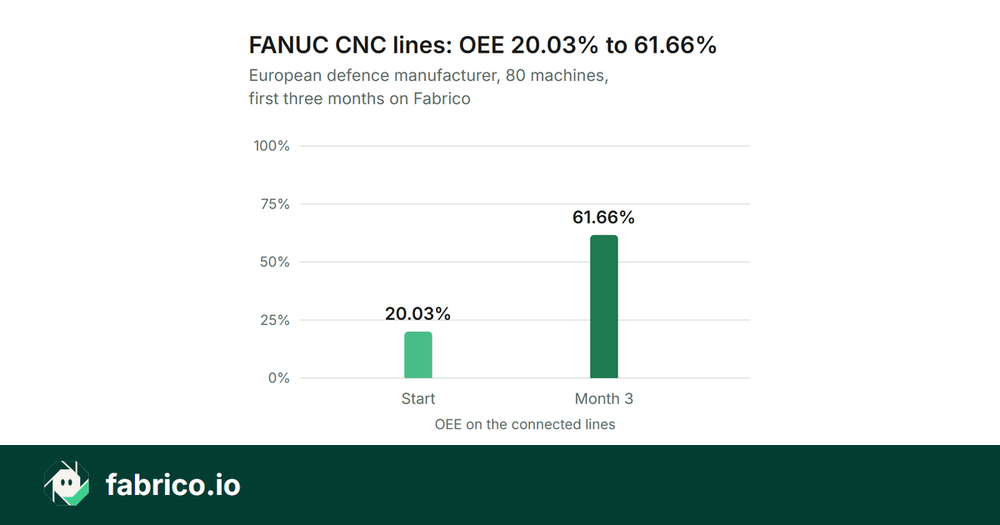
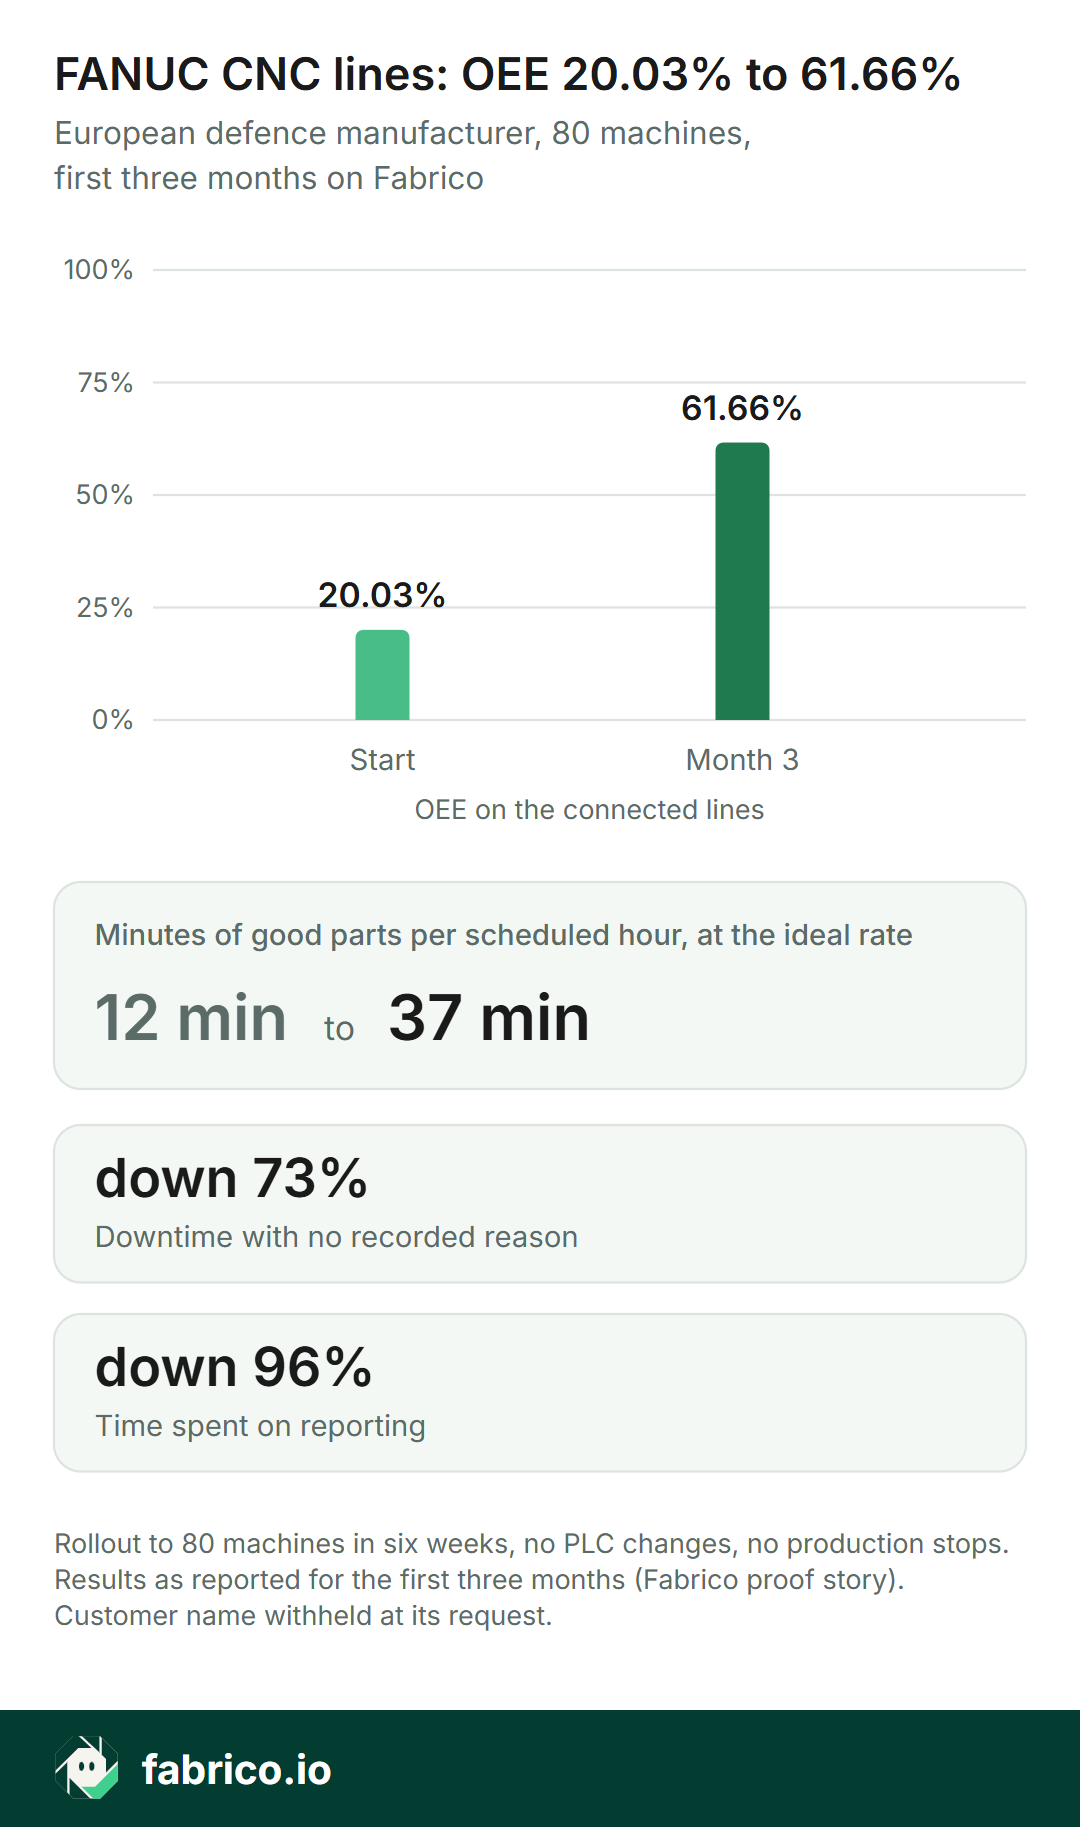
On its FANUC CNC lines, a European defence manufacturer went from 20.03% to 61.66% OEE in the first three months, with the rollout reaching 80 machines in six weeks, nothing changed in the control logic and no production stops. Results as reported for the first three months; the customer's name is withheld at its request.
- Company: a European defence manufacturer. Name withheld at its request.
- Machines: FANUC CNC lines; the rollout reached 80 machines in six weeks.
- In Fabrico: MES and OEE, rolled out with the implementation partner Nexus IIOT.
- Period: the first three months, as reported; the rollout to 80 machines took the first six weeks of it.
- Where the numbers come from: Fabrico's published proof story (PDF on this page); results as reported for the first three months.
The problem: twelve minutes of good parts in every scheduled hour
At 20.03% OEE, the lines made about one fifth of what they could have made in the time they were planned to run: for every scheduled hour, about 12 minutes of good parts at the ideal rate.
Stops without a recorded reason cannot be priced, ranked or fixed, so the first job was to see the stops.
The rollout: connect the machines, change nothing on them
The plant and Nexus IIOT connected the FANUC CNC lines without touching the control logic and without stopping production. The rollout reached 80 machines in six weeks.
In Fabrico, a stop on a connected machine is logged from the machine signal and the operator adds the reason. Over the first three months the plant reported 73% less downtime without a reason and 96% less time spent on reporting, which is hours back for the people who solve problems.
What the plant reported
Once stops had reasons, the biggest losses were obvious. The reported result after three months: about three times the good output from the same machines and the same scheduled hours.
The results, first three months
| Measure | From | To | Change |
|---|---|---|---|
| OEE on the FANUC CNC lines | 20.03% | 61.66% | +41.63 points |
Same lines, same scheduled hours. Results as reported for the first three months.
Also reported for the same three months: downtime with no recorded reason down 73%; time spent on reporting down 96%. The absolute values are not in the published proof story.
What the numbers mean:
- OEE: how much of planned production time became good parts at the ideal rate (availability x performance x quality). At 20.03% that is about 12 minutes of good parts per scheduled hour; at 61.66% about 37.
- Downtime with no recorded reason: stop time with no reason attached, so it could not be ranked or priced.
- Time spent on reporting: the hours people spent assembling the figures by hand.
Download the proof story (PDF, PowerPoint)
Three things to keep in mind:
- Both OEE values are as reported for the first three months.
- About three times the good output from the same machines means the extra parts came from the same scheduled hours. Extra output becomes profit when you can sell it; if you cannot, the same gain comes back as fewer hours and less overtime.
- Fabrico provides the measurement. The gain came from what the plant did once it could see and rank its stops.
Why the name is withheld
The customer asked for its name to be withheld. The figures are published as reported, with the implementation partner named.
Next step: one of your CNC lines
Bring one line and one week of stops. On a demonstration line we show how a stop gets its reason, how the losses rank and, with the financial impact module, what each one costs. If your machines are FANUC or another CNC, ask how a line connects with no change to the control.
See how businesses benefit


Real Fabrico tiles, sample data.