


 Login
 Blog
Production Monitoring Software: How It Works, What to Track and 6 Tools (2026)

TL;DR
Production monitoring software shows during the shift what each connected line is doing: running, stopped or running slow, good parts against target, and the reason tagged for a stop. It reads run, stop and count signals from the PLC or a retrofit sensor, with a camera counting parts where there is no signal, and turns them into OEE by line and shift, which is why the same tools are also sold as OEE monitoring software.
Below: how it works on the shop floor, who uses it, the main approaches, 6 tools compared (plus Fabrico, which we sell and do not rank) and the questions to ask in a demo.
- "Real time" only helps if the data arrives while the shift can still react, and if short stops are captured instead of averaged away.
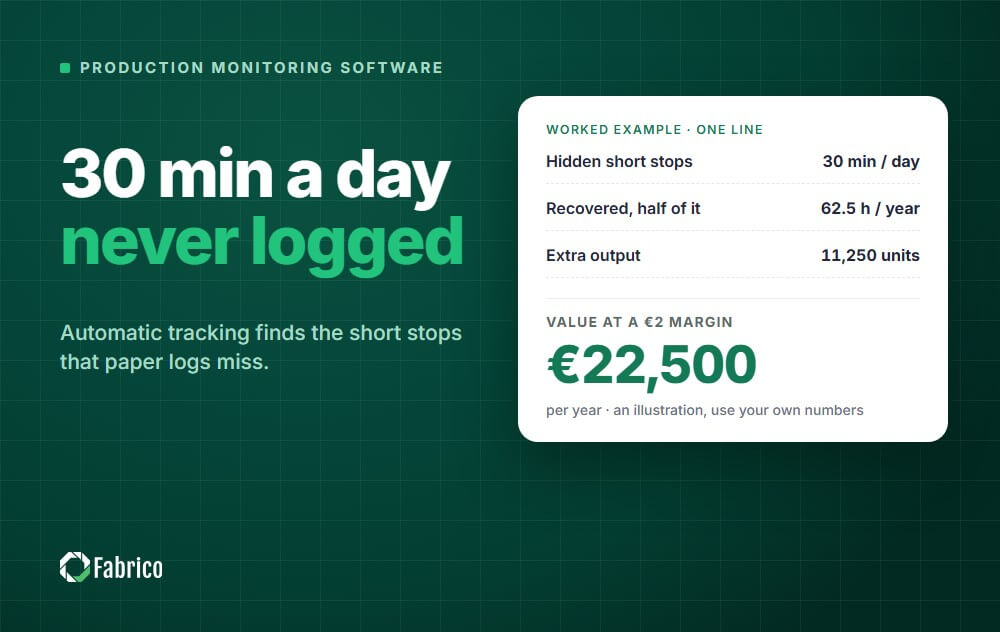
- Automatic tracking can show stops that paper logs miss. The worked example below turns 30 hidden minutes a day into a business case.
- Each vendor description is based on the vendor's own website, checked in September 2026. The "Things to consider" notes are our own suggestions, and Fabrico is our product.
- Once one bottleneck machine is reporting, run a pilot with a written scorecard before you roll anything out.
What is production monitoring software?
Production monitoring software collects data from manufacturing equipment and shows it on live dashboards, so supervisors, operators and maintenance see the same picture during the shift.
Most tools track machine state, part counts, cycle times and stops, and calculate OEE from them, which is why the category overlaps with OEE monitoring software.
Production tracking software is a closely related term. It often puts more weight on orders, jobs and operator input, while monitoring puts more weight on machine data.
In Fabrico, connected machines report their own stops from the PLC or a Fabrico IoT device with external sensors, and AI cameras (an add-on) count parts where there is no signal; see how Fabrico connects machines. For what each record should contain and how to roll it out, see our guide to production tracking software.
Many tools do both, so compare them by what they actually capture, not by the label.
If OEE is the number you want to run the plant on, see how Fabrico's OEE software tracks it by line and shift from live machine data.
If you need machine data, downtime and OEE but not scheduling or genealogy, read what a light MES covers and where it stops.
What "real time" has to mean
Every tool in this guide says real time on its website. Before you compare tools, agree on what the word must mean on your shop floor.
| Test | Why it matters | How to check it in a demo |
|---|---|---|
| Machine state updates during the stop | A supervisor can only react to a stop while it is happening | Stop a machine and time how long the dashboard takes to change |
| Stops have a start and an end time | Durations are what you add up in a Pareto chart | Ask to see the raw event list for one shift |
| Short stops are captured, not averaged | Short stops often hide inside "slow running" | Trigger three short stops and look for three events |
| Counts come from the machine | Manual counts drift and arrive late | Compare the count with a manual count over one hour |
| The right person is told | A dashboard nobody watches changes nothing | Ask who gets notified about a long stop, and how |
If a tool passes all five, it gives you real time you can act on. If it only refreshes a report every hour, it is fast reporting, not monitoring. For that job, see our guide to production reporting software.
What to track on every machine
| Data point | Usual source | What you use it for |
|---|---|---|
| Machine state (running, stopped, changeover) | PLC or sensor | Availability and the downtime timeline |
| Part count | PLC counter, sensor or AI camera (an add-on) | Output and performance |
| Cycle time | Calculated from counts or read from the PLC | Slow running against the ideal cycle time |
| Stop reason | Operator on a tablet or phone | Knowing why, not only how long |
| Rejects | Operator entry, inspection station or sensor | Quality and first pass yield |
| Product or order | Operator selection or ERP | The right standard for each product |
| Shift and crew | Shift calendar | Fair comparisons between shifts |
Start with state and counts, because they are automatic and hard to argue with.
Add stop reasons next, using a short list, as our guide to downtime reason codes explains.
How production monitoring works in Fabrico
Fabrico is a light MES: production monitoring, downtime tracking and OEE from the same machine data. On the shop floor it runs in four steps.
- Connect. Each machine connects in the way that suits it: through its PLC, through a Fabrico IoT device with external sensors on older machines, or through AI cameras (an add-on) that count output where there is no signal. Where no sensor counts them, operators add stop reasons, good parts and scrap on a tablet or phone.
- Capture. Stops on connected machines are recorded with their start time and duration. When a line stops, a "line is down" card appears with the running counter and four actions: start a changeover, add a stoppage reason, add production or open a task. The reason takes two taps: the machine, then the reason, red for unplanned and amber for planned.
- See. The overview shows a card per line with its status, OEE, availability, performance and quality, and produced against remaining. The production line screen splits the shift into hourly rows of actual against target, with stops coloured by type. A TV status screen puts the same picture on the shop floor, readable from metres away.
- Improve. OEE analytics rank the top unplanned and planned stop reasons by line, shift, day or week, so the daily meeting starts with the biggest loss instead of collecting numbers. Stop reasons come from operators. AI cameras (an add-on) count parts; suggesting a stop reason is planned, on the roadmap. See what AI adds in AI production monitoring.
Installing the devices and connecting the machines takes about one month. Full rollout across the lines you choose takes 3 to 4 months. Book a demo to see it on a demonstration plant with lines like yours, or contact us with your machine list.
Who uses production monitoring software
- Operators see output against the shift target and tag stops as they happen, not at the end of the shift.
- Shift leads and supervisors see which line is standing still right now and walk there during the stop.
- Plant and production managers compare lines and shifts on OEE and stop reasons, and run the morning meeting from the numbers.
- Continuous improvement engineers get downtime by cause, machine and shift as input to their own root cause and SMED work on changeovers.
- Maintenance sees which breakdowns cost the most line time; in Fabrico a work order is opened from the stop in one step, linked to the line.
Manual tracking vs production monitoring software
| Paper or spreadsheet | Production monitoring software | |
|---|---|---|
| When you see a loss | After the shift, or the next day | While it is happening |
| Short stops | Rarely written down | Captured from machine data |
| Accuracy of durations | Rounded, often from memory | Timestamped events |
| Effort for operators | Writing and adding up | Picking a stop reason |
| Cost to start | Very low | Software, and sensors for machines without a usable signal |
Manual tracking is a good way to start the habit. It stops being enough once you need to find the losses nobody writes down.
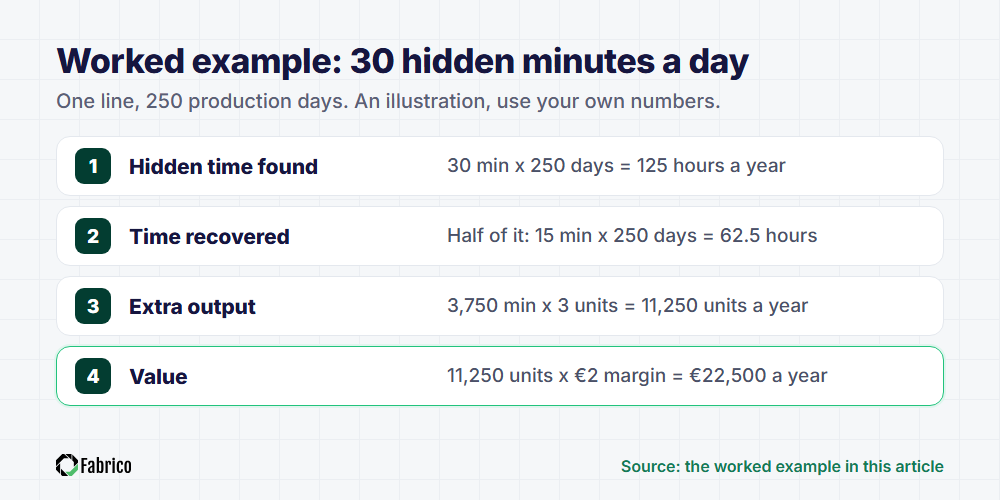
Worked example: the business case for one line
Here is a simple way to size the value before you buy anything. The numbers are an illustration, so replace them with your own.
| Item | Value |
|---|---|
| Line speed at the ideal cycle time | 3 units per minute |
| Short stops found by automatic tracking, not in the paper log | 30 minutes per day |
| Share you expect to remove in the first year | Half, so 15 minutes per day |
| Production days per year | 250 |
| Contribution margin per extra unit sold | €2 |
- Hidden time found: 30 × 250 = 7,500 minutes, or 125 hours a year.
- Time recovered: 15 × 250 = 3,750 minutes, or 62.5 hours a year.
- Extra output: 3,750 × 3 = 11,250 units a year.
- Value: 11,250 × €2 = €22,500 a year, if you can sell the extra units.
If the plant cannot sell more, value the recovered time as avoided overtime or a shift you no longer need. Then compare the result with the full cost of the system, including sensors and the time your team spends on it.
Production monitoring approaches compared
| Approach | Where the data comes from | Stop reasons | Best for |
|---|---|---|---|
| Paper sheets and whiteboards | Operators write counts and stops by hand | Long stops only, often written after the fact | A first look at one line |
| Spreadsheets | Manual entry after the shift | Whatever someone remembers | A few lines and a patient analyst |
| Standalone machine monitoring | Machine signal or sensor | Run and stop states, reasons often missing | Seeing utilisation per machine |
| Light MES (Fabrico's approach) | PLC or retrofit sensor, AI cameras (an add-on) for counts, plus operator input | Stops on connected machines, with a reason tagged on the line | Live OEE and downtime by cause without a full MES project |
| Full MES suite | Machines plus ERP, routings and genealogy | Yes, inside a wider system | Plants that also need dispatching, genealogy and batch records |
6 real-time production monitoring and intelligence tools at a glance, plus Fabrico
We picked tools that sell real-time production monitoring or production intelligence on their own websites, checked on 17 September 2026.
Fabrico is listed first because it is our product. The other six are listed in alphabetical order, not ranked.
Sources: each vendor's public website, checked on 17 September 2026. Product names are trademarks of their owners.
Features change often, so confirm details with each vendor.
| Tool | Data and maintenance, per the vendor |
|---|---|
| Fabrico | Data: PLCs, IoT sensors and AI cameras (an add-on) Maintenance: Built in |
| Guidewheel | Data: Clip-on sensors that read a machine's electrical signature, plus operator input at the line Maintenance: Maintenance requests from the floor, and actions triggered through your CMMS |
| L2L | Data: PLCs, SCADA, IIoT devices and operator entry Maintenance: Its own CMMS |
| Mingo Smart Factory | Data: PLC hardware, retrofit sensors and operator entry Maintenance: CMMS integrations, naming Fiix and UpKeep |
| Shoplogix | Data: Machine signals, PLCs, sensors and OPC, plus operator reason entry Maintenance: Its own Maintenance (CMMS) module |
| Sight Machine | Data: Controls, historians, MES and ERP Maintenance: Predictive maintenance recommendations |
| Worximity | Data: Sensors, PLCs and APIs, plus operator input Maintenance: CMMS integration through APIs, plus maintenance forms |
One note: we sell Fabrico, so it is not ranked
Disclosure: Fabrico is our product.
What it is: a light MES and OEE platform for seeing line losses during the shift, with maintenance built in as a complement.
How it tracks production
- Connects to machines through PLCs, IoT sensors and AI cameras (an add-on), so machines without a usable control signal can be tracked too. Supported protocols: OPC UA, Modbus, PROFIBUS, PROFINET, MQTT, EtherNet/IP, EtherCAT, IO-Link and HTTP.
- Calculates OEE in real time, with availability, performance and quality for each connected machine.
- Detects micro stops and shows downtime, MTTR and MTBF by machine, with Excel export.
- Sends push, in-app and email notifications based on rules you configure.
- Offers an AI assistant (an add-on) and multi-plant views with cross-plant benchmarking.
- Connects to your own tools through a REST API and webhooks. A connection to SAP or another ERP can be scoped per customer.
Maintenance
Your team can open work orders, run recurring preventive maintenance, manage spare parts and use approval workflows in the same platform.
Technicians use the iOS and Android apps and scan QR codes on machines. Fabrico is certified to ISO 27001, ISO 9001 and ISO 20000-1 and EU clients are hosted on AWS in Frankfurt.
Things to consider
- Production scheduling is on Fabrico's roadmap, not in the product today. Plan scheduling in your ERP or a dedicated tool.
- Machines without a usable signal need a Fabrico IoT device with external sensors or AI cameras (an add-on) first. Include that in your rollout plan.
- As a light MES, Fabrico leaves genealogy, routings and bills of materials in your ERP.
- Fabrico is cloud software, so it needs a working connection at the line; ask us before the pilot how a lost connection is handled at your plant.
- There is no formal root cause workflow. Stop reasons come from operators, and your team does the analysis. Suggested stop reasons are planned, on the roadmap.
1. Guidewheel
What it is: Guidewheel calls its platform FactoryOps and says it "gives your team machine intelligence, real-time visibility, and the AI-ready data layer that drives profitability."
How it tracks production
- Guidewheel says its sensor "clips around a machine's power conductor and reads its electrical heartbeat, so you see run, idle and down in real time."
- According to Guidewheel, this means "there is no need for PLC access or control-system changes."
- Guidewheel says operators or supervisors "tag the reason in a few taps, on a stop the sensor has already recorded".
- Guidewheel lists real-time OEE by machine and by plant, cycle and cycle time tracking, planned vs actual production, and mobile alerts.
Maintenance and integrations
- Guidewheel describes maintenance requests from the floor, and its site lists "Trigger maintenance actions through your CMMS" as an option.
- It says it integrates natively with SAP and connects to ERPs such as Oracle, Epicor and Microsoft Dynamics, plus CMMS, MES and BI tools, through Workato and an open API.
Things to consider
- Guidewheel says its sensors reach the cloud "over ethernet, WiFi or LTE, depending on what the site already has". Ask your IT team which option fits your plant.
- Guidewheel names executive leaders, maintenance teams and continuous improvement among the roles it serves. Agree who owns the pilot on your side.
2. L2L
What it is: L2L describes itself as a Connected Manufacturing Operations Platform that combines "operational data and AI to drive real-time action on the shop floor".
How it tracks production
- L2L says it captures data through "manual inputs from operators via the Operator Portal or Console, automated machine signals, and direct integration with existing systems like ERP and MES."
- It describes connections to PLCs, SCADA systems and IIoT devices to automate OEE calculations and downtime tracking.
- L2L lists real-time OEE tracking, digital production boards and live run rates across lines and sites.
- According to L2L, you can start tracking with operator entry before a full connectivity rollout is complete.
Maintenance and other modules
- L2L describes its own CMMS, with preventive maintenance based on time intervals or usage cycles and QR code access to equipment history.
- L2L also lists scheduling, digital work instructions and in-platform AI guidance it calls Execution AI.
Things to consider
- L2L says its platform covers downtime tracking, maintenance, production goals and frontline skills. Agree which modules your first phase needs.
- L2L says it connects with ERP systems like Oracle and SAP. Confirm the connection for the ERP you run.
3. Mingo Smart Factory (now part of Nulogy)
What it is: Mingo describes itself as "a manufacturing productivity and analytics platform that provides visibility into the data from machines, devices, and people and puts it all into context." Its site says Mingo is now a Nulogy company.
How it tracks production
- Mingo lists three ways to connect: hardware for existing controllers or PLCs, sensors or wireless nodes to retrofit machines, and, in areas with no machines, operator entry on PCs or tablets.
- Mingo says its IoT Edge Platform connects machines to the cloud and stores data if the internet connection goes down.
- Mingo lists real-time tracking of availability, performance, quality and downtime, plus scoreboards, operator screens and automatic shift reports.
- Mingo says its mobile app for iOS and Android shows downtime alerts, OEE, cycle times and target vs actual counts.
Maintenance and integrations
- Mingo describes integrations with CMMS systems, naming Fiix and UpKeep, and says work order requests can be triggered "directly from Mingo."
- It offers a managed integration service that, in its words, "connects with most ERP systems", plus an open API.
Things to consider
- Mingo says it runs its software "in a dedicated public cloud (AWS) environment". Share that with your IT team early.
- Mingo's industry list includes food and beverage, plastic packaging, metal stamping and injection molding. Ask for an example from a process like yours.
4. Shoplogix
What it is: Shoplogix describes a cloud-based platform "that provides manufacturers with real-time data presented in user-friendly visual dashboards". It says it is part of the Constellation Software family.
How it tracks production
- Shoplogix says its OneSignal approach turns "part count signals into meaningful production insights for your operation teams."
- It says it can use data from PLCs, sensors or OPC protocols, and that it works with any machine "regardless of age or communication protocol".
- Shoplogix says operators pick downtime and scrap reasons from a dropdown list, and it lists hour-by-hour OEE in real time.
- Shoplogix describes a Digital Andon for real-time alerts and escalation, and an AI assistant called Pulse AI.
Maintenance
- Shoplogix describes a Maintenance module with "core CMMS capabilities such as creating, assigning, and scheduling work orders, tracking maintenance history, and logging repair tasks."
- It says preventive maintenance can be scheduled on real usage, based on production throughput and run speeds.
Things to consider
- Shoplogix lists several modules and add-on sensors. Agree which ones your pilot needs.
- Shoplogix says it integrates with common ERP and MES solutions. Confirm the connection for the systems you run.
5. Sight Machine
What it is: Sight Machine presents itself as an agentic manufacturing platform, which it launched in June 2026. Its homepage describes "Agent-powered manufacturing that continuously finds more output, eliminates more waste, and improves with every run".
How it tracks production
- Sight Machine says it connects to plant systems such as "controls, historians, MES, ERP, and document repositories".
- It says its platform turns raw signals into production events and KPIs, and that agents watch fault signals, event counts and timing patterns.
- According to Sight Machine, findings arrive as recommendations in tools such as Microsoft Teams, Microsoft Excel or a kiosk on the floor.
Maintenance
- Sight Machine describes agents that monitor signals such as spindle load, vibration and tool wear to surface predictive maintenance recommendations.
Things to consider
- Sight Machine says its manufacturing intelligence "flows across the enterprise stack, linking production to supply chain, logistics, and demand". Agree which of those areas your first phase covers.
- Sight Machine says each deployment is "single-tenant by design, with its own database, namespace, and keys". Your IT team will want that detail for its review.
6. Worximity
What it is: Worximity sells "OEE and real-time production monitoring that boosts efficiency, improves profitability and empowers your manufacturing workforce", together with continuous improvement coaching.
How it tracks production
- Worximity says sensors collect line counts or events and send them to its IoT device, and that data can also come from newer equipment through PLCs.
- Its FAQ says the connection device needs power and a machine signal from a PLC, an API or a photoelectric sensor.
- Worximity lists real-time OEE, line status, shop floor displays, alerts when lines are down and regular performance reports.
- Worximity says operators can justify unplanned downtime in a few clicks, and that Worximity Forms works on phones, tablets and PCs.
Maintenance and integrations
- Worximity says push and pull APIs exchange data with back-office systems "like an ERP, MES and CMMS."
- Its Forms module lists uses such as "Preventive maintenance checklists, calibration logs, parts requests".
Things to consider
- Worximity says it connects to BI platforms "like Power BI or Tableau". Ask which reports your team would build there.
- Worximity's industry list includes food and beverage, packaging and co-manufacturing, CPG and machining. Ask to see a reference from a similar line.
Questions to ask in every demo
- How do you connect to our oldest machine, the one without a usable PLC signal?
- Can you show the raw stop events for one shift, with start and end times?
- What is the shortest stop your system records on our type of machine?
- How does an operator enter a stop reason, and how long does it take?
- Who is notified about a long stop, and through which channel?
- Who turns a long stop into maintenance work, and in which system is that work tracked?
- Which ERP and other systems do you connect to, and is there an API?
- Where is our data hosted, and which security certifications do you hold?
- What does a pilot include, and what do we need to prepare?
- Can we export our data if we leave?
A pilot scorecard
Pick your bottleneck machine, agree on the criteria below before the pilot starts, and score the tool at the end.
| Criterion | Pass when |
|---|---|
| Count accuracy | The system's count matches a manual count over a full shift |
| Stop capture | Short stops you trigger on purpose appear as separate events |
| Reason coverage | Most stop minutes above your threshold have a reason by the end of each shift |
| Adoption | Operators enter reasons without daily reminders |
| Action | The team has fixed at least one loss it found in the data |
| Trust | The supervisor uses the dashboard in the daily meeting instead of the paper log |
Testing on your hardest machine shows a tool's limits early. Our daily OEE meeting guide shows how to use the data once it is trusted.
Next steps
If short stops and downtime are your biggest losses, start with our guides on micro stops and how to reduce machine downtime. To compare tools built for downtime first, see our downtime tracking software review.
For six more tools, see our production monitoring systems comparison.
To see how Fabrico tracks OEE and downtime in real time, book a demo.
Frequently asked questions
What is the difference between production tracking and production monitoring?
Production tracking often focuses on orders, jobs and operator input. Production monitoring focuses on machine data collected automatically.
Many tools cover both, so check what each one captures on your machines.
What does real-time production monitoring mean?
It means machine state and counts update while the shift can still react, stops are recorded with a start and end time, and the right people see it during the shift.
Can production monitoring software work with old machines?
Often, yes. Machines without a usable control signal can be connected with sensors or cameras, depending on the tool.
Ask each vendor to show the method on your oldest machine.
How long does a production monitoring pilot take?
Plan a pilot on one machine, counted from the day it reports data. Use it to check the counts, capture the stops, build the habit of entering reasons and fix a first loss.
Connecting the machine comes first, so ask each vendor for that date separately. With Fabrico, plan for two steps. Installing the devices and connecting the machines takes about one month. Full rollout across the lines you choose takes 3 to 4 months.
What is real-time production tracking software?
It is production tracking software that records output, stops and job progress as they happen, from machine signals and operator input.
Use the five tests in this guide to check whether a tool's tracking is truly real time.
Is production monitoring software the same as OEE monitoring software?
Mostly. Production monitoring software tracks machine state, counts and stops; OEE monitoring software turns the same data into availability, performance and quality by line and shift. Most tools in this guide do both.
Fabrico calculates OEE in real time from the same machine data it uses for monitoring. The OEE formula shows how the three factors combine.
How much does production monitoring software cost?
It depends on the number of machines, the hardware each one needs and the modules you choose. Vendors price by machine, by site or by number of users, and sensors or cameras can add to the cost.
Ask each vendor to quote the same scope. For Fabrico: Quoted per plant. Start with a one-line pilot.
What should production monitoring software connect to?
At least your ERP, so products and orders match what the machines report, and an API or data export for your own reports.
Fabrico has a REST API, webhooks and Excel or CSV export, and a connection to SAP PM or SAP S/4HANA can be scoped per customer with your SAP team.
See where lines like yours lose time, with live OEE and downtime by cause.
Book a demoContact usRelated articles










Real Fabrico tiles, sample data.