


 Login
 Blog
Equipment Commissioning Checklist: Stages, Sign-Offs and Pass Marks

In short: An equipment commissioning checklist takes a new machine or line from mechanical completion to a signed handover through five gated stages: mechanical completion, pre-commissioning, cold commissioning, wet commissioning and a performance run. Each check names who signs, the evidence and the pass mark, and the last gate is a measured OEE baseline run.
- Close each stage with a signature, evidence on file and a pass mark agreed before the work starts.
- Run the handover test with the plant crew for three shifts in a row, measured from the machine signal or a counting camera.
- Do not sign until the count is checked, the machine states are logged and stop reasons are in use.
- A failure-mode table prices the commissioning misses that cost money after handover.
A new flow wrapper, case packer or full packaging line is bolted down, wired and piped. The builder passed its tests, the integrator wants a signature and sales has a launch date. This checklist covers the weeks in between: what to check at each stage, who signs, what goes in the file, and the pass mark that closes the gate.
The factory acceptance test (FAT) at the builder's works and the site acceptance test (SAT) are the stages before commissioning; the acceptance test guide sets out what each one covers. The weeks after handover are a separate plan: the new line ramp-up plan. Machine safety and legal duties are signed off by the plant's own safety and legal owners; this page is not legal advice.
Equipment commissioning checklist: the stages and their gates
The International Electrotechnical Commission's commissioning standard for process plants, IEC 62337, frames the job well. Its summary says it describes activities following the "completion-of-erection" milestone of the project and prior to the "acceptance-of-the-plant" phase by the owner, and that those activities need adapting to each plant. A packaging line is not a process plant, but the shape holds: commissioning starts when the installers say they are done and ends when the owner accepts.
For a food or FMCG packaging machine, five gates do the work: mechanical completion (installed to the drawings, with no A items, the faults that block safe power-on, on the punch list), pre-commissioning with the power off, cold commissioning powered but without product, wet commissioning with product and packaging material, and a performance run by the plant's own crew that ends in handover.
Decide in the commissioning plan who leads each stage, integrator or plant, and where the lead passes from one to the other. A stage nobody owns is a stage nobody closes.
The handover gate is the easiest one to let slide. "It ran well on Thursday" is an opinion. A measured run is not: OEE software reading the machine's own signal, or a camera that counts output where there is no clean signal, records availability, performance and quality per shift, with stops timed and given a reason at the line. The same screen then follows the line after handover, so the first weeks of output are judged on the same rules as the run.
What you see: a shift timeline, unclassified time waiting for a reason, and the operator's line-down screen, on sample lines. Book a demo.
Plays from YouTube. Google may set cookies when you press play. Privacy policy.
The safety and legal layer, before first power-on
In the EU, the machine arrives with duties already met by its maker. The Machinery Directive 2006/42/EC, Article 5, says that before placing machinery on the market and/or putting it into service, the manufacturer or an authorised representative must, among other things, draw up the EC declaration of conformity and affix the CE marking. Check both are in the file, with instructions in the plant's language, before anyone powers the machine. Where a line joins machines from several makers, ask who declares the line as a whole.
The rules are changing. The new Machinery Regulation (EU) 2023/1230 replaces the Directive. The European Commission notes that a corrigendum fixed its application dates, and that machinery placed on the EU market before 20 January 2027 must comply with Directive 2006/42/EC. A line ordered now may be put into service either side of that date, so ask the builder which law the machine was built and declared to.
Risk assessment has its own standard. ISO 12100 specifies principles of risk assessment and risk reduction for the design of machinery; ask for the builder's assessment, and add the hazards your layout creates, such as a new walkway or an operator reaching into a buffer.
The plant also has duties as the user. In Great Britain, HSE guidance says that where safety depends on how equipment is installed, it should be inspected after installation and before first use. In the US, OSHA's lockout standard, 29 CFR 1910.147, requires an energy control program of procedures, training and periodic inspections before anyone services a machine that could start up unexpectedly. Commissioning has plenty of that work: guards come off, settings change, and two teams work on one machine. OSHA's overview is blunt that the unexpected startup or release of stored energy can result in serious injury or death. Write the isolation procedure for each energy source on the new machine before cold commissioning, not after the first incident. More on the practice: lockout tagout.
The checklist with pass marks, stage by stage
Three tables cover the first four stages; the fifth, the handover, has its own section below. Each row is a check, the person who signs it, the evidence that goes in the file and the pass mark that closes it. Agree the pass marks in the commissioning plan before the integrator arrives; a pass mark written on the day of the test tends to match whatever the line just did. Change the names to the roles your plant uses, but keep one name per row.
Stages 1 and 2: mechanical completion and pre-commissioning
| Check | Who signs | Evidence | Pass mark |
|---|---|---|---|
| Mechanical completion walkdown against the drawings | Project engineer, integrator lead | Signed completion record, punch list | No A items open |
| Electrical and pneumatic install: earthing, insulation tests, air pressure | Electrical engineer | Test sheets per circuit | All circuits tested, within the builder's limits |
| Safety file: CE marking, declaration, instructions, risk assessment | Plant safety owner | Copies in the project file | Complete before first power-on |
| Isolation points and a lockout procedure per energy source | Plant safety owner | Written procedure, labelled isolators | Every source has a tested procedure |
| Product-contact parts and cleaning plan | QA or hygiene lead | Material declarations, cleaning method | All contact parts covered |
Stage 3: cold commissioning
| Check | Who signs | Evidence | Pass mark |
|---|---|---|---|
| I/O check: every sensor and actuator | Integrator controls engineer | Ticked I/O list | 100% of points checked |
| Safety functions: e-stops, guard interlocks, light curtains | Plant safety owner | Function test record | Each one stops the machine as designed |
| Dry cycles at 50%, 75% and 100% of rated speed | Integrator lead | Speed log with times | Each step runs clean for the agreed time |
| Machine states and counts reach plant systems | Plant automation or IT/OT lead | Signal list with timestamps | Each state seen once and matches the HMI |
| Format parameters loaded for every format | Integrator controls engineer | Recipe list per format | All formats in the contract loaded |
The signal row is easy to leave until later. If the machine follows PackML, the OPC Foundation's PackML specification names standard machine states and Overall Equipment Effectiveness (OEE) data as things PackML provides. Ask the integrator to show each state arriving in your systems during cold commissioning, while changes are still cheap. The detail is in the PackML state model guide, and what a machine screen can and cannot give you is in HMI data collection for OEE.
Stage 4: wet commissioning
| Check | Who signs | Evidence | Pass mark |
|---|---|---|---|
| First runs per format with film and cartons from normal suppliers | Production manager | Run log per format | One clean hour at rated speed per format |
| Count at the constraint against a hand count | CI or production engineer | Hand tally sheet, counter reading | Within 1% over one hour |
| Rejects reach the bin and the reject count | QA lead | Bin count against the reject counter | Counts match |
| Changeover per format against its standard | Production manager | Timed changeover sheet | Two in a row within the standard |
| Cleaning or washdown cycle | QA or hygiene lead | Cleaning validation record | QA signs it off |
| Stop reason list on the operator screen, crews trained | Production manager | Reason list, training record per shift | Every shift trained before the performance run |
Two rows decide whether the handover data can be trusted: the hand count proves the counter, and the reason list decides whether the run's stops can be split between builder and plant. Keep that list short, with builder and plant items apart; downtime reason code design covers how.
The handover test: a measured OEE baseline run
The performance run turns "it works" into a number both sides sign. The formula need not be invented: a NIST report on manufacturing standards notes that ISO Standard 22400 presents commonly-accepted OEE calculations, including the timing calculations. Use it for the run, with one formula written into the plan: OEE is availability times performance times quality, with losses counted once at the constraint, as in the OEE calculation guide.
Eight pass marks close the gate. Do not sign while any is open:
- Run length: 3 shifts in a row, nights and a changeover.
- Crew: Plant operators run it; integrator only advises.
- Count: Counter within 1% of a one-hour hand count.
- States: Running, stopped, starved, blocked, faulted logged.
- Reasons: Reason list live; unclassified 10% or less.
- OEE baseline: A, P and Q at or above the plan's marks.
- Punch list: No A items; B items dated, with an owner.
- Dossier: Drawings, PLC backup, spares, training records.
If the line has a contract performance figure, the test conditions for it belong in the contract, not here; see the OEE clause in a new line contract. The baseline run is the plant's own measurement, and it becomes week 0 of production. How to set a baseline that holds is covered in OEE baseline measurement.
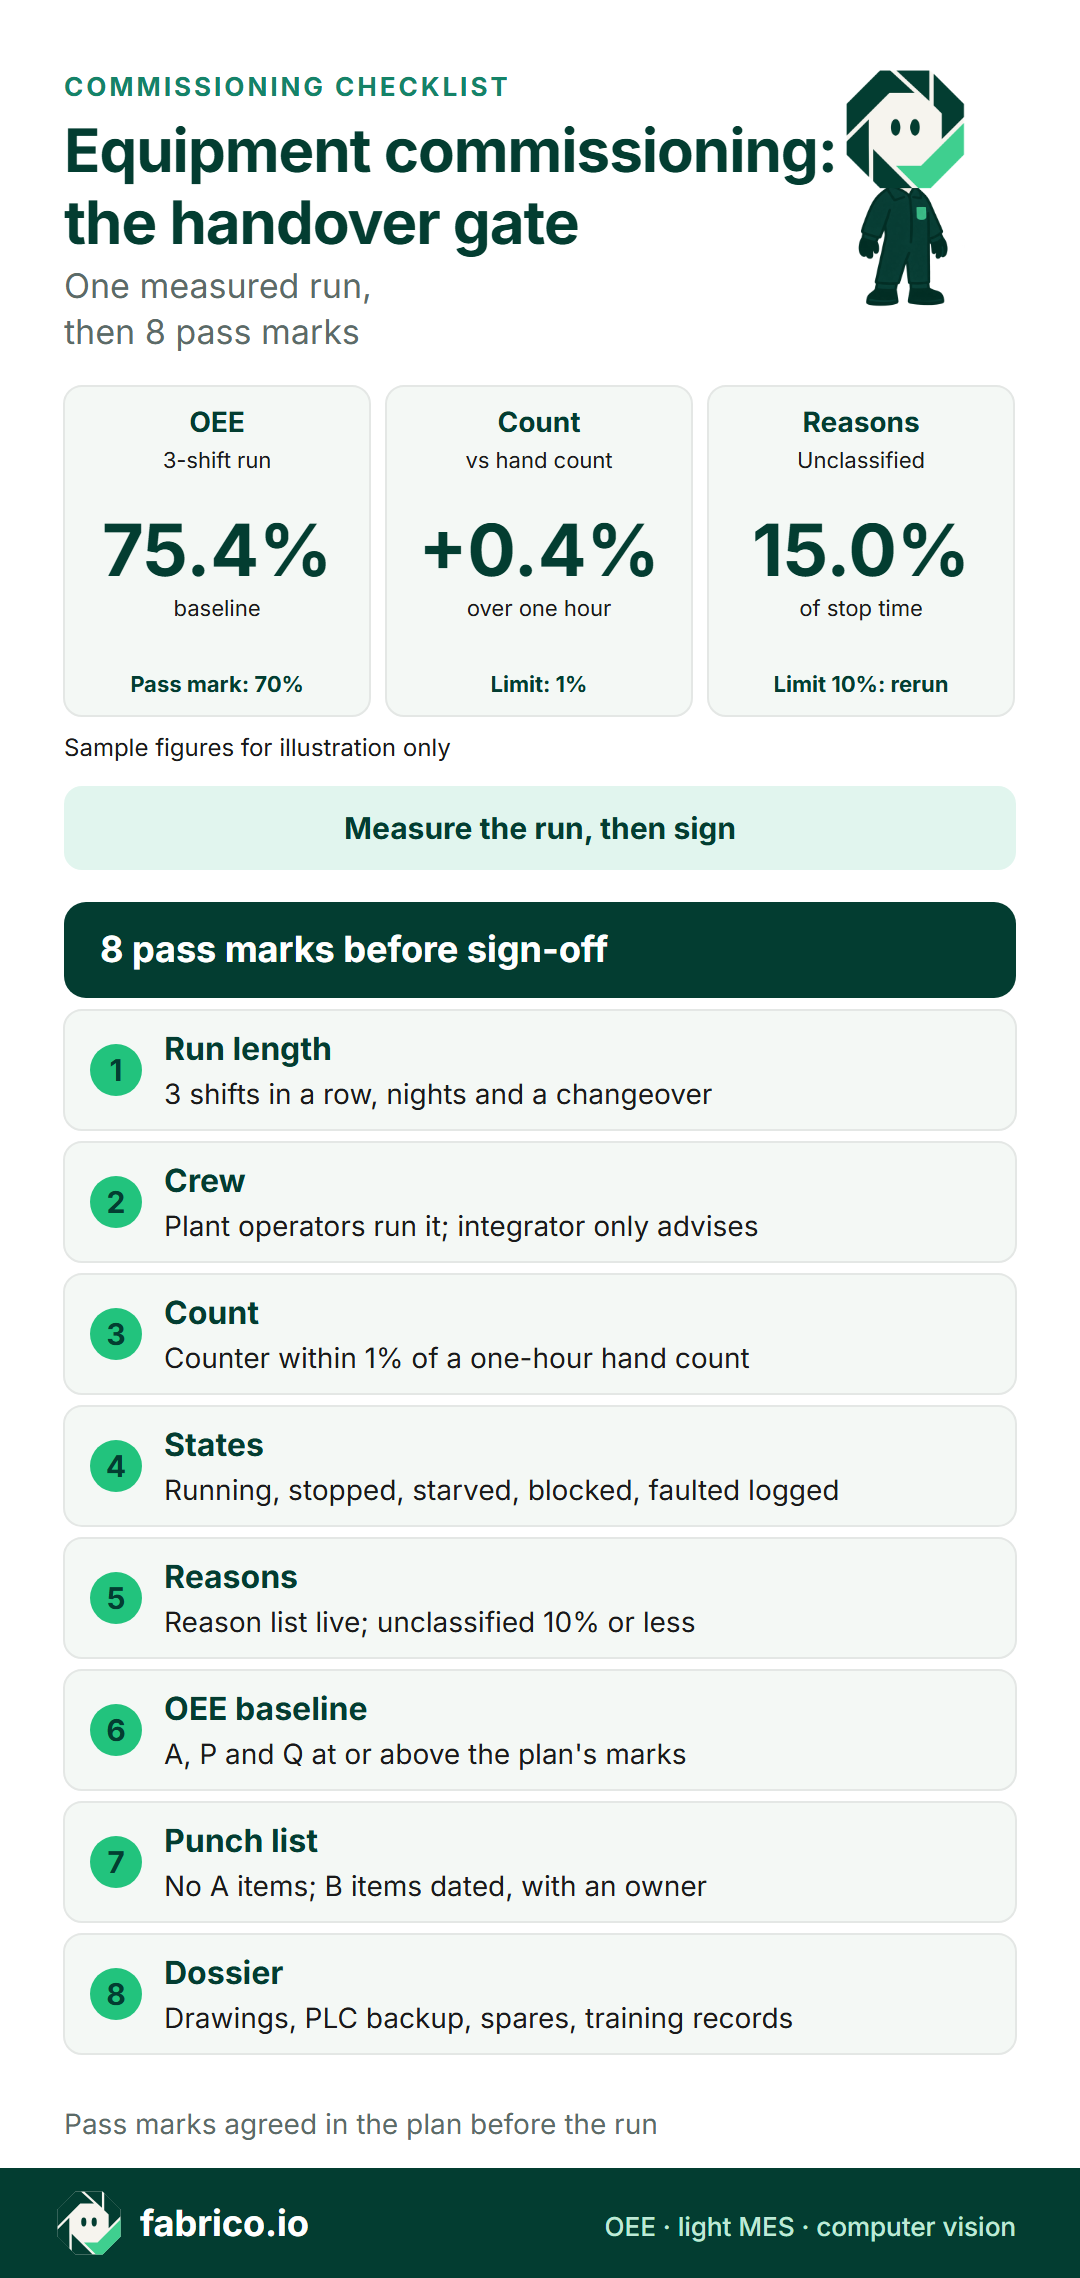
Text version of this infographic
- Title: Equipment commissioning: the handover gate. One measured run, then 8 pass marks.
- OEE: 75.4% baseline over a 3-shift run (87.0% availability, 88.0% performance, 98.5% quality). Pass mark: 70%.
- Count: +0.4% against a hand count over one hour. Limit: 1%.
- Reasons: 15.0% of stop time unclassified. Limit 10%, so one shift is rerun.
- Sample figures for illustration only.
- Measure the run, then sign.
- 8 pass marks before sign-off:
- 1. Run length: 3 shifts in a row, nights and a changeover.
- 2. Crew: Plant operators run it; integrator only advises.
- 3. Count: Counter within 1% of a one-hour hand count.
- 4. States: Running, stopped, starved, blocked, faulted logged.
- 5. Reasons: Reason list live; unclassified 10% or less.
- 6. OEE baseline: A, P and Q at or above the plan's marks.
- 7. Punch list: No A items; B items dated, with an owner.
- 8. Dossier: Drawings, PLC backup, spares, training records.
Worked example: the handover run on a biscuit flow-wrap line
Sample figures for illustration only. A biscuit plant commissions a new flow-wrap line. The flow wrapper is the constraint, rated at 150 packs a minute for the format tested. The plan sets the run at three shifts in a row of 480 minutes, so 1,440 planned minutes, with one changeover and the night shift included. The pass marks, written before the run: availability 85%, performance 85%, quality 98%, OEE 70% (85% x 85% x 98% = 70.8%, rounded down), unclassified stop time 10% or less of stop time, and the counter within 1% of a hand count.
What the run recorded:
- Stops: 187 minutes. Changeover 38, machine faults 96 (film splices and infeed jams), starved by the biscuit feed 25, and 28 with no reason.
- Availability: run time 1,440 minus 187 = 1,253 minutes. 1,253 / 1,440 = 87.0%.
- Performance: 165,400 packs counted against 1,253 x 150 = 187,950 possible. 165,400 / 187,950 = 88.0%.
- Quality: 2,480 rejects, so 162,920 good packs. 162,920 / 165,400 = 98.5%.
- OEE: 87.0% x 88.0% x 98.5% = 75.4%. Check: 162,920 good packs / (1,440 x 150 = 216,000) = 75.4%.
- Count check: over one hour, the counter read 8,445 and the hand count 8,412: +0.4%, inside the limit.
Four OEE marks pass. The reasons mark does not: 28 of 187 stop minutes, 15.0%, have no reason. So the line is not handed over yet. The integrator and the crew go through the 28 minutes with the shift notes, fix the reason list where it had no fitting entry, and rerun one shift.
In money. At a sample contribution of EUR 0.12 a pack, one minute of the wrapper standing costs 150 x EUR 0.12 = EUR 18, and an hour EUR 1,080. Against the 216,000 packs the run could have made, it lost 53,080: 28,050 to stops (187 x 150), 22,550 to slow running (187,950 minus 165,400) and 2,480 to rejects, each counted once. That is EUR 6,369.60 over three shifts. The 28 unclassified minutes alone are EUR 504 a run; over 15 shifts a week, if nothing changes, EUR 2,520 a week of loss that no one can assign to the builder or the plant.
If the counter had never been checked. Say it over-read by 3%. The true count would be about 160,583 packs, performance 160,583 / 187,950 = 85.4%, good packs 158,103 and OEE 158,103 / 216,000 = 73.2%. The run still passes 70%, but the baseline sits 2.2 points high, and every week after handover would chase a number the line never made. The 4,817 phantom packs are worth about EUR 578 a run and EUR 2,890 a week.
Commissioning misses that cost money after handover
Each miss below can pass a handover unnoticed and surface weeks later as lost output. Here are seven, with the first sign in the line data and a sample cost at EUR 18 a minute, the flow-wrap example's rate. Sample figures for illustration only.
| Commissioning miss | First sign in the line data | Sample cost | Close it before handover |
|---|---|---|---|
| No stop reason list at handover | 15% or more of stop time has no reason | EUR 2,520 a week of stops nobody can assign | Load the list and train each shift in wet commissioning |
| Counter never checked against a hand count | OEE reads high; packed output does not match the count | 3% over-read hides about EUR 2,890 a week | One-hour hand count, within 1% |
| Rated speed per format not written down | Performance swings when someone edits the rate | Rate set to 140 instead of 150: 12,530 packs of slow running hidden, EUR 1,504 per three shifts | Rated speed per format in the handover file |
| Changeover not timed before handover | Changeovers run 20 minutes over the standard | 5 a week: EUR 1,800 a week | Two timed changeovers per format |
| Critical spares not on site | One long stop waiting for a part | One 8-hour wait: EUR 8,640 | Spares list agreed and stocked before handover |
| Crews trained on the day shift only | Night shift stops run longer | 30 more minutes a night, 5 nights: EUR 2,700 a week | Train each shift; include nights in the run |
| Film tested from one supplier only | Jams when the second supplier's reel goes on | 135 extra stop minutes in one run: EUR 2,430 | Wet runs with every approved supplier's material |
Each fix costs an hour or a shift while the integrator is on site, and weeks once its engineers have gone home. Watch the speed row: if the rated speed per format is not on file, it can be edited down later, and slow running leaves the figures but not the line. Reduced speed vs minor stops explains how to tell them apart.
Book a demo to see stops, counts and reasons from a connected line laid out on one shift timeline, the view a handover run is read from.
Plan it this week, close it this quarter
For a plant, production or engineering manager with a machine arriving in the next few months:
- This week: write the five gates into the commissioning plan with one owner each, and name who leads which stage, integrator or plant.
- This week: set the performance run pass marks (run length, crew, OEE factors, unclassified limit, count tolerance) and send them to the integrator.
- This week: ask the builder for the declaration of conformity, instructions and risk assessment.
- This month: draft the stop reason list for the new machine, split into builder and plant items, and decide where the count and the machine states will come from.
- This month: agree the critical spares list and the training plan per shift, night shift included.
- This quarter: run the four stage tables, file the evidence, and hold the handover until all eight pass marks are met.
- This quarter: carry the baseline into week 1 of production unchanged, with the same formula, rated speed and reason list.
For a new site rather than a new line, maintenance software set-up runs alongside this work; see CMMS for a greenfield plant start-up as a further read.
Where Fabrico helps at the handover gate
Fabrico is OEE and light MES software. At commissioning, it supplies the measured side of the last gate:
- The baseline from the machine: Fabrico reads automated machines from the PLC and fits an IoT device with sensors where the PLC is hard to read, so the run is measured in availability, performance and quality per machine, line and shift.
- Stops with reasons: micro-stops are detected from the machine signal, and the operator picks the stop cause on a tablet or phone, so the unclassified share is visible during the run, not after it.
- A machine with no usable signal: the camera add-on counts output instead, and its video for a stop is streamed on request and not stored in Fabrico.
- Evidence for the file: downtime splits by cause, machine and shift, losses are shown in money, and lists export to Excel or CSV for the handover report.
More: the OEE and MES solution overview, light MES explained, the computer vision add-on, how to judge OEE software, OEE software for high-speed packaging lines and computer vision for food manufacturing. Flow wrapper losses in detail: flow wrapper OEE.
Questions engineers ask about commissioning
Where does commissioning start and end?
It starts at mechanical completion, when the installers say the machine is in place to the drawings, and ends when the plant signs the handover. In between, the installed machine is checked stage by stage, from power-off checks through dry and product runs to a performance run by the plant's own crew. The builder's acceptance tests come before it.
What is the difference between cold and wet commissioning?
Cold commissioning runs the machine powered but without product: I/O checks, safety functions and dry cycles at rising speed. Wet commissioning adds product, packaging material and, on food lines, water or cleaning fluids, so formats, counts, rejects and changeovers can be tested for real.
How long should the performance run before handover be?
At least three shifts in a row, with the night shift, one changeover and the formats that matter. If one shift misses a pass mark, fix the cause and rerun that shift; do not average it into the other two.
Who should sign the commissioning handover?
The production manager accepts the line for output, the engineering manager accepts the technical file and punch list, the plant's safety owner signs the safety checks, and the integrator's project lead signs for the supplier. Each signature sits next to the evidence it covers.
Do I need OEE software to commission a new packaging machine?
Not to commission it, but the handover test needs a measured baseline: availability, performance and quality taken from the machine signal, with stop reasons logged. A spreadsheet can do it on one run; software keeps the same rules through the weeks that follow.
Book a demo to see a measured run on one screen: availability, performance and quality by shift, with stops and their reasons.
Related articles
Latest from our blog


Real Fabrico tiles, sample data.