


 Login
 Blog
Flour Mill Software: ERP, Mill Control and OEE, Sorted

In short: flour mill software is a set of separate systems. A wheat mill runs mill control or SCADA for the rolls, sifters and bins, lab records for ash, moisture and protein, blend and treatment control, a flour mill ERP for wheat, lots, orders and invoices, a warehouse and dispatch system for bags and tankers, and an OEE and light MES layer on the packers. The right first purchase depends on whether you are missing records or missing hours.
- The ERP is the business record: contracts, lots, stock and costs. It does not see the packer stop.
- Most of the mill, from cleaning to the plansifters, already runs under its own control system.
- Bagging lines for 1 to 50 kg sacks are where Fabrico measures OEE, plus run and stop time on machines with a signal.
A flour mill is a long chain of machines with very few people. Wheat arrives by truck or rail, is cleaned and tempered, then passes through break and reduction roller mills, plansifters and purifiers, often for hours with nobody touching it. The flour streams are blended, treated, and then packed into bags or blown into bulk tankers.
Some vendors of flour mill software or flour mill ERP software promise all of it. A mill buys several products instead, and the real choice is the order in which to fix them.
Fabrico covers one of them: measuring OEE, with a light MES, on the packing and bagging lines. This page maps the other systems and works one packer shift through to money.
Flour mill software, system by system
Each system in a flour mill answers one question. The control system asks whether the flow is right. The lab asks whether the flour is right. Finance reads the ERP for money and stock. Operations needs the line layer to see why the packer was idle.
| System | Its job in a flour mill | Owner |
|---|---|---|
| Mill control or SCADA | Runs intake, cleaning, tempering, roller mills, sifters, conveyors and bins, with alarms and interlocks | Head miller, automation |
| Intake and weighbridge | Truck weights, wheat samples, bin allocation | Intake, QA |
| Mill lab records | Ash, moisture, protein and other flour tests, extraction rate per run | QA lab |
| Blend and treatment control | Flour stream blending, enrichment and improver feeder rates | Head miller, QA |
| Flour mill ERP | Wheat contracts, lots, stock, orders, invoices, costing | Finance, sales |
| WMS and dispatch | Bag stock, bulk bins, tanker loading, delivery notes | Logistics |
| OEE and light MES | Run time, stops and counts at the packers, palletiser and machines with a signal | Operations, CI |
The last row is the one that measures the line. It records when each packer runs and stops, how many bags it counts, and the reasons the crew gives for its stops, per machine and per shift. Availability, performance and quality come out of those three records, and so does the money lost on the shift.
What you see: a shift timeline, unclassified time waiting for a reason, and the operator's line-down screen, on sample lines rather than a flour mill. Book a demo.
Plays from YouTube. Google may set cookies when you press play. Privacy policy.
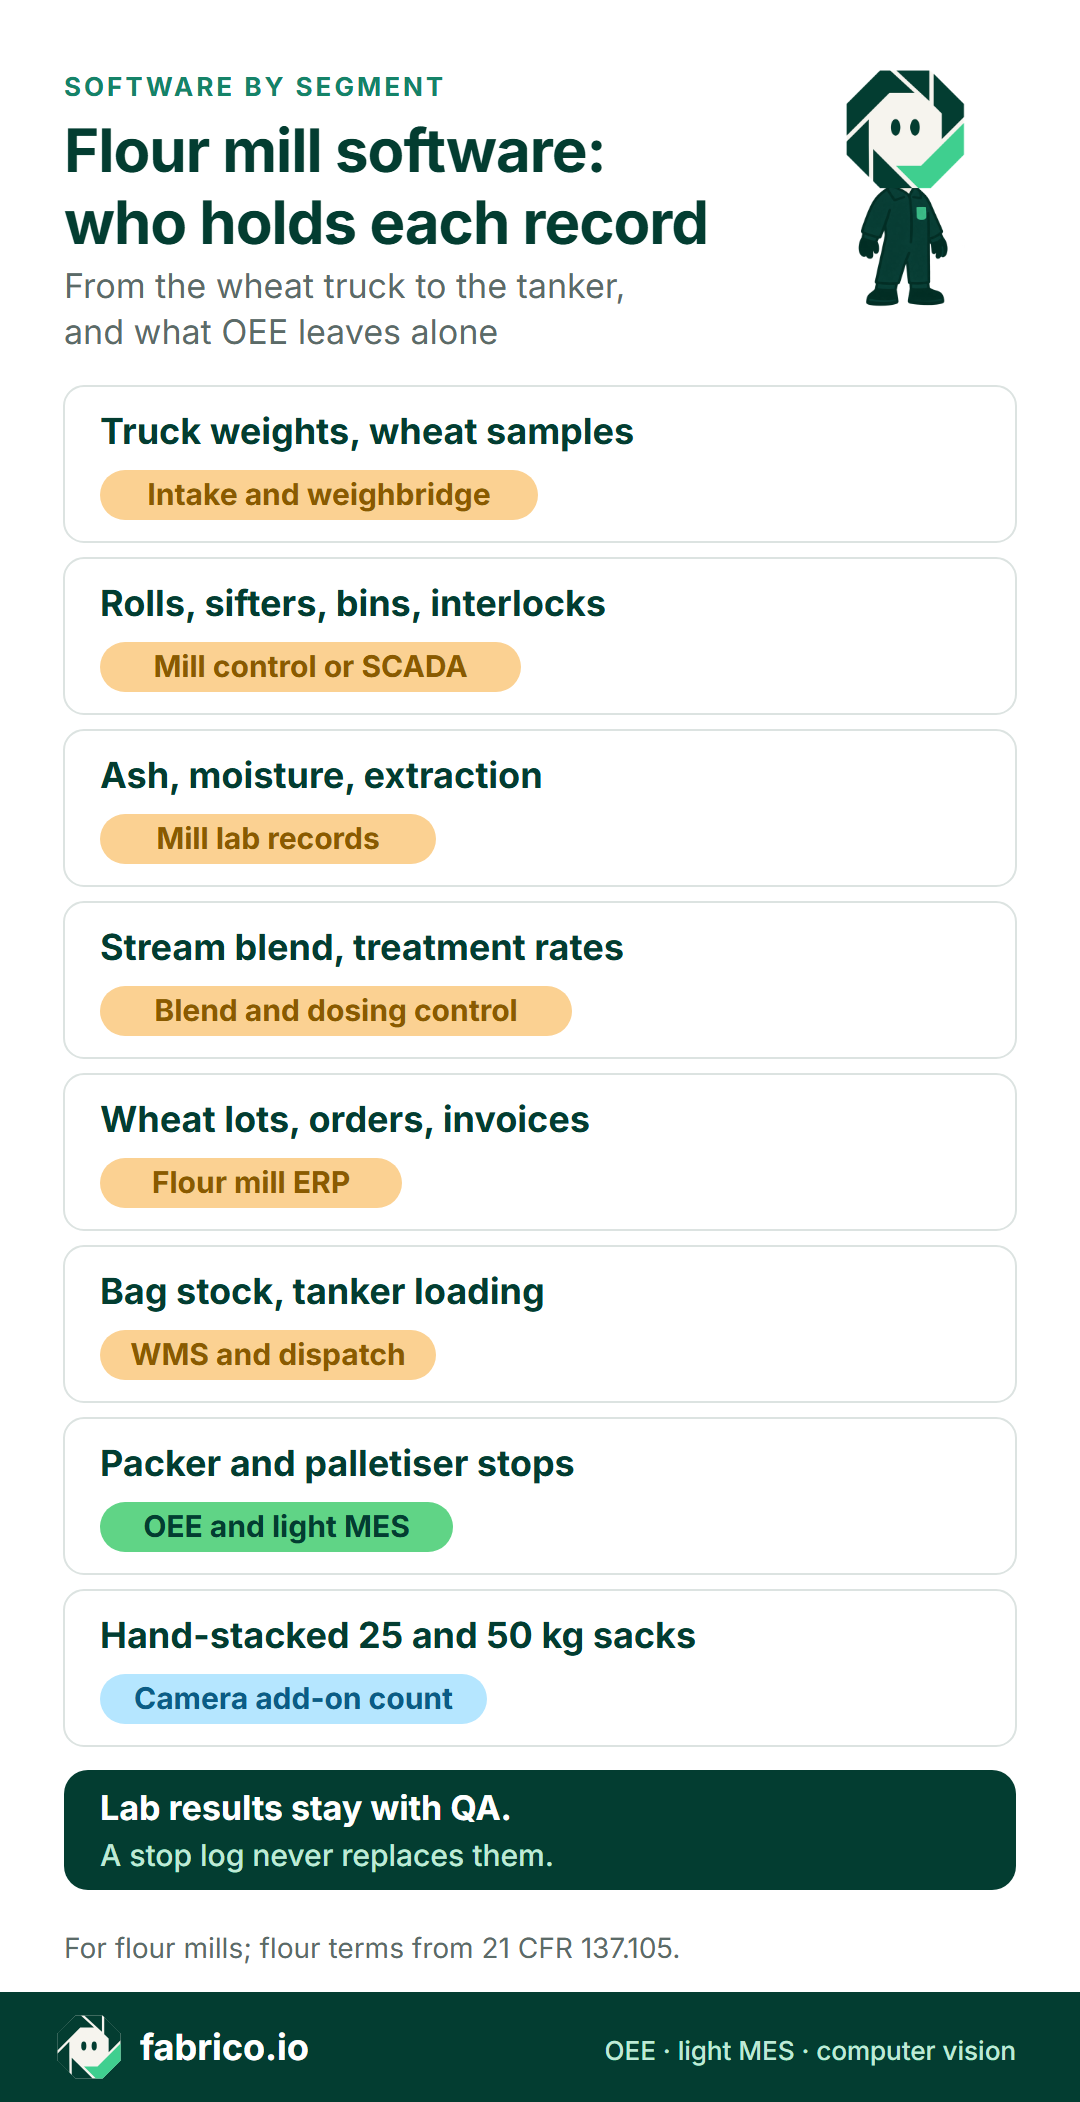
Text version of this infographic
- Truck weights and wheat samples: intake and weighbridge software.
- Rolls, sifters, bins and interlocks: mill control or SCADA.
- Ash, moisture, protein, extraction: mill lab records.
- Stream blend and treatment rates: blend and dosing control.
- Wheat lots, orders, invoices: flour mill ERP.
- Bag stock and tanker loading: WMS and dispatch.
- Packer and palletiser stops: OEE and light MES (where Fabrico works).
- Hand-stacked 25 and 50 kg sacks: camera add-on count.
- Lab results stay with QA; a stop log never replaces them.
Mill control and SCADA
The mill control system sets tempering water, runs the roller mills, plansifters and purifiers in sequence, moves stock between bins and trips the line on a choke. It usually comes with the mill equipment. A floor layer should read from it, never run it.
Lab records: extraction rate and ash
Whether the flour is right is a lab question. The lab tests moisture, ash and protein on wheat and on flour, and the extraction rate comes from wheat in against flour out over a run. These are QA records, with their own methods and sign-offs.
For scale, the USDA NASS Flour Milling Products report for July to September 2026 says all wheat ground for flour in the quarter was 227 million bushels, and total flour production was 105 million hundredweight. At 60 pounds a bushel, that is about 77 pounds of flour from every 100 pounds of wheat across US mills. The same report puts the daily 24-hour milling capacity of wheat flour at 1.63 million hundredweight. Our arithmetic from those figures: 105 million over 92 days of 1.63 million is about 70 percent of rated capacity, so US mills had headroom.
Blending and treatment
Bakery and household flours are blends of streams, and many are treated with enrichment, improvers or, where allowed, bleach, dosed by the mill control or a dosing system.
Flour mill ERP software: what it does, and what it does not
Flour mill ERP software is the business record of the mill. It holds wheat purchase contracts and intake tickets, flour products and specs, customer orders, lots, stock in bins and bags, invoices and costs. Some ERPs for milling add a grist calculator or a link to the lab. It is the right home for anything finance or sales must sign.
What an ERP does not do is watch the floor during the shift. It counts bags once the run is booked, but rarely shows that the 25 kg packer stood for 40 minutes because the flour bin ran empty. That is the job of an OEE layer reading machine signals during the run. Our page on ERP vs MES covers the general split.
| Question | Flour mill ERP | OEE and light MES |
|---|---|---|
| How much wheat did we buy and grind? | Yes, from contracts and intake | No |
| What did this lot cost? | Yes, from stock and costing | No |
| How many bags did we pack? | After the run, per product | During the run, per packer |
| Why did the packer stop at 03:10? | No | Yes, signal plus operator reason |
| What was the extraction rate? | From lab and stock figures | No, a lab record |
So the ERP and the floor layer do not compete. The ERP sends products, bag sizes and orders to the line, and gets run hours, stop minutes and bag counts back.
What the flour rules ask for, and which system keeps the proof
US and UK rules show why lab and dosing records are their own category; QA names the local rules.
- Ash and moisture. Under 21 CFR 137.105, flour is freed from bran coat, or bran coat and germ, until its ash, on a moisture-free basis, is not more than 1/20 of the percent of protein plus 0.35. The same section says its moisture content is not more than 15 percent. Both are lab results.
- Enrichment. 21 CFR 137.165 says enriched flour contains in each pound 2.9 milligrams of thiamin, 1.8 milligrams of riboflavin, 24 milligrams of niacin, 0.7 milligrams of folic acid and 20 milligrams of iron.
- UK fortification. The Bread and Flour Regulations 1998, as made, list the essential ingredients of flour in Schedule 1, for example calcium carbonate at not less than 235 and not more than 390 milligrams per hundred grams. Later amendments apply, so check the current text.
- Flour dust at the packers. In Great Britain, HSE's COSHH guidance gives flour dust a workplace exposure limit of 10 mg/m3 averaged over 8 hours and 30 mg/m3 over 15 minutes, and says less than 2 mg/m3 is usually achievable with good control. The HSENI flour dust page names flour dust and enzymes as one of the most common causes of occupational asthma in bakeries and milling, so burst bags and leaking spouts are dust events as well as lost bags.
The lab and the dosing control prove the flour rules, not a stop log. The line layer adds only time: a lab hold that stops the packer gets its own reason, while the record stays with QA.
Packing line losses in a flour mill
The mill itself is a continuous process, so its losses show as low throughput, chokes and roll change stops. Most of the stop time a buyer can see sits in the packhouse, where packers also stand starved when the flour bin above them runs low: a mill problem showing up at the packer. For how OEE treats continuous and batch steps, see OEE for batch processes.
Packer speed sets the scale of these losses. A six-station flour bagging system with a double weigh hopper, from one mill equipment maker, is rated in its product data sheet at 22.5 tonnes an hour in 25 kg bagging, which is 900 packs an hour, or 15 bags a minute. A mill grinding 400 tonnes a day makes about 16.7 tonnes of flour an hour if it all went to bags, so a packer of that size outruns the mill. It works in bursts and waits on the bin in between, which is why "starved" deserves its own reason code.
Flour packhouse failure modes
| Loss | Early sign in line data | Fix |
|---|---|---|
| Packer starved by a low flour bin | Short stops booked as packer faults, clustered after mill-side alarms or bin switches | Take the bin level as a signal, book starved separately, agree a minimum level with the head miller |
| Valve bag jams and misplaced bags | Many stops under two minutes, rising after a new bag delivery | Log stops against the bag lot, check valve size and magazine settings with the bag supplier |
| Sewing or sealing head faults | Repeat stops on the same head, thread breaks per hour creeping up | Change needles and thread on a count, keep a spare head set up |
| Check weigher rejects | Reject count rising while speed holds, underweights just after a product change | Re-tare after each product change, check flour aeration at the spout |
| Burst bags and spout leaks | Cleaning stops and rejects together, dust complaints on the same shift | Review bag spec and spout seals, clean by vacuum, never by compressed air |
| Palletiser blocks | Packer stops with the packer itself healthy and the outfeed full | Separate reason code, check pallet supply and wrapper cycle time |
| Long product and bag size changes | Change minutes vary by a factor of two between crews | One written change sheet per bag size, timed and reviewed; see changeover time |
| Running below rated speed | Bags per hour under the ideal with no stops booked | Compare against the maker's rate per bag size; see reduced speed loss vs minor stops |
Worked example: what one 25 kg packer shift costs
Sample figures for illustration only, except the packer rate, which is the maker's rating quoted above. A wheat mill grinds 400 tonnes a day and packs bakery flour in 25 kg bags on one six-station packer, two 8-hour shifts a day. Agree the time definitions before you compare packers or mills; our OEE and ISO 22400 guide covers them, and our OEE calculation guide shows each formula step by step.
| Step | Figure | How it is worked out |
|---|---|---|
| Planned production time | 450 min | 480 min shift minus 30 min planned breaks and cleaning |
| Stops | 90 min | Starved by the bin 40, bag jams 25, product and bag size change 15, palletiser block 10 |
| Run time | 360 min | 450 minus 90 |
| Availability (A) | 80.0% | 360 / 450 |
| Ideal output in run time | 5,400 bags | 360 min x 15 bags a minute |
| Bags packed | 4,860 | From the packer count |
| Performance (P) | 90.0% | 4,860 / 5,400 |
| Good bags | 4,763 | 4,860 minus 97 check weigher rejects and burst bags |
| Quality (Q) | 98.0% | 4,763 / 4,860 |
| OEE | 70.6% | 0.800 x 0.900 x 0.980; check: 4,763 / (450 x 15 = 6,750) |
The gap to a perfect shift is 6,750 minus 4,763, or 1,987 bags, nearly 50 tonnes of flour. It splits cleanly by loss: 1,350 bags to the 90 stopped minutes, 540 to slow running, and 97 to rejects. At a sample contribution of EUR 1.20 per 25 kg bag, the whole gap is worth EUR 2,384.40 a shift. Nobody recovers all of it, so price the part a team can act on.
Say the mill takes the bin level as a signal and agrees a minimum level, and the packer team fixes the worst bag lot. That is reachable: the bin refills in the 8 hours without packing, as the mill grinds about 400 tonnes a day and two shifts bag about 243. Starved minutes fall from 40 to 10 and jams from 25 to 15, so 40 minutes come back. At the shift's own speed and quality that is 40 x 15 x 0.90 x 0.98, or about 529 good bags. At EUR 1.20 a bag:
- Per shift: 529 x EUR 1.20 = EUR 634.80.
- Per month, at 42 shifts: EUR 26,661.60.
- Per year, at 504 shifts (42 x 12): EUR 319,939.20.
- New OEE: 5,292 good bags / 6,750 = 78.4%, with availability up from 80.0% to 88.9%.
The margin only counts when bagged orders are waiting. With spare packhouse hours, the 40 minutes are worth the overtime they avoid, a smaller figure, so price it with finance. One check on the ideal: set it from a good shift, say 780 bags an hour, and the same shift shows a performance of 4,860 / (360 x 13) = 103.8%. Over 100% means the ideal is wrong; use the maker's rating per bag size.
Which flour mill software to buy first
Start with the pain that costs the most today. An open audit finding on treatment or labelling comes first; beyond that, weigh lab and dosing records against a floor layer on the packers.
The sales mix changes the order. A mill selling mostly bulk flour by tanker puts the lab, dosing and dispatch first. A mill with retail packs and many sack sizes loses more hours in the packhouse, so the floor layer pays sooner.
Book a demo to see how a packer's stops, bag counts and lost money appear on one shift timeline.
Who hands what between flour mill systems
Name an owner for each link before the first shift goes live. The most useful link for the packhouse is a single signal from the mill control: the bin level or run state that lets a packer stop be booked as starved, not as a packer fault.
The same hand-offs decide how fast QA answers a complaint about weak dough: bins, improver rate, lab results, pallets and packer times must line up. That trace breaks where systems run on different clocks, so give them one time source and one lot code owner.
Five questions for flour mill software vendors
| Question | What a good answer shows |
|---|---|
| Does it run the mill, or read from the mill control? | A floor layer should only read. Ask which signals it takes from the SCADA and who agreed them with the head miller. |
| Where do ash, moisture and extraction live? | The answer should be the lab records. Be wary of line software that offers to calculate extraction. |
| Can a packer stop be booked as starved by the mill? | Ask for a bin level or run state input, and a reason group for mill-side causes. |
| Can one line hold 1 kg packs and 50 kg sacks? | Ask for a separate ideal rate per bag size, set at the packer. |
| Who owns the flour lot code? | One owner, usually the ERP, with the WMS for bags and tankers. Watch one lot code travel from the lab sheet to the bag and the ticket. |
What to do this week and this quarter
This week, for the production or packhouse manager:
- Add up last week's packer stop minutes by cause: starved, jams, sealing, changes, rejects, palletiser.
- Time one bag size change on the busiest packer, to the first good bag.
- Ask the head miller which mill control signal shows the bin above the packer running low.
- Write down the maker's rated bags per hour for each bag size.
- Walk one shift with QA and count burst bags and spout leaks.
This quarter:
- Put a run signal and a bag count on the busiest packer and the palletiser, and split starved time from packer faults.
- Agree 8 to 12 stop reasons with the crews, in their own words.
- Price one packer minute with finance, from margin per bag and overtime cost.
- Set a target on the largest loss, such as halving starved minutes, and review it weekly.
- Send bag counts and stop minutes to the ERP.
Fabrico in a flour mill packhouse
Fabrico is a cloud OEE and light MES platform. In a flour mill it covers:
- Bagging line OEE: valve and open-mouth packers, sewing or sealing heads, check weigher and palletiser are each logged with stops and bag counts, with a separate ideal rate per bag size.
- Stop reasons from the crew: the crew picks why the packer stopped, on a tablet or phone, from a short list that splits bag jams, bin empty, product change and lab hold.
- Run and stop time in the mill: where a roller mill, sifter or conveyor already gives a run signal, its running and stopped minutes are recorded per shift, with lost time shown in money. The mill control keeps running those machines.
Where 25 or 50 kg sacks are stacked by hand, there is no machine count. The camera add-on fills that gap by counting the sacks. Its video for that moment opens from the shift timeline; it is streamed on request and not stored in Fabrico. The FMCG camera guide and the computer vision add-on page explain how the count works.
The ERP takes bag counts and stop minutes by REST API, webhooks or a CSV export. Read OEE software for the platform, light MES vs full MES for where a full MES takes over, and the flour and grain milling maintenance software guide for planned work on rolls and sieves.
Mill control, lab records, dosing, the ERP and dispatch each keep their own home, and QA owns the quality records. Quality inspection is not part of Fabrico. Production planning and scheduling are not part of Fabrico today.
Questions flour mill managers ask
What is flour mill software?
Several products, not one: mill control or SCADA, intake and lab records, blend and treatment control, an ERP, a warehouse and dispatch system, and OEE on the packing lines. Each answers a different question.
What does flour mill ERP software do?
It runs the business side: wheat contracts and intake tickets, flour products and customers, lots, stock, invoices and costing. It counts packed bags once the run is booked, not the minutes the packer stood still or why.
Is the mill SCADA the same as an MES?
No. The mill control system runs the rolls, sifters, conveyors and bins, and holds the flow settings. An MES or light MES sits beside it and records run time, stops and output per machine and shift, with the reason the operator picks.
Where does extraction rate belong?
In the lab and QA records, worked out from wheat in and flour out over a run, not in line software.
What OEE should a flour packer reach?
There is no fixed figure. Set the ideal from the maker's rating for each bag size, then track availability, performance and quality per shift. In the sample shift above, 70.6% rose to 78.4% once starved and jam minutes fell.
Want to see where packhouse hours go? Book a demo to see a bagging line's stops, bag counts and lost money per shift.
Related articles
Latest from our blog


Real Fabrico tiles, sample data.