


 Login
 Blog
Can a Camera Tell Why the Line Stopped? What It Can and Cannot Do

Key takeaways
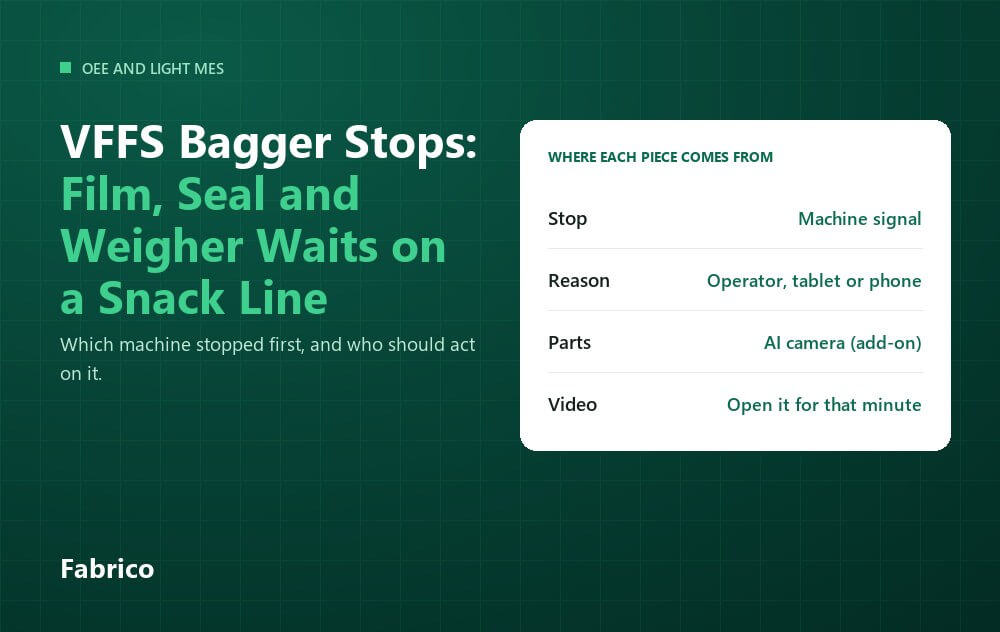
- Not today. A camera does not tell you why the line stopped. The machine signal gives the stop, and the operator adds the reason.
- You can open the camera video for that minute and look. In the standard setup, camera video is streamed, not stored in Fabrico.
- The AI camera (an add-on) counts parts, so shortfalls and empty pockets show in the count.
- The operator's reason feeds the stop Pareto and OEE (overall equipment effectiveness) by line and shift.
- It cannot see inside the controller, judge a part against its spec or know why a person stopped the line.
By the numbers
- Large plants suffer an average of 25 unplanned downtime incidents a month, down from 42 in 2019. (Siemens, 2024)
- 28% of large US manufacturers rank vision systems as a first or second investment priority for the next 24 months. (Deloitte, 2025)
- Automated optical inspection is the leading industrial AI use case, with a share of about 11% across the 48 use cases IoT Analytics tracks. (IoT Analytics, 2025)
Not today. The machine signal tells you when the line stopped, and the operator adds why. A person can then open the camera video for that minute and check the reason against what happened, not against memory.
Fabrico is a cloud-based OEE and light MES (manufacturing execution system) platform. Its software logs stops from the machine signal, prices each loss in money and shows OEE live by line and shift. The AI camera is an add-on that counts parts.
What can a camera show when a line stops?
A camera on the line is a witness. A PLC (programmable logic controller) knows the machine's state, but it often cannot show that product stopped moving. When you open the video for that minute, you may see these scenes:
- An infeed jam: product tipped over or piled up where it enters the machine.
- A blockage: the outfeed is full, so the machine has nowhere to put product.
- An empty infeed: nothing arrives, so the machine is starved by one upstream.
- A manual intervention: a guard opens and someone steps in to clear or adjust the machine.
- Nothing in view: no cause is visible, so the reason has to come from the operator or the fault codes.
The video shows the scene; a person who knows the line names the cause. Our guide to camera based production monitoring covers where to point the camera and how light affects it.
How does a stop get its reason, step by step?
- The machine signal gives the stop. The PLC or other machine signal gives the start and the end.
- The stop shows on the line screen, with its minutes, waiting for a reason.
- The operator adds the reason from the plant's own reason list.
- If the reason is unclear, open the camera video for that minute. Look at what happened, then pick the right code.
- Short stops need a rule. Below a threshold the plant picks, two minutes for example, ask for no reason and count them instead. Asking about each 30 second jam trains people to tap anything.
- The reason feeds the reports: the stop Pareto and OEE by line and shift, next to the minutes and the cost.
A stop without a reason explains nothing, and a reason is only as good as the list behind it. Our guide to micro stops shows what to do with the short stops. For the setup, read how to connect line cameras to MES downtime codes.
What can a camera not tell you about a stop?
A camera sees one field of view, in one range of light. It cannot tell you:
- What happened inside the controller. A drive fault or a failed sensor looks like a machine that simply stopped.
- Whether a part was out of spec. A badly glued case blank can look normal on video. This is not product inspection.
- Why a person stopped the line, for example to check a seal. The video shows a stop with no visible fault.
- What is out of frame or in poor light. A jam behind a guard or glare from a window can hide the cause.
So the operator stays in the loop. The video turns "what happened?" into a quick look instead of a guess. It also protects the operator: the morning meeting talks about the machine, not about who was standing there.
What does a stop reason look like in a worked example?
Sample line (illustrative numbers, not a customer). A bottle labeller runs at 200 bottles a minute. It is the first hour after a changeover, 06:00 to 07:00. A camera covers the infeed, the outfeed and the label magazine. The short-stop threshold is 2 minutes.
Before, the PLC logged stops of 2 minutes or longer, and the operator wrote reasons at the end of the hour from memory. Shorter stops were dropped. Here is the same hour with the machine signal logging the stops, short ones included, and the operator adding reasons after the restart:
| Start | Minutes | What you may see in the video | Operator's reason |
|---|---|---|---|
| 06:04 to 06:52 | 4 (4 short stops) | Bottles tipped at the infeed | Counted as short stops, no reason asked |
| 06:11 | 4 | Bottles piled up at the infeed | Infeed jam |
| 06:23 | 6 | Outfeed full, labeller waiting | Blocked by the case packer |
| 06:38 | 5 | Guard open at the label magazine | Label reel splice |
| 06:47 | 3 | Empty infeed, no bottles arriving | Starved by a filler stop |
| 06:55 | 3 | Machine still, nothing visible | Label sensor fault |
| Total | 25 |
Method note: Sample line, illustrative numbers, not a customer. Every result here comes from the inputs listed and the formula shown with it, so anyone can repeat the calculation.
The reason table for the hour, before and after:
| Reason | Before: from memory (min) | After: added by the operator (min) |
|---|---|---|
| Jam | 7 | 4 |
| Short stops at the infeed | Not recorded | 4 |
| Blocked by the case packer | 0 | 6 |
| Label reel splice | 0 | 5 |
| Starved by a filler stop | 0 | 3 |
| Label sensor fault | 0 | 3 |
| Other | 14 | 0 |
| Total recorded | 21 | 25 |
- Recorded stop time: 21 minutes before, 25 after. The 4 extra minutes are the short stops the old log dropped.
- Share of "Other": 14 / 21 = 66.7% before, 0% after.
- The operator added 5 reasons. For two of them, the video for that minute settled what the operator was unsure of.
- Lost output: 25 x 200 = 5,000 bottles. At a sample margin of $0.10 a bottle (€0.10 in a euro plant), that is $500 for the hour, or €500.
Before, the 3 starved minutes were logged as a jam, and "Other" was the biggest bar. After, the operators' reasons charge those minutes to the filler upstream, and the case packer and the label reel show up.
How do you start with stop reasons and camera video?
Start with the loss, not the camera:
- Pick the station where stops most often end up as "Other".
- Clean up the reason list first. A video cannot fix a bad list.
- Agree the short-stop threshold with the people who run the line.
- Review stops without a reason each morning. Our guide to unclassified downtime shows how.
To see video next to the OEE chart, read about an OEE dashboard with video context.
Fabrico starts with a pilot on one line. See how stops and camera video sit on one timeline on the computer vision OEE feature page (the camera is an add-on). There is no free plan and there are no tiers: each plant gets a quote. Suggested stop reasons are on the roadmap, not in the product today.
Proof from a named plant: Ficosota (also a Fabrico investor) raised OEE from 53.1% to 59.6% on 16 lines, June to September 2026, with monthly good output up 23.2%. Read the Ficosota case.
Toyota calls jidoka "automation with a human touch": the machine stops on a problem, and a person decides what happens next. (Toyota, Toyota Production System)
Frequently asked questions
Can a camera find the root cause of a stop?
No, not by itself. The machine signal gives the stop and the operator adds the reason. Why the bottles tipped is for the team to find, with the video for that minute and the fault codes in front of them.
What happens if the operator does not add a reason?
The stop stays without a reason. Its minutes still count as lost time in OEE, and it shows up in the morning review. Adding a reason should be quicker than skipping it: pick from a short list on the line screen, right after the restart.
Does the camera watch the operators?
It should not. A line camera should watch product and machines and give no scores per operator. The European Data Protection Board's video guidelines (3/2019) say employers should not rely on consent for video at work. This is not legal advice: check with your data protection officer and, in Germany, your works council.
Where is the video kept, and for how long?
In the standard Fabrico setup, camera video is streamed, not stored in Fabrico. If a plant records video of its own, where it is kept, for how long and who can open it depend on the product and on your IT rules. Agree these points in writing before the first camera goes up.
Related articles
Latest from our blog


Real Fabrico tiles, sample data.