Login
 Blog

Production Efficiency: Formula, Examples and How to Improve It

Key takeaways
- Production efficiency compares what a process actually produced with what it should have produced in the same time.
- The formula is simple: actual output ÷ standard output × 100. The hard part is choosing the right standard and the right time base.
- The same shift can honestly report 84.0%, 75.6% or 71.8%, depending on which time you count and whether you count bad parts.
- Production efficiency over run time tells you how fast you ran. OEE also tells you how much time you lost to stops and how much you scrapped.
- Stops nobody recorded are often a large share of the loss, so measure at the machine before you try to improve anything.
What is production efficiency?
Production efficiency is the ratio between the output a process actually delivered and the output it was designed or planned to deliver.
It is expressed as a percentage. 100% means the process ran exactly at its standard rate.
Plant managers use it to answer one practical question: are we getting the output this line is capable of?
It applies to a single machine, a line, a work cell or a whole plant, as long as you have a clear standard to compare against.
Production efficiency vs productive efficiency
Search for the term and you will also find productive efficiency from economics.
That is a different idea: an economy producing on its production possibilities frontier. This guide is about the shop floor meaning.
The production efficiency formula
The standard formula is: Production efficiency (%) = Actual output ÷ Standard output × 100
Standard output is what the process should produce in the time you are measuring, at its standard rate.
You can write the same idea in three ways. They give the same answer when the time base is the same.
| Version | Formula | Best for |
|---|---|---|
| Output-based | Actual output ÷ standard output × 100 | Lines that make one product per run |
| Rate-based | Actual output rate ÷ standard output rate × 100 | Comparing runs of different lengths |
| Time-based | Standard time earned ÷ actual time used × 100 | Mixed products with different cycle times |
Where the standard comes from
The standard rate should come from the ideal cycle time: the fastest time the process can make one good part under optimal conditions.
If you set the standard from last year's average instead, your efficiency will look good while the line keeps losing output. Our guide to ideal cycle time explains how to find the right number.
Worked example: one shift, three honest answers
Here is a typical shift on an assembly line, with round numbers to keep the math easy. Replace them with your own figures.
| Item | Value |
|---|---|
| Shift length | 480 minutes |
| Planned breaks | 30 minutes |
| Planned production time | 450 minutes |
| Unplanned stops (breakdown and a long jam) | 45 minutes |
| Run time | 405 minutes |
| Ideal cycle time | 60 seconds per unit (60 units per hour) |
| Total units produced | 340 |
| Rejected units | 17 |
| Good units | 323 |
Answer 1: efficiency over run time = 84.0%
In 405 minutes of running, the line should make 405 units at one unit per minute.
It made 340. So 340 ÷ 405 × 100 = 84.0%.
This number only describes speed while running, so it equals the OEE performance factor. It ignores the 45 minutes of stops completely.
Answer 2: efficiency over planned time = 75.6%
In 450 planned minutes, the line should make 450 units.
It made 340. So 340 ÷ 450 × 100 = 75.6%.
This version now includes the stops, but it still counts the 17 rejected units as if they were good.
Answer 3: OEE = 71.8%
Overall equipment effectiveness (OEE) only counts good units against planned time.
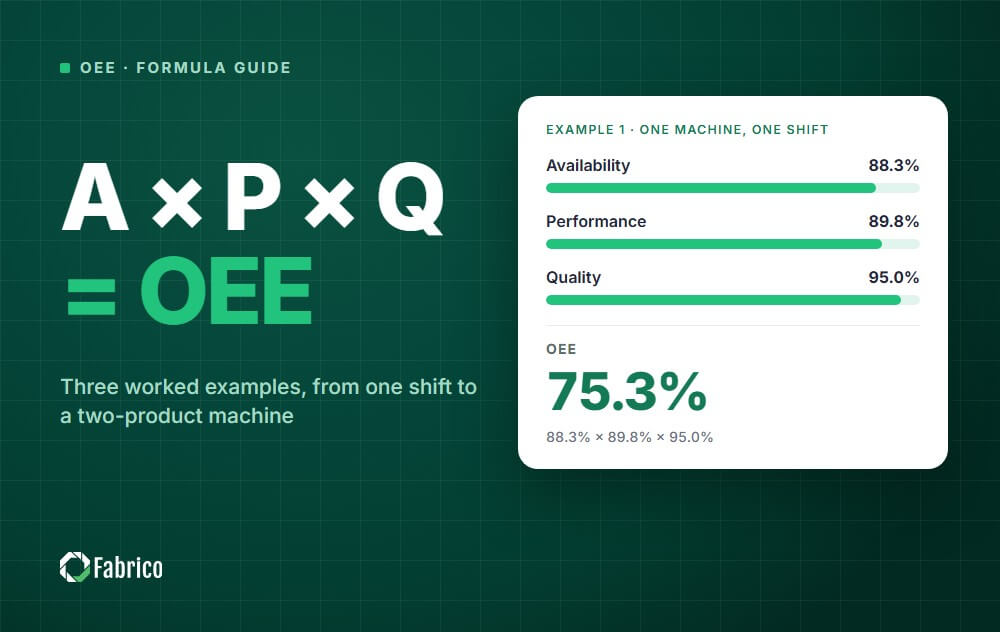
- Availability = 405 ÷ 450 = 90.0%
- Performance = 340 ÷ 405 = 84.0%
- Quality = 323 ÷ 340 = 95.0%
- OEE = 90.0% × 84.0% × 95.0% = 71.8%
You can check it in one step: 323 good units × 1 minute ÷ 450 minutes = 71.8%.
What the three answers tell you
| Metric | Result | What it hides |
|---|---|---|
| Efficiency over run time | 84.0% | All downtime and all scrap |
| Efficiency over planned time | 75.6% | All scrap |
| OEE | 71.8% | Nothing inside planned time |
None of these numbers is wrong. The mistake is reporting one without saying which one it is.
If your team reports 84% and the plant misses its volume target, this gap is usually the reason. For the full step-by-step method, see our OEE calculation guide.
Production efficiency vs OEE, productivity and utilization
These four metrics are easy to mix up, so here is how they differ.
| Metric | Question it answers | Typical formula |
|---|---|---|
| Production efficiency | Did we produce at the standard rate? | Actual output ÷ standard output |
| OEE | How much of planned time made good parts at full speed? | Availability × Performance × Quality |
| Productivity | How much output per unit of input? | Output ÷ labor hours (or cost, or energy) |
| Utilization | How much of the available time did we use? | Time used ÷ time available |
A simple way to remember it: efficiency over run time is about speed, OEE is about lost time, speed and quality together.
Productivity can rise while efficiency falls, for example when a line runs with three operators instead of four and slows down a little. Our comparison of productivity vs efficiency goes deeper.
What is a good production efficiency?
There is no universal benchmark, because the result depends entirely on how tight your standard is.
A line with a loose standard can report 95% while a line with a strict standard reports 80% and makes more.
Use these rules of thumb instead:
- Compare a line with itself over time, with the same standard and the same time base.
- Treat anything above 100% as a warning. If your standard is based on the ideal cycle time, it usually means the standard is too slow or the count is wrong.
- Use OEE for comparisons between similar lines, because it is anchored to the ideal cycle time by definition, while efficiency standards vary from plant to plant. An OEE of 85% is the widely cited world-class figure, but most plants measure well below it (see world-class OEE).
Five mistakes that make efficiency numbers lie
1. A standard that is too slow
Imagine the example line was given a standard of 50 units per hour, based on "what it usually does", instead of 60.
Standard output over the 405 run minutes becomes 337.5 units. Efficiency jumps to 100.7%, and nobody looks for the missing speed.
2. Counting bad parts as output
A unit you scrap or rework still used machine time.
If you count it as output, a line that runs fast and makes defects looks like your best performer.
3. Measuring only over run time
This is the most common way downtime disappears from a report.
Always state the time base, and track availability separately if you only report run time efficiency.
4. Averaging percentages
Line A makes 900 of a standard 1,000 (90%). Line B makes 100 of a standard 200 (50%).
The simple average is 70%. The true combined figure is 1,000 ÷ 1,200 = 83.3%.
Always add up outputs and standards first, then divide.
5. Relying on manual logs
Operators record long breakdowns. They rarely record a 40-second jam that happens 30 times a shift.
Those micro stops show up as "slow running", and the real cause is never found.
Where efficiency is lost: the six big losses
The classic six big losses framework is the best map of where output goes missing.
| Loss (OEE factor) | Example and first thing to try |
|---|---|
| Equipment failure (Availability) | Example: Motor trips, conveyor breaks First thing to try: Preventive maintenance on the repeat offenders |
| Setup and adjustments (Availability) | Example: Changeovers, first-off approval First thing to try: SMED on the longest changeover |
| Idling and minor stops (Performance) | Example: Jams, sensor blocks, starved infeed First thing to try: Automatic stop capture to find the top three |
| Reduced speed (Performance) | Example: Running below rated speed "to be safe" First thing to try: Find the reason the speed was lowered |
| Startup rejects (Quality) | Example: Scrap after a changeover or restart First thing to try: Standard settings for each product |
| Production rejects (Quality) | Example: Defects during a stable run First thing to try: Check the process at the point of the defect |
12 ways to improve production efficiency
The list is ordered the way most plants should tackle it: measure first, then remove stops, then speed up, then cut scrap, then sustain.
1. Measure at the machine, not on a clipboard
Automatic data from the PLC, a retrofit sensor or a camera records stops, including the short ones.
Our guide to machine monitoring systems compares the three options.
2. Fix the standard before you chase the number
Set the standard rate from the ideal cycle time for each product.
Write it down, and change it only through a controlled review.
3. Give every stop a reason
Use a short list of stop reasons that operators can pick in seconds.
Fifteen to twenty-five clear reasons work better than a hundred vague ones. See downtime reason code design.
4. Attack the biggest loss first
Rank your losses by minutes lost and work on the top one or two.
A Pareto chart usually shows that a handful of causes drive most of the lost output.
5. Shorten changeovers with SMED
Separate the steps that must happen with the machine stopped from the ones that can be prepared in advance.
Then move as much work as possible outside the stop. Our SMED guide walks through the method.
6. Make short stops visible
Count how often the line stops for less than two minutes, and which station causes it.
Frequent short stops are often cheap to fix: a guide rail, a sensor position, a product that is slightly out of spec.
7. Prevent the breakdowns you already know about
Most repeat failures come back at the same place: the same bearing, the same belt, the same sensor.
Put them on a preventive maintenance schedule based on run hours or cycles, and let operators handle cleaning and basic checks through autonomous maintenance.
8. Shorten the repairs you cannot prevent
Repair time grows when technicians wait for parts, drawings or the machine's history.
Keep critical spares in stock and the asset history one scan away. See mean time to repair for the levers.
9. Run the bottleneck at its rated speed
Output of the whole line is set by its slowest step, so check that the bottleneck runs at its ideal cycle time and never waits for material.
An hour gained at the bottleneck is an hour gained for the whole line. An hour gained elsewhere often is not.
Our guide to bottleneck analysis shows how to find it.
10. Make it right the first time
Every rejected unit wastes the machine time that made it.
Track first pass yield by product, and fix startup scrap with standard settings for each changeover.
11. Standardize the work and train to it
Two operators on the same line often run it at different speeds.
Capture the best known method as standard work, then train every shift to it.
12. Review the numbers every day
A short daily review keeps losses from becoming normal.
Look at yesterday's top three losses, agree one action each, and check them the next day. Our daily OEE meeting guide gives a simple agenda.
A four-week plan to raise production efficiency
- Week 1: pick the bottleneck line, confirm the ideal cycle time for each product and agree on one time base.
- Week 2: start automatic data capture and introduce a short stop reason list.
- Week 3: build a Pareto of the losses and choose the top two to fix.
- Week 4: fix them, measure again and write down what changed.
Keep the scope to one line until the numbers are trusted. Rolling out an untrusted metric to ten lines only multiplies the arguments.
How Fabrico helps
Fabrico is an OEE platform with a full CMMS built in.
It collects data from your machines through PLC connections, IoT sensors and AI cameras, and calculates availability, performance, quality and OEE in real time.
It detects micro stops, shows downtime, MTTR and MTBF by machine, and lets you export the data when you need it.
Because maintenance lives in the same platform, your team can open a work order or set up a preventive maintenance plan for a machine that keeps stopping, and check spare parts stock, without switching tools.
The AI assistant answers questions about a machine's losses and history in plain language.
Want to see your own production efficiency, measured instead of estimated? Book a demo.
For the bigger picture, start with our what OEE is guide.
Frequently asked questions
What is the formula for production efficiency?
Production efficiency = actual output ÷ standard output × 100.
Standard output is what the process should produce in the same time at its standard rate, ideally based on the ideal cycle time.
Can production efficiency be over 100%?
Yes, but treat it as a warning, not a win.
A result above 100% usually means the standard rate is set too low or the output count includes something it should not. If a line regularly beats its standard, review the standard against the ideal cycle time.
What is the difference between production efficiency and OEE?
Production efficiency over run time measures speed against a standard. OEE multiplies availability, performance and quality, so it also captures downtime and scrap.
In the example above, the same shift gave 84.0% efficiency over run time and 71.8% OEE.
What is the difference between production efficiency and productivity?
Efficiency compares actual output with a standard. Productivity compares output with an input, such as labor hours, cost or energy.
You can improve one without the other, so track both.
How often should production efficiency be measured?
Measure it continuously and review it at least once per shift or once per day.
Weekly or monthly reports are useful for trends, but they are too slow to catch the stops that cause the losses.
How do you calculate production efficiency for several products?
Use the time-based version. For each product, multiply the units made by its standard cycle time to get standard time earned.
Add those up, divide by the time base you chose (run time or planned time) and multiply by 100. State which base you used, because the two give different answers.
See how Fabrico unifies OEE and maintenance in one platform.
Request a demoRelated articles