


 Login
 Blog
Computer Vision for Coffee Manufacturing: Roasting and Packing Lines

In short: computer vision for coffee manufacturing pays off in the packing hall, not at the roaster: at the valve station and bagger, at hand-packing tables and at the end of line. Roasters, grinders and fillers already give good machine signals, and roast colour, seals and oxygen belong to inspection and lab systems.
- Treat the roastery and the packing hall as two lines. Degassing silos sit between them, so each needs its own OEE.
- A roaster runs in batches. Count it in batches or green kg, and keep roast weight loss out of the quality figure.
- On bag, brick and can lines, video for the minute helps most with short stops at the valve station, jaws and nitrogen supply.
- Fabrico takes stops and counts from machine signals and the reason from the operator. Its AI camera add-on counts output and opens the camera video for any moment on the shift timeline.
A coffee plant runs on two clocks. The roaster works batch by batch. The packing hall runs bags, bricks, cans or capsules by the minute, often hours after the beans left the drum.
This page is written for plant managers and CI leads picking camera and OEE software for a roasting and packing plant. If you are still comparing OEE software in general, start with our OEE software guide. We sell Fabrico, so hold what we say to the same test as any other vendor.
Why a lost minute costs more in coffee now
Coffee got expensive. Eurostat reports that the EU imported 2.9 million tonnes of coffee from outside the EU in 2025. That is only a little more than the 2.7 million tonnes of 2015, but the value rose from €8.6 billion to €18.7 billion.
So the average imported tonne roughly doubled in value, from about €3,200 to €6,400 in each year's euros. At import prices, every scrapped bag, split brick and gram of overfill now carries about twice the coffee cost of 2015.
Downtime isn't shrinking on its own either. Siemens' True Cost of Downtime 2024 report surveyed large industrial firms in four sectors. FMCG was the only one of the four where downtime hours had not fallen since 2019.
What computer vision does in a coffee plant, and what it doesn't
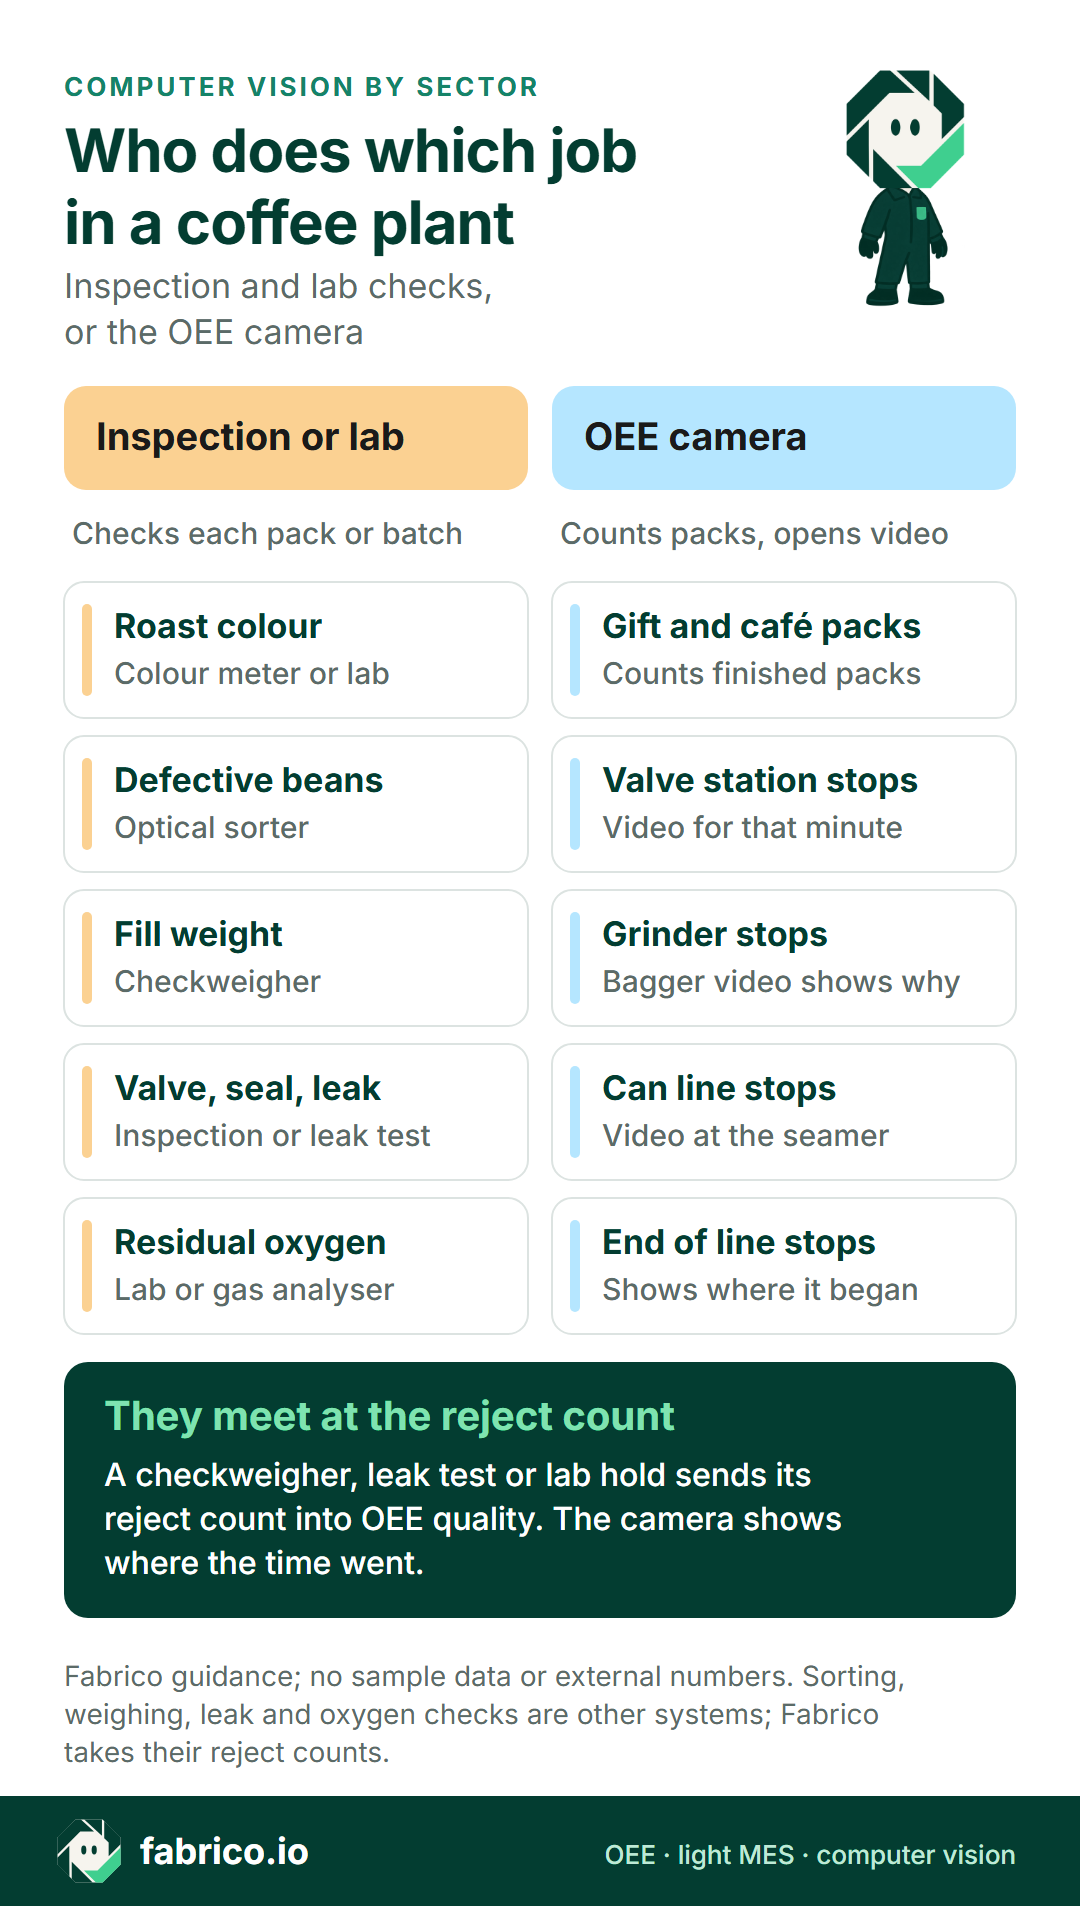
Three kinds of system get called "vision" here: optical sorters reject beans, inspection cameras check codes and seals, and an OEE camera counts output and shows the minute a line stopped. Only the last is about lost time.
| Job | Inspection or lab | OEE camera |
|---|---|---|
| Remove defective or foreign beans | Optical sorter, destoner, metal detection | No |
| Roast colour on target | Roast colour meter or lab | No |
| Fill weight | Checkweigher | No |
| Valve present, seal, leak | Inspection or leak test | No |
| Residual oxygen | Lab sample or gas analyser | No |
| Count hand-packed gift and café packs | Not its job | Yes |
| Show why the bagger stopped | No | Video for that minute |
The two meet at the reject count: a checkweigher or leak tester sends it, and OEE software books it as a quality loss, knowing how many packs failed but not why. More in label and code vision vs an OEE camera.
Where the losses hide in a roasting and packing plant
The roaster: batches, not a line speed
A batch roaster has no line speed. It has a cycle: charge, roast, drop, cool. A continuous roaster is measured like any process, in green kg an hour against its rated throughput. Measure a batch roaster in batches against an ideal charge-to-charge time for each blend and roast degree, or in green kg an hour.
Watch the gaps between batches: green coffee not weighed out, a blend not released, a full silo downstream. The roaster control knows when each batch was charged and dropped, so those gaps come straight from the signal.
Keep roast weight loss out of quality. A peer-reviewed study from the Zurich University of Applied Sciences notes that around 20% of dry matter is lost for dark roasted coffee. That is the process, not a defect. A batch that misses its colour target and gets blended back or scrapped is the quality loss.
A camera adds little here: the roaster's controls know more than a picture of the drum. For burner, fan and chaff collector care, see maintenance software for coffee roasting.
Degassing silos and the grinder
Roasted coffee keeps giving off carbon dioxide, so whole beans usually rest in silos before packing. Those silos split the plant in two: the roaster can run while the packer is down, and the packer can run on yesterday's roast. When the next blend has not finished its degassing hold, the packer is starved, not slow. Give "waiting for degassing release" its own starved code, so it is not booked to the packing crew.
Ground coffee is different. The Zurich study says that after grinding, the rate of degassing is greatly increased. It cites reported losses as high as 40 to 50% of the trapped gas within the first few minutes, and finer grinds lose more than coarse ones. How long ground coffee waits before packing is a process decision per pack type.
Where that wait is short, a bagger stop soon stops the grinder, which logs a stop it didn't cause. Split every stop into own fault, starved and blocked.
Bag, brick and can packing
The Zurich paper calls the one-way valve bag the most common coffee packaging format: gas gets out, air stays out. Each pack type stops in its own places.
- Valve bags. A valve reel running out, a valve placed off its mark or film creasing at the valve station each stop the bagger. The jaws, film splices and weigher add the rest; see VFFS bagger stops.
- Vacuum bricks. A soft brick or a vacuum fault gets rejected, and a run of them stops the machine.
- Cans and tins. The lid feed and the seamer are the usual short stops.
Nitrogen runs through all three. If supply pressure drops, the line may run on while residual oxygen drifts out of spec, and product goes on hold when the lab result comes back. Code nitrogen faults as their own stop, and agree how held product counts in OEE.
Weight is the other leak. A heavy bag still counts as good, so overfill never shows in OEE. Track it alongside, as in our guide to giveaway and overfill.
Capsules and pods, in short
Capsule and pod lines are fast and the PLC counts them well. Our page on coffee capsule line stops shows where those cameras go, and OEE for coffee capsule lines covers lanes, nitrogen and weights.
Blends, grinds and pack sizes
Many coffee plants run dozens of blends, roasts and grinds in retail, private label and café sizes. Every switch is a changeover: a blend at the roaster, a grind at the grinder, a film or carton at the packer.
A move to decaf or an organic blend may need a fuller clean-out, to the plant's own rules. Give each type its own code and standard time, and never cut a required clean to lift OEE. Sites that also pack tea will know the pattern from OEE for tea packing lines.
Hand packing and the end of line
Gift boxes, sample packs and mixed café cases are often packed by hand at a side table. No PLC counts them, so a camera may be the only automatic count. See manual packing station OEE with a camera.
At the other end, a backed-up case packer stops the bagger, which logs the stop as its own. Video for that minute shows where it began; see case packer downtime on camera.
Coffee plant map: where the cameras go
Which system handles each job, from roaster to pallet:
The cameras cluster in the packing hall. Start at the busiest bagger, or a hand-packing table nobody counts.
Camera, sensor or operator for each coffee station
| Station | Counts and stops from | Where a camera helps |
|---|---|---|
| Roaster | Roaster control: charge, drop, temperatures | Rarely. The batch data says more |
| Cooler, destoner, sorter | PLC, plus the sorter's own rejects | No. The sorter is inspection |
| Grinder | PLC run state and motor load | Rarely. The bagger camera shows why it waited |
| Bagger, brick or can line | PLC count and stop signal | Video for short stops at the valve station, jaws or seamer |
| Gift and café hand packing | Nothing, or a paper tally | Counts finished packs at the done spot |
| Case packer, palletizer | PLC run state | Video shows if it stopped itself or was blocked |
| Weight, seal, oxygen checks | Checkweigher, leak test, lab | None. Their reject count feeds OEE |
In every row the signal times the stop and the operator picks the reason, with the video when the cause isn't obvious. More by machine type in camera or sensor by machine.
Want to check this against your own plant? Book a demo with a list of your stations and the signal each machine gives today.
Worked example: one shift, two clocks
This is sample data for one 480 minute shift. It is not a customer's plant and not a product screen.
The roaster. The ideal charge-to-charge cycle for this blend is 20 minutes, so 24 batches are possible. Waiting for green coffee cost 30 minutes and a blend change 20, leaving 430 minutes of run time: availability 89.6%. It finished 20 batches, 400 minutes of ideal time, so performance is 93.0%. One batch missed its colour target, so quality is 95.0%.
Roaster OEE is 89.6% x 93.0% x 95.0% = 79.2%. As a check, 19 good batches of the 24 possible is also 79.2%.
The packer. A bagger for 500 g valve bags with nitrogen flush, at an ideal 45 bags a minute. The signal timed 80 minutes of stops: a 30 minute grind change, 54 short stops at the valve station worth 18 minutes, 12 minutes of film splices and reel changes, a 10 minute nitrogen pressure stop, and 10 minutes blocked by the case packer.
Run time is 400 minutes: availability 83.3%. The ideal is 18,000 bags; the bagger counted 16,560, running below rated speed on the fine espresso grind, so performance is 92.0%. The checkweigher and leak test rejected 330, leaving 16,230 good: quality 98.0%.
Packer OEE is 83.3% x 92.0% x 98.0% = 75.1%. As a check, 16,230 good bags of the 21,600 possible is 75.1%.
Now the camera question. The PLC logged all 54 valve stops as "valve station fault". With the video for each minute, the operators coded 34 as film creasing at the valve station and 20 as valves placed off their mark, so the fix starts with film tension, not the valve applicator.
At an assumed contribution of €0.70 a bag, the 18 valve minutes are 810 bags, or €567 a shift. The 10 minutes over the 20 minute grind change standard are another 450 bags, or €315. The 10 blocked minutes belong to the case packer, not the bagger crew. That money is real only if the bags would have sold. Overfill sits outside OEE: one gram over on each of the 16,230 good bags is another 16 kg of coffee a shift.
Questions to ask any vendor of computer vision for coffee manufacturing
Put these to every vendor, us included. Bring one real shift from your plant.
| Ask | How to test the answer |
|---|---|
| How do you measure a batch roaster? | Hand over a shift of charge and drop times. Ask for OEE per blend. |
| Can the roastery and packing hall have separate OEE? | Ask how the silos are handled, and which number reaches the plant report. |
| Can it count hand-packed gift and café packs? | Film one run, count it by hand, compare. |
| Who gets the stop when the bagger blocks the grinder? | Take one real stop and ask which machine gets the blame. |
| Where do rejects and held product go? | Ask to see a checkweigher count and a nitrogen hold land in OEE. |
| Is video stored, and who can watch it? | Get the storage location, the retention time and the access list. |
| What does a pilot look like? | One packing line, fixed dates, a hand count to compare. |
For a pilot plan you can reuse, read how to run a computer vision OEE pilot.
Privacy and the works council
Packing halls and hand-packing tables have people in them. In Germany the works council must agree before a camera goes up, and in France staff representatives must be consulted first. Elsewhere, expect the same questions, and in a smaller roastery the crew will simply ask what it is for. The legal detail is in GDPR and production line cameras.
- Frame the product. The valve station, the jaws, the done spot, not faces.
- Write down the video rules. Fabrico's standard setup streams video on request without keeping it in Fabrico. Name who may open it.
- Report by line and shift. Never rank named operators.
Roadmap: wider automatic masking of people in view. The full approach is in production line cameras without surveillance.
How Fabrico does it
In a coffee plant, Fabrico runs as a cloud OEE and light MES platform. What it does today, and what it leaves to other systems:
- Machine data first: roaster, grinder, packers and end of line report stops and counts through a PLC, sensor or counter. Operators pick the stop reason on a tablet or phone.
- Losses in money: OEE and downtime per line and shift, with each loss priced, in the web app and on iOS and Android.
- Camera add-on: AI cameras count packs where no machine does, such as a gift-box table. Any moment on the shift timeline can be opened as camera video. In the standard setup that video is streamed on request, not stored in Fabrico.
- Open data: REST API, webhooks, and Excel or CSV export.
- On the roadmap, not live: cameras that spot stops by themselves, mark jam zones, or propose a stop reason for the operator to confirm.
- Left to other systems: roast colour, bean sorting, and weight, seal, leak and oxygen checks. Fabrico takes their reject counts. For planning and scheduling, ask us in the demo.
Test us with the seven questions above, like any other vendor. Book a demo or contact us.
What people ask next
Can an OEE camera check roast colour, valves or seals?
No. Colour meters, optical sorters, leak tests and lab samples do those jobs, and their reject counts belong in the quality part of OEE. An OEE camera counts packs and opens the video for the minute a line stopped.
Should the roaster and the packing line share one OEE?
Usually not. Degassing silos let each run on its own timing, so measure the roaster in batches or green kg and each packing line in packs a minute.
Where should the first camera go in a coffee plant?
Over the valve station and bagger jaws on the line with the most short stops, or at a hand-packing table with no count. One camera shows quickly whether more are worth it.
How do you measure OEE on a coffee roaster?
In batches or green kg an hour, against an ideal charge-to-charge time for each blend and roast degree. The roaster control gives charge and drop times, so the gaps between batches come from the signal. Keep roast weight loss out of quality; a batch that misses its colour target is the quality loss.
Is camera video stored?
Fabrico's standard setup streams video on request and does not keep it in Fabrico. Ask each vendor where their video lives, and put the reply in front of your works council.
What drives the cost of computer vision in a coffee plant?
Cameras, lines, mounting, network and training set the quote. Hand every vendor one identical station list and the quotes become comparable.
Want to see it on a coffee line like yours? Book a demo.
Related articles










Real Fabrico tiles, sample data.