


 Login
 Blog
Computer Vision for Furniture Manufacturing: Assembly, Upholstery, Packing

In short: computer vision for furniture manufacturing pays off as a counter at the manual end of the plant: cameras count what leaves hand sanding, assembly, upholstery and packing, where no machine gives a count, and let you open the video of a stop.
- Panel lines are well served already: the beam saw, edgebander and CNC drilling controllers usually know their own cycles and counts. Read them first.
- Cameras earn their place at manual assembly, upholstery, sanding, packing and on older machines with no usable signal.
- Edge, surface and hole checks are inspection. That is a different job, done by inspection systems or trained people.
- Furniture losses hide in changeovers between orders and colours, waiting for parts, rework after finishing, and batch-size-one flow.
- Fabrico's camera add-on counts output and lets you open the video for any moment on the shift timeline. The operator adds the stop reason.
Your edgebander knows how many panels it ran today. Your sanding bench, your upholstery cell and your packing table do not.
This page is for plant managers, operations and CI leads in panel and solid wood furniture plants who are choosing cameras and OEE software.
It shows where a camera earns its place, where the machine controller is the better count, and what to ask each vendor.
Computer vision for furniture manufacturing: two different jobs
Two kinds of camera system get sold to furniture plants under one name. Inspection systems look for defects on the part. OEE cameras count output and show you what happened at a stop.
| Job in a furniture plant | Inspection system | OEE camera |
|---|---|---|
| Edge defects: open glue, chipping, trimming | Yes | No |
| Surface defects after finishing | Yes, or a trained person | No |
| Hole pattern and part ID | Yes, or the CNC and a barcode | No |
| Count finished pieces or boxes | Often counts what it inspects | Yes, also at manual stations |
| Video of a stop | Defect images, not stop video | Open the video for that minute |
| Feeds OEE through | Its reject count | The output count |
Edge inspection is a project of its own. A 2025 study in the journal Drvna industrija trained a YOLOv7-Tiny model for edge banding defects on 1,887 images of six defect types, and reported 82.1% precision and 75.4% recall on industrial camera data. That is a research result from one team, not a buyer benchmark. It shows that inspection needs its own images, labels and tuning.
So keep the two apart in the spec. A reject count from an inspection system or a QC station can feed the quality part of OEE, so rejects are counted once. To test a counting camera before you trust it, read how accurate camera OEE is.
Panel furniture and solid wood: two different plants
The European Commission calls furniture "a labour-intensive and dynamic sector dominated by small and medium-sized enterprises (SMEs) and micro firms", with around 1 million workers in 130 thousand companies in the EU. In the United States, the Bureau of Labor Statistics counts about 329,500 jobs in furniture and related product manufacturing in October 2026 (preliminary), a group that also includes mattresses, window blinds, cabinets and fixtures.
Labour-intensive is the point for this page. Much of the output in furniture passes through hands, not through a PLC.
Panel furniture
Cabinets, wardrobes, kitchens, office and flat-pack furniture start as boards. A beam saw or a nesting router cuts them, an edgebander applies the edge, and a CNC drilling and dowelling machine bores the holes. Then parts are sorted, kitted by order, and assembled or packed flat.
The first three machines usually have controllers that log cycles, programs and often part counts. A 2022 study of the edge banding module on an automated door line, published in Applied Sciences, read retooling time, the number of retoolings and pieces per series straight from the IT system controlling the line. On a machine like that, read the controller. A camera there adds a picture, not a better count.
Solid wood and upholstered furniture
Chairs, tables, beds and sofas follow a different path. Solid wood goes through cross-cut saws, moulders and CNC routers, then hand sanding, gluing and assembly, finishing in spray booths, and drying. Upholstered pieces add cutting and sewing of covers, frame building, padding, covering and packing.
Here most of the value is added at benches and booths with no signal at all. That is where a camera that counts finished pieces earns its place.
Where the losses hide on furniture lines
Changeovers between orders and colours
On a panel line, a new order can mean a new board decor, a new edge colour, a new glue and a new program at the drilling machine. The edgebander has to change edge material and often clean or switch the glue unit. In finishing, a colour change in a spray booth means flushing guns and lines before the next colour.
Book changeovers with their own codes, by type: decor, edge colour, glue, finish colour. Then the time per type is visible, and you can sequence orders to cut it. Video helps here too; see changeover video analysis for SMED.
Waiting for parts
An assembly station that is missing one door, one drawer front or one bag of fittings stops, even if every machine upstream ran well. In upholstery, a covering station waits for a frame or a sewn cover. These waits often go unrecorded, because nothing broke.
Give "waiting for parts" its own stop reason, split by what was missing if you can. In many plants it turns out to be a large loss at assembly, and it points upstream to cutting, sorting and kitting, not to the station.
Rework after finishing
A scratch found after lacquering sends a piece back to sanding and spraying. That piece uses the booth twice and the drying space twice. If the count is taken only at packing, the rework disappears into a slow day.
Record rework as a quality loss where it is found, and do not count the reworked piece as new output when it passes again. A count at the booth exit and another at packing give you two numbers to compare.
Batch size one
Made-to-order furniture means many orders of one or a few pieces. Every piece can have a different size, so one ideal rate per machine makes the performance figure meaningless.
Set ideal rates by product family, or by part size class at the edgebander and the drilling machine. Then a slow day shows as slow running, not as noise. For software that handles this across the plant, see our guide to OEE software for wood and furniture plants.
Older machines with no usable signal
Many furniture plants run machines from several decades side by side. An old moulder or a manual panel saw may have no controller worth reading. A simple sensor or a camera can count there; see OEE on legacy machines without PLCs.
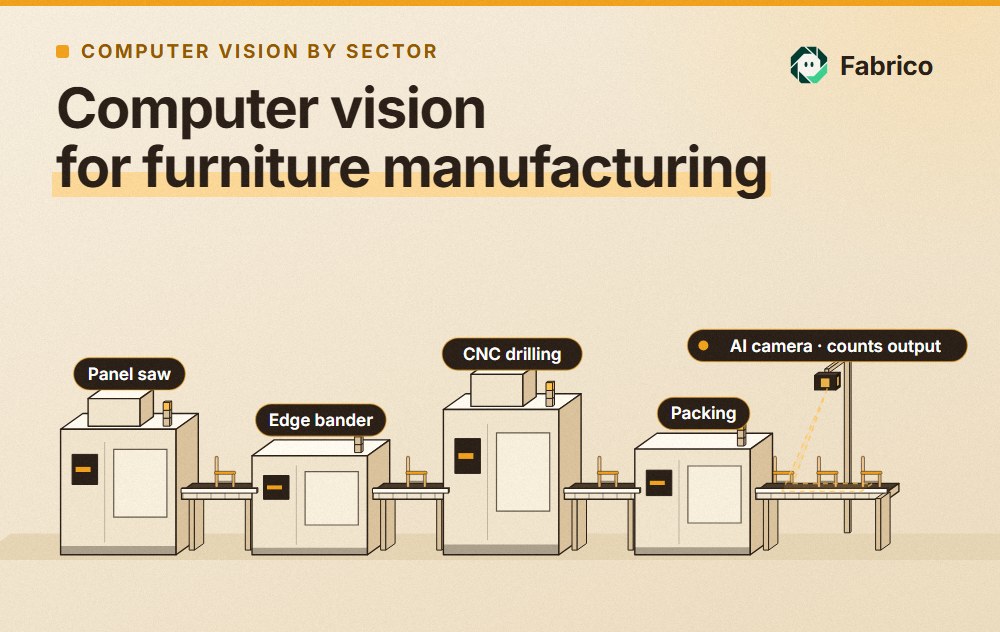
Where a camera goes in a furniture plant
Here is one example: a panel line and a solid wood and upholstery line in the same plant.
For a longer list by machine type, see camera or sensor for OEE, machine by machine.
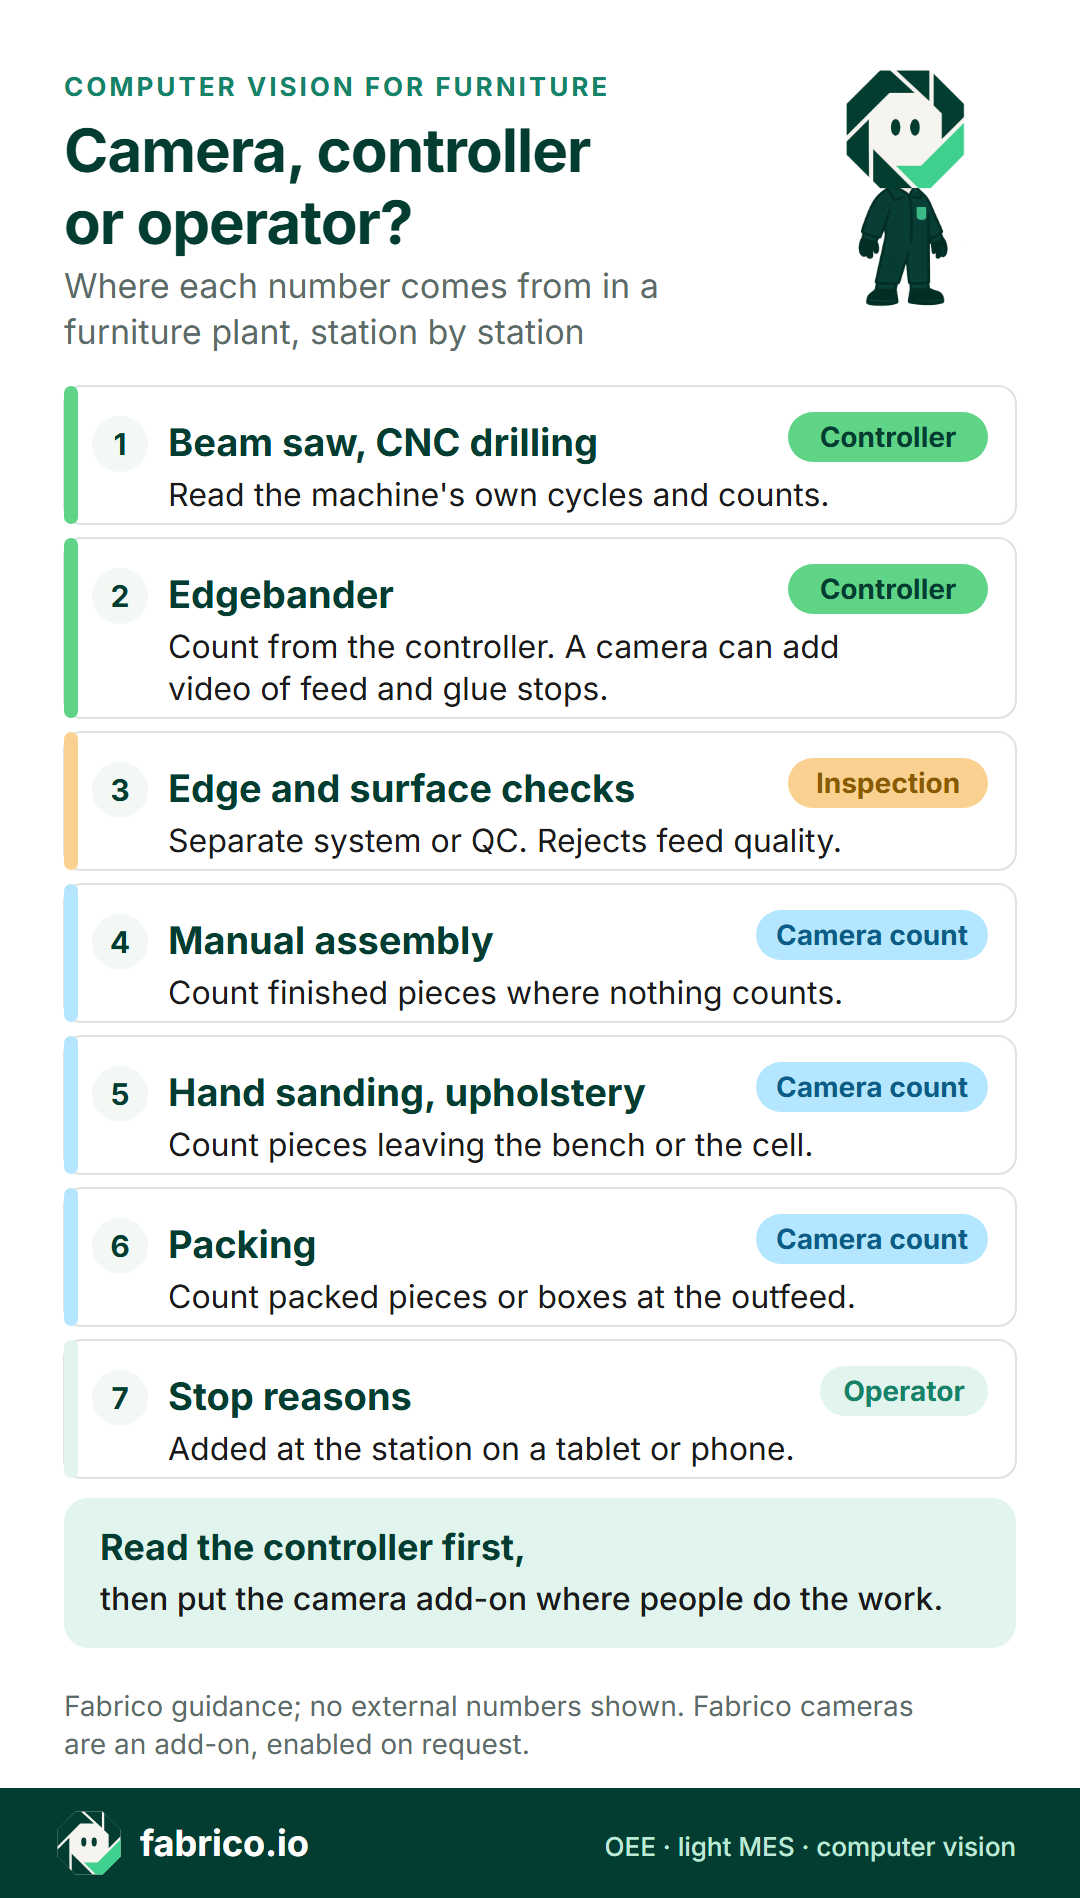
Camera, controller or operator: station by station
This is typical for a furniture plant, not a rule. Check each machine.
| Station | Count and stops from | What a camera adds |
|---|---|---|
| Beam saw or nesting router | Machine controller | Little. Read the controller. |
| Edgebander | Machine controller | Video of feed and glue unit stops |
| CNC drilling and dowelling | Machine controller | Little. Read the controller. |
| Sorting and kitting | Operator or scanner | Video when an order is short of parts |
| Manual assembly | Nothing, or a hand tally | Count of finished pieces |
| Hand sanding | Nothing | Count of pieces leaving the bench |
| Spray booth and drying | Conveyor controller on automatic lines, or nothing | Count at the exit of manual booths |
| Upholstery cell | Nothing | Count of covered pieces |
| Packing | Nothing, or a label printer | Count of packed pieces or boxes |
| Stop reasons, all lines | The operator, on a tablet or phone | Video to check a disputed reason |
You rarely need a camera at every station. Manual assembly is covered in more depth in computer vision for OEE in manual assembly, and packing in OEE at a manual packing station.
Bring your station list and one week of stop sheets to a demo, and we will go through it station by station.
Worked example: one shift at a cabinet assembly station
These are example numbers, and they describe no real plant. A two-person station assembles and packs kitchen cabinets. The ideal cycle is 3 minutes a cabinet, and the shift has 480 planned minutes.
Nothing upstream counts what this station finishes. A camera above the outfeed counts the cabinets that leave it. The team logs stops with their start, end and reason on a tablet, and marks the cabinets sent back for touch-up.
Stops took 90 minutes: waiting for parts 45, two order changeovers 30, and a clamp press fault 15. Run time is 390 of 480 minutes, so availability is 81.3%.
At 3 minutes a cabinet, 390 minutes could make 130 cabinets. The camera counted 117, so performance is 90%. The gap is 39 minutes of slow running.
Six of the 117 cabinets went back for touch-up after a door was misaligned or a panel was marked in assembly. That leaves 111 good, so quality is 94.9%. Those 6 cabinets are 18 minutes of station time.
OEE is 81.3% x 90% x 94.9% = 69.4%. Check it the short way: 111 good cabinets x 3 minutes is 333 of 480 minutes, also 69.4%.
Half the stop time was waiting for parts. No amount of effort at this station fixes that. The fix sits upstream, at cutting, sorting and kitting. Without a count and a reason code, that wait looks like a slow team.
Eight checks for any furniture camera or OEE vendor
Run these with every vendor, and with us. Bring one real shift from last week as the test case.
| Ask | How to test the answer |
|---|---|
| What exactly does the camera count? | Pieces, cabinets, boxes or sets? Ask how a flat-pack order of several boxes converts to finished units. Run it next to a hand count for one shift. |
| How does it handle batch size one? | Ask to see ideal rates by product family, and a shift where every order is different. |
| Can it read the saw and edgebander? | Ask which machines connect directly, and what comes through: run state, counts, program changes. |
| How are changeovers booked? | Ask for codes by type: decor, edge colour, glue, finish colour. |
| Where does waiting for parts show? | Ask for a missing-parts stop reason, and a report by station and shift. |
| How is rework counted? | Ask how a piece sent back to sanding or spraying lands in quality without being counted twice. |
| Does the camera cope with dust and overspray? | Ask about housings near sanding and booths, and what happens to the count when the lens gets dirty. |
| Is video kept, and who can open it? | Ask where it lives, for how long, and who sees it. |
Before you roll out across the plant, test on one line first. See the guide to a computer vision OEE pilot.
Cameras, privacy and the works council
Furniture plants are full of people at benches, and a camera over a sanding bench or an upholstery cell will see some of them. Tell staff before any camera goes up. In many European countries, talk to the works council first.
Frame the camera on the piece, the outfeed or the packing table, not the person. Report by station and shift, not by person. Ask each vendor, us included, what privacy masking is live today and what is still roadmap.
Fabrico's camera add-on counts product, not people. For a fuller checklist, read production line cameras without surveillance.
Where Fabrico fits
Fabrico is a cloud OEE and light MES platform. Here is what it does in a furniture plant today.
- Stops and counts: from the machine signal: the PLC of the saw, edgebander or drilling machine, or a Fabrico IoT device with external sensors on older machines.
- Stop reasons: the operator adds them at the station, on a tablet or phone.
- OEE and losses: OEE, downtime and losses by line and shift, with losses shown in money. On the web, iOS and Android.
- Camera add-on, on request: AI cameras count output at manual assembly, sanding, upholstery and packing, and on machines with no usable signal. With the add-on, you can open the camera video for any moment on the shift timeline. In the standard setup, video is streamed on request, not stored in Fabrico.
- Your data: it leaves through a REST API, webhooks and Excel or CSV export.
Roadmap, not live today: stops detected by the camera add-on, jam zones on the video, and the add-on suggesting a stop reason.
What Fabrico does not do: inspection of edges, surfaces or hole patterns, which stays with your inspection systems or QC and feeds Fabrico's quality figure through a reject count or signal. Fabrico does not optimise or nest your cutting. For planning and scheduling, ask us in the demo.
For the full product, see Fabrico computer vision for OEE. If you are still comparing platforms, read the guide to OEE software, and for what a light MES tracks in a wood plant, see MES for woodworking. All eight checks above apply to us too.
Bring one shift's stop sheet from an assembly or upholstery station to a demo, and ask us to show which numbers we can fill and which we cannot.
What people ask next
Which furniture station should get the first camera?
Usually the one with the weakest count and the most hands: a manual assembly station, an upholstery cell, a sanding bench or the packing table. Saws, edgebanders and drilling machines with a controller you can read come last.
Can a camera check edge banding and surface quality?
Yes, but that is an inspection camera, not an OEE camera. Edge defects, surface defects and hole patterns are checked by inspection systems or trained people. Fabrico does not sell inspection. The reject count from inspection or QC can feed the quality part of OEE.
Do I need a camera on the edgebander?
Usually not for the count. Most modern edgebanders log cycles and counts in their controller, and that is the better source. A camera can add video of what happened at the feed or the glue unit when the machine stopped.
Can a camera count furniture made to order, one piece at a time?
Yes. Fabrico's camera add-on counts finished pieces as they leave a station; agree the camera position for your largest and smallest pieces in the pilot. For OEE to mean something, set ideal rates by product family, so a large wardrobe and a small wall cabinet are not held to the same cycle.
Does computer vision work near sanding and spray booths?
It can, if the housing suits the dust and overspray and the lens is cleaned on a schedule. Mount cameras outside the booth and away from the spray path, and agree each position with your safety team. Ask each vendor what happens to the count when the lens gets dirty.
Is the camera video stored?
Not in Fabrico. In the standard setup, video is streamed on request, and with the camera add-on you can open it for any moment on the shift timeline. Ask every vendor the same question, and where their video lives.
What drives the cost of computer vision in a furniture plant?
Pricing is set per quote. The drivers are the number of stations and cameras, mounting and housings for dusty areas, the network to the hall, and training. Give each vendor the same station list so the quotes compare.
Want to see it on a line like yours? Book a demo and bring one shift of stop sheets from an assembly or packing station.
Related articles









Real Fabrico tiles, sample data.