


 Login
 Blog
Computer Vision for Plastic Extrusion: Catch Miscounted Bundles, Coils and Rolls

In short: computer vision in plastic extrusion earns its keep as a counter: a camera add-on counts packed bundles and wrapped rolls, where totals drift.
Wall thickness, film gauge and gels stay with gauges and web inspection; Fabrico does no inspection, and its camera add-on only tells OEE what left the line.
- The miscounts in this audit sit after the saw and the winder: double bundles, unlogged start-up scrap, crop cuts and regrind counted twice.
- Each miscount gets a fix and an owner: the saw for lengths, the coiler for metres, the cradle camera for bundles, the lab for holds.
- In the example night shift the sheet says 85.3% OEE, the audit says 80.0%, and EUR 675 of output is lost while orders wait.
- Fabrico's camera add-on counts output only, and the operator still adds the stop reasons.
The haul-off metre counter is the number an extrusion line trusts most, and it is not what the plant ships. After the saw, lengths become bundles, coils and rolls, scrap goes to the granulator and comes back as feed, and some packed product waits on a lab result. Each step can bend the shift total where the PLC never looks.
This is an audit of those miscounts on pipe, profile, sheet and film lines: the table first, then each row with its fix and its owner, then a priced night shift.
The miscount table: nine ways extrusion output is misreported
Use it as a checklist against one week of shift sheets.
| Miscount | Lines | Fix | Station that owns the count |
|---|---|---|---|
| 1. Metres, lengths and coils added into one total | All | One unit per product, converted where the unit is made | Haul-off for metres, saw for lengths, coiler for coil metres |
| 2. Start-up and purge scrap never logged | All | Own loss code; scrap counted or weighed per start-up | Operator at the scrap rack, saw as cross-check |
| 3. Crop cuts counted as good lengths | Pipe, profile | Crop flag at the saw | Saw |
| 4. Short coils counted as full coils | Small-bore pipe | Coil metres, not coils | Coiler length counter |
| 5. Regrind fed back and counted twice | All | Output counted at packing, never as extruder kilograms | Cradle, winder or stacker |
| 6. Edge trim recycled inline read as output | Film, sheet | Trim kilograms booked as a separate input | Winder and trim system |
| 7. Held bundles and rolls called good on the day | Pipe, film | Good only on release | Lab release |
| 8. Handover bundle counted by both shifts | Pipe, profile | Count the strap event and its time | Cradle camera add-on |
| 9. Reprinted lengths counted as reject and as good | Pipe, profile | Rework, counted once, priced at crew time | Gauge and print station |
Rows 1, 4 and 6 add numbers in different units. Rows 2, 3 and 5 hide scrap, so quality looks better than it is. Rows 7, 8 and 9 count product twice, or as good too soon. Two numbers settle almost every row: metres made, from the haul-off encoder, and metres packed, from the station where product leaves the line. The audit explains every metre of the gap.
Explainer presented by Iris, Fabrico's AI-generated presenter: how an add-on camera counts output where a machine has no signal. Book a demo.
Plays from YouTube. Google may set cookies when you press play. Privacy policy.
Counting rule one: metres, lengths or coils, one unit per product
Extrusion makes a continuous product and ships it in pieces. The Plastics Pipe Institute’s PE pipe handbook says the pipe extrusion line generally consists of the extruder, die, cooling systems, puller, printer, saw and take-off equipment, and explains why one plant ships in two units: most pipe of four inches or smaller can be coiled, in lengths of up to 10,000 feet, while larger pipe is usually cut into lengths of 40 to 50 feet and bundled before the truck or railcar.
So a line that runs 32 mm coils on Monday and 110 mm lengths on Tuesday changes its unit with its die. Add coils to lengths and the weekly total means nothing. Set one planning unit per product and convert where the unit is made:
- Straight pipe and profile: lengths from the saw, metres from lengths times cut length.
- Coiled pipe: metres from the coiler’s length counter, never a coil count.
- Profile in boxes: pieces per box times piece length.
- Film and sheet: kilograms from the winder or a roll scale; rolls are only the handling unit.
The OEE method per line type is in OEE for pipe and profile extrusion and OEE for blown film extrusion; why total and good output are counted at different points is in good count versus total count.
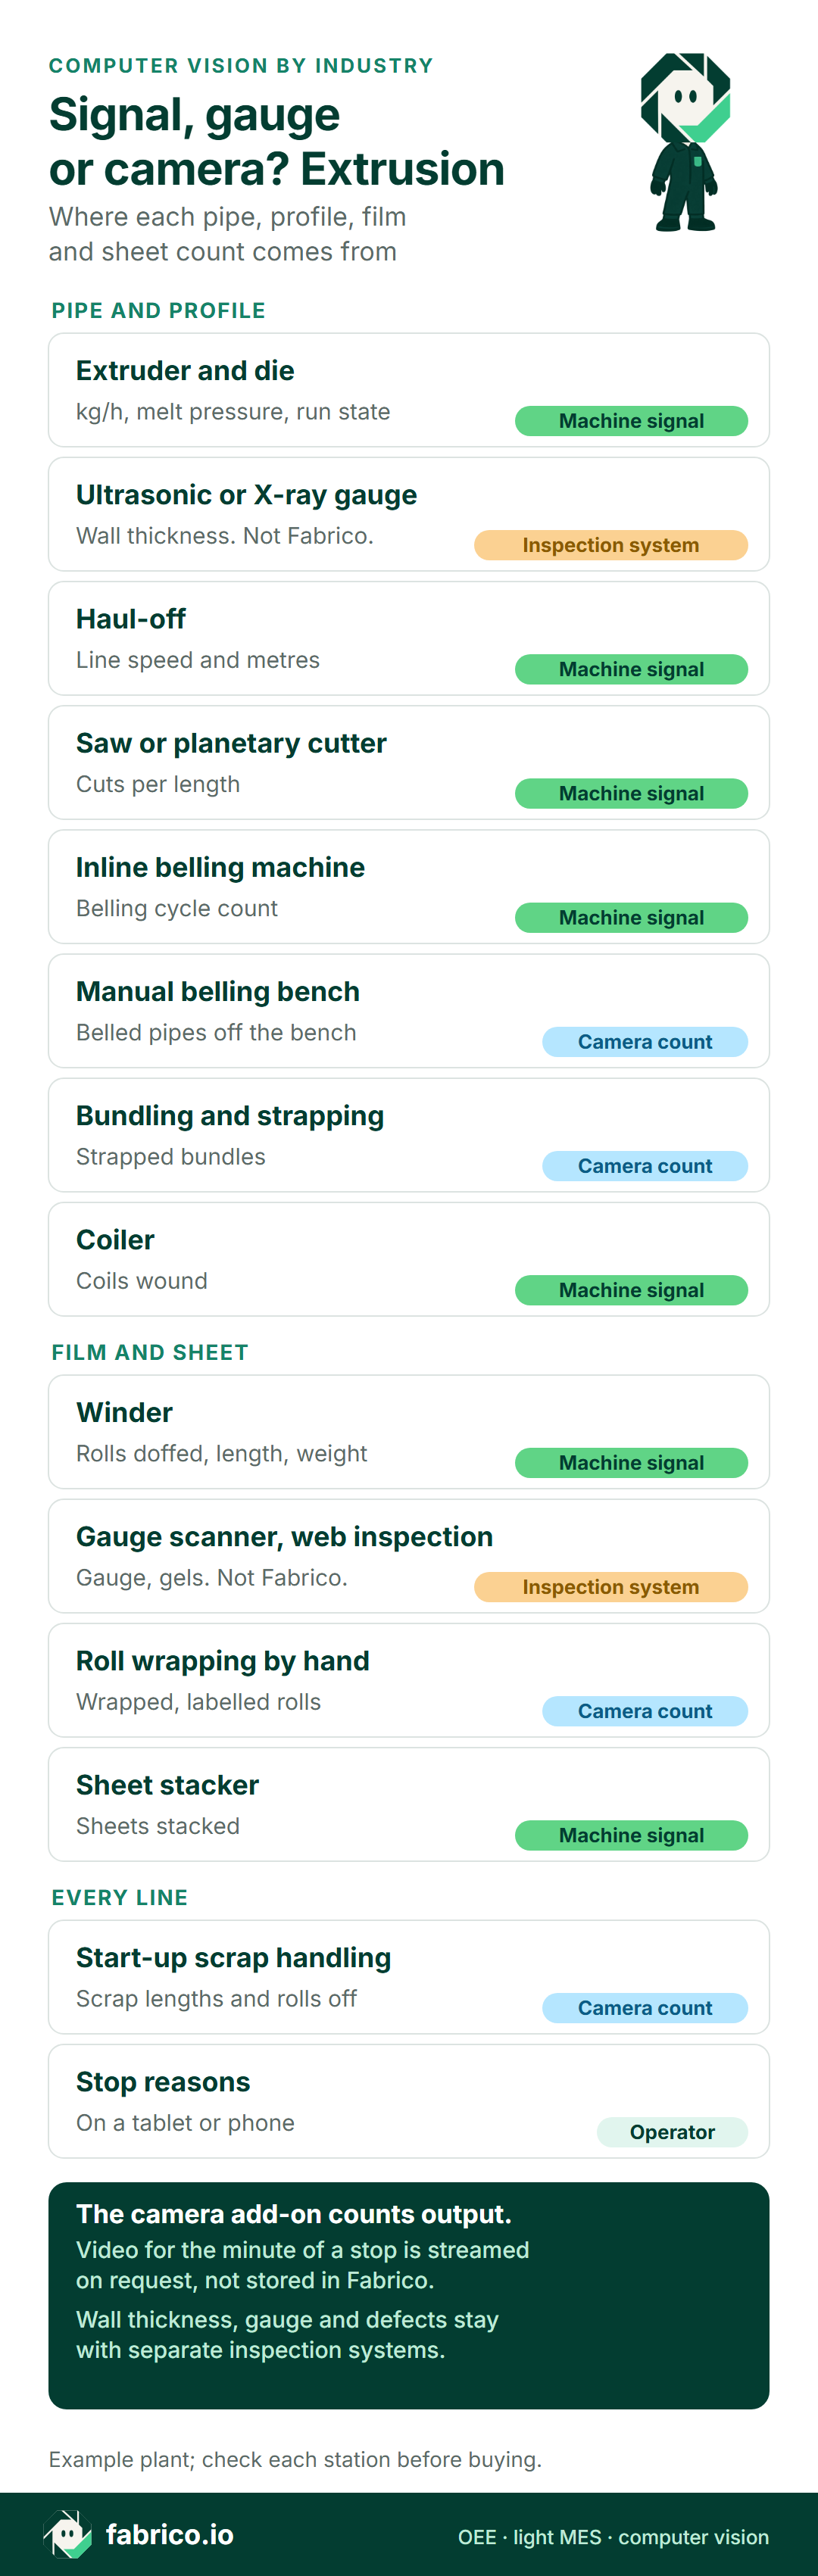
Text version of this infographic
- Pipe and profile: extruder and die: machine signal, kg/h, melt pressure, run state
- Pipe and profile: ultrasonic or X-ray gauge: inspection system, wall thickness, not Fabrico
- Pipe and profile: haul-off: machine signal, line speed and metres
- Pipe and profile: saw or planetary cutter: machine signal, cuts per length
- Pipe and profile: inline belling machine: machine signal, belling cycle count
- Pipe and profile: manual belling bench: camera count, belled pipes off the bench
- Pipe and profile: bundling and strapping: camera count, strapped bundles
- Pipe and profile: coiler: machine signal, coils wound
- Film and sheet: winder: machine signal, rolls doffed, length, weight
- Film and sheet: gauge scanner, web inspection: inspection system, gauge and gels, not Fabrico
- Film and sheet: roll wrapping by hand: camera count, wrapped and labelled rolls
- Film and sheet: sheet stacker: machine signal, sheets stacked
- Every line: start-up scrap handling: camera count, scrap lengths and rolls taken off
- Every line: stop reasons typed by the operator at the line
- Camera add-on: counts output only; video for the minute of a stop is streamed on request, not stored in Fabrico
- Wall thickness, gauge and defects stay with separate inspection systems
- Example plant; check each station before buying.
The audit priced: one night on a 110 mm pipe line
Example inputs, not a real plant. A line makes 110 mm PE pipe in 6 metre lengths, strapped in bundles of 20. The night runs 22:00 to 06:00; less a half-hour break, 450 minutes are planned. At a rated 5 metres a minute, 2,250 metres are possible. At 06:00 the sheet said 16 bundles, one screen change and 10 gauge rejects. The audit checked each line against its owner:
| Count | Shift sheet | Audited | Owner |
|---|---|---|---|
| Bundles packed | 16 | 15: bundle 16 was strapped at 21:50 by the evening shift | Bundling cradle, camera add-on |
| Packed metres | 1,920 | 1,800 (15 x 20 x 6 m) | Cradle count x lengths per bundle |
| Start-up scrap after the screen change | Not logged | 90 m, 15 lengths, sent to the granulator | Operator at the scrap rack |
| Gauge rejects | 10 lengths | 10 lengths, 60 m | Ultrasonic gauge |
| Saw cuts | Not used | 325 = 300 packed + 15 start-up + 10 rejected | Saw |
| Stops | Screen change 20 min | Screen change 20 min, saw blade change 10 min | PLC, reason by the operator |
| OEE | 85.3% (1,920 of 2,250 m) | 80.0% (1,800 of 2,250 m) | All of the above |
The haul-off logged 1,950 metres, 325 lengths, and the saw agrees: 300 reached the cradle, 15 were start-up scrap, 10 were rejects. The extra bundle was row 8, strapped and counted by the evening shift, then counted again. The 90 start-up metres were row 2, ground without a note.
Availability. The screen change stopped the line for 20 minutes and a saw blade change for 10: 420 of 450 minutes, 93.3%.
Performance. 420 running minutes could make 2,100 metres. The haul-off logged 1,950, so 150 metres, 30 minutes, went to slow running: 92.9%.
Quality. The camera add-on counted 15 bundles, 1,800 metres. The other 150 metres were 90 of start-up and 60 of rejects: 1,800 of 1,950 is 92.3%.
OEE. 93.3% x 92.9% x 92.3% = 80.0%, and 1,800 of 2,250 possible metres is 80.0%. The sheet’s 85.3% was 5.3 points high, from one bundle counted twice and one start-up never logged.
Money. As a price anchor, a UK merchant lists 110 mm x 10.0 mm SDR11 PE100 pipe at £18.22 a metre before VAT. A merchant’s gross price sits above what an extruder earns, so the example takes a cautious contribution margin of EUR 1.50 a metre, which the plant replaces with its own. While 110 mm orders wait, each lost metre is lost margin: stops 150 metres, EUR 225; slow running 150 metres, EUR 225; start-up scrap 90 metres, EUR 135; rejects 60 metres, EUR 90. Total: 450 metres, EUR 675 for the night.
The sheet would have shown 330 lost metres, EUR 495. The audit adds EUR 180 and, more usefully, makes the post-screen-change start-up a named, priced loss that points at how the die returns to tolerance, not at the packers. With an empty order book, lost metres cost crew time and energy, not margin. Fabrico prices losses the same way, from the plant’s own price or margin per product.
Make it weekly: put made, packed, scrap and held columns in the shift production report and have the shift lead sign off the gap.
Start-up and purge scrap that never reaches a log
Every start-up, die, colour and screen change makes material that is not product: purge, the first metres through the die, and lengths cut before wall and diameter are in tolerance. It is slow on purpose. HSE guidance for extruder lines says to carry out purging at slow speed and reduced pressure, and while the haul-off is fed by hand, "The extruder should be operated at the slowest speed practicable for the product." Book those minutes as start-up, not slow running.
The miscount: the scrap goes straight to the granulator and nobody writes it down, so quality looks near perfect. The haul-off knows better, because it counted those metres too. The fix:
- A start-up loss code for start-up, die, colour and screen changes, entered by the operator against the stop.
- Scrap counted per event at the scrap rack, with purge lumps weighed, up to the first length in tolerance.
- A saw cross-check: cuts in the start-up window, less lengths that reached the cradle, match the scrap rack count.
Ways to shorten start-ups are in cutting start-up and shutdown losses; a code list that keeps purge, start-up and gauge rejects apart is in these scrap reason codes, and a written routine in line start-up standard work.
Crop cuts and short coils: count once, at the cradle
The saw counts every cut, including crops: the first cut after threading, the squaring cut after a length change, the short end of a run. Take the length count from the saw and every crop becomes a good length. Flag crops at the saw, and take the OEE length count at the cradle, where a crop never arrives.
Coils hide the same error. A coil cut short by a die change is still one coil. If the plan says 100 metre coils and three ran 60, 75 and 40 metres, a coil count overstates output by 125 metres. The coiler’s length counter has the true figure. Profile offcuts work the same way: book them as scrap at the cutting table and count full boxes at packing.
Regrind and edge trim: the same kilogram, twice
Start-up lengths, crops and rejects go to the granulator, and the regrind goes back into the hopper. Read output as kilograms through the dosing unit or the extruder and the same kilogram counts once when first extruded and again when it returns. With many start-ups, kilograms extruded can rise while metres packed fall.
Count output only at packing, in the planning unit, and report regrind kilograms as an input. The granulator then works as a scrap meter.
Film and sheet lines feed edge trim straight back, and the blown film OEE guide notes that some plants count it as neither good nor scrap. Pick one rule per line and keep trim kilograms on their own report line.
Rules can decide where regrind may go. Under the US federal gas pipeline rule, rework and/or regrind material is not allowed in plastic pipe produced after March 6, 2015 for use under that part, so on US gas pipe runs start-up scrap is a real material loss, not a loop.
Pellet handling has its own EU rule as well. The EU plastic pellets regulation (EU) 2025/2365 applies to installations that handle five tonnes or more of plastic pellets a year, converters included: operators must avoid, contain and clean up spills and keep a risk management plan, and sites above 1,500 tonnes a year need a certificate of compliance or a permit. A plant that already logs start-up scrap and regrind per event starts that plan from records rather than estimates.
Held bundles and rolls: a counting rule for release
ASTM D3035 for PE pressure pipe requires pipe to conform to requirements for workmanship, dimensions, sustained pressure, hydrostatic burst pressure, tensile strength at yield and environmental stress cracking, and the PPI handbook notes that the standards specify the type and frequency of quality control tests that are required. Some results arrive after the making shift has gone home.
So the sheet calls every strapped bundle good, the lab rejects a batch two days later, and the report for that night still shows 100% quality. The fix is a hold status: count bundles and rolls as made when strapped or wrapped, flag them while held, and call them good only on release. A later reject is booked back to the shift that made it. The lab owns release; the cradle owns the count.
See how quality holds and release sit next to OEE. Reprinted lengths, row 9, are rework: counted once as good, the reject not counted again, the reprint priced at crew time, as in whether rework counts as good.
Film and sheet lines: doffs, transition film and wrapped rolls
On blown and cast film the winder PLC knows when it doffs a roll, and often its length and weight. The film miscounts:
- Transition film from a colour or gauge change is wound, so the winder counts it as a roll. It needs its own reason and a scrap or second-grade code.
- Scrap rolls after a bubble break look like product at the doff. Count them where they are taken off, and book them as scrap, not rework (see scrap vs rework).
- Rolls wrapped by hand leave with no count. A camera add-on at the wrapping station counts them.
Sheet lines end at a stacker or winder that usually reports; the audit there is the trim loop and manual palletising. Converting is covered in computer vision for packaging converters, moulding in computer vision for injection molding, and cable insulation in computer vision for wire and cable.
Who owns each count: machine signal, gauge, camera or lab
One example pipe line from hopper to yard. After the saw the flow splits: good lengths to the cradle, scrap to the rack and the granulator, regrind back to the hopper.
The haul-off owns metres made, the saw owns lengths and crops, and the gauge owns rejects; it stays its own system and its signal only tells OEE which lengths to take off. The cradle owns bundles packed, and is usually the one station with no electronic count, which is why the camera add-on goes there. If cradle plus scrap rack does not equal the saw count, a length went unlogged. If the granulator takes in more than the rack sent, scrap skipped the count. A hand belling bench, unlike an inline belling machine, needs a count too.
What a camera can count at the cradle, and what it cannot
A counting camera is good at events: a strapped bundle crossing a line, a wrapped roll leaving the table. It is much worse at items hidden in a pile. A peer-reviewed study of densely packed scenes, CountNet3D at IEEE/CVF WACV 2023, states that "the performance of 3D object detectors can suffer in scenarios where extreme occlusion of objects is present". The authors’ own 3D point-cloud method still reports "an error rate of 11.01%" on real scenes with extreme occlusion.
The study covers retail and inventory scenes, not pipe, and a 3D method, not a camera over a cradle. Its lesson still holds: counting 20 pipe ends inside a bundle is hard, and one error in nine would wreck the audit. So design the count around clear events:
- Count the strap, not the pipes. One strapped bundle leaving the cradle; lengths per bundle come from the product setup, and the saw checks the total.
- Keep hands and forklifts off the counting line. A packer leaning in or a forklift lifting a bundle can hide the event.
- Plan for water, steam and glare. Spray, steam off the cooling bath and wet black pipe cut contrast; use a water-rated housing mounted outside the guarding.
An OEE camera does not measure wall thickness, ovality, film gauge or gels; gauges and web inspection do, and their reject signals feed quality.
The cradle is where the packers are. Tell the team, and the works council where one exists, before a bracket goes up. In Germany Section 87 of the Works Constitution Act gives the works council a right of co-determination over technical devices designed to monitor the behaviour or performance of employees. Point the lens down at the bundle and publish counts per line and shift, never per packer.
Where Fabrico fits in the audit
Fabrico is cloud OEE software with light MES functions. In this audit it holds both sides of the gap on one shift timeline:
- Metres made. Run state, metres, cuts and rolls come from the extruder, haul-off, saw, coiler and winder PLCs, so a start-up or a screen change lands on the timeline as a stop that waits for its reason.
- Output packed. At bundling cradles, hand belling benches and roll wrapping, the camera add-on counts strapped bundles, belled pipes and wrapped rolls. Where a camera add-on covers the station, the video for the minute of a stop can be opened from the shift timeline, streamed on request and not stored in Fabrico.
- Rate and unit per product, in metres a minute or kilograms an hour, so packed output is read against what that die should make.
Operators and shift leads enter the stop reasons themselves, on a tablet or phone at the line. OEE and losses appear per line and shift, with lost output priced in money, in a browser or the iOS and Android apps. Data goes to the ERP over a REST API or webhooks, or out as Excel and CSV.
Roadmap, not live today: a camera add-on that spots a stalled bundling cradle unprompted and suggests a likely stop reason for the operator to confirm.
Left to other systems: wall thickness gauging, film gauge scanners, web inspection, dosing and line control, lab testing and the resin lot record.
Put four audit questions to every vendor:
| Question | What a good answer shows |
|---|---|
| Which unit is each product planned in? | Metres, coil metres or kilograms per product, never one unit per line. |
| Where does packed output come from? | A count at the cradle, wrapper or stacker, separate from haul-off metres. |
| Is regrind ever counted as output? | No: regrind kilograms are booked as an input, apart from output. |
| How does a held bundle become good? | A hold flag, good on release, a later reject booked to the making shift. |
See Fabrico computer vision for OEE, how a camera add-on count becomes availability, performance and quality in OEE with computer vision, and extrusion next to moulding in OEE in plastics manufacturing.
Want the audit on one screen every shift? Book a demo to see haul-off metres, packed bundles and start-up scrap counted on one timeline.
Extrusion miscount questions
Where should an extrusion plant put its first counting camera?
Where finished product leaves with no electronic count: usually the bundling cradle on a pipe line or the hand wrapping station on a film line. The extruder, haul-off, saw, coiler and winder already report through the PLC.
Can an OEE camera measure wall thickness or find film defects?
No. Ultrasonic or X-ray gauges measure wall thickness, gauge scanners measure film, and web inspection finds gels and holes. Fabrico does no inspection; reject signals from those systems still lower the OEE quality figure.
Should regrind count as output in extrusion OEE?
No. Regrind is earlier scrap fed back as raw material. Count output at packing and report regrind kilograms as an input, or the same material is counted twice.
How do you stop crop cuts inflating the length count?
Flag crop cuts at the saw and take the OEE length count at the cradle, not at the saw.
When does a held bundle count as good?
Only on release by the lab. Count it as made when strapped, flag it while held, and book a later reject back to the shift that made it.
Want your haul-off metres and packed bundles to agree? Book a demo to see bundles, coils and wrapped rolls counted against the metres the line made.
Related articles




Real Fabrico tiles, sample data.