


 Login
 Blog
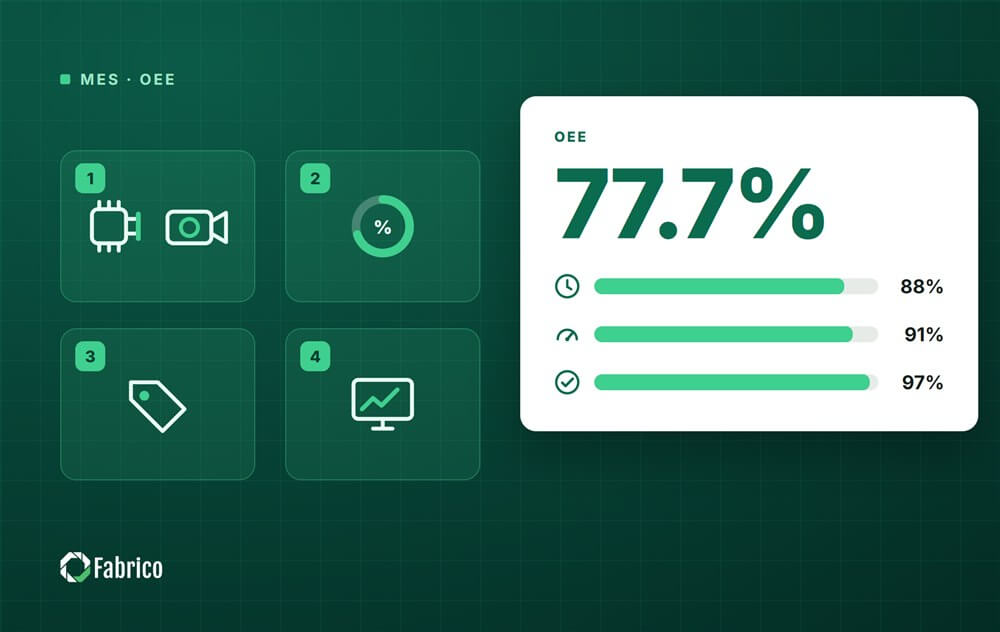
OEE Monitoring Software: How an OEE Monitoring System Works
Choose an OEE monitoring system by how each machine will report run, stop and count, not by the dashboard. The right one takes that data from the PLC or a sensor, shows short stops and slow cycles on their own, gets the stop reason from the operator, and shows OEE by line and shift while the shift can still act.
Fabrico, our product, is a cloud-based OEE and light MES platform with maintenance (CMMS) built in. Routings, BOMs, dispatching and genealogy stay in the ERP, so Fabrico is not the pick if you want those in one system.
Most plants already know their OEE. The trouble is when they learn it: at the end of the shift, from a spreadsheet. This guide covers how an OEE monitoring system works, how to connect machines with and without a PLC, where cameras fit, and what to ask each vendor.
What is OEE monitoring?
OEE monitoring is the live measurement of overall equipment effectiveness on each machine, line and shift. Instead of calculating OEE after the fact, the system records runs, stops and parts on connected machines as they happen and keeps the three factors current:
- Availability: run time against planned production time, with breaks and non-production time taken out.
- Performance: actual output against what the ideal cycle time allows in the run time, so slow cycles and micro-stops show up.
- Quality: good units against all units produced.
OEE tracking and OEE monitoring are often used as the same thing. In practice, tracking is the record and monitoring is the live view built on it: a shift lead who can see that Line 2 has lost twenty minutes to short stops since 6:00 can still do something about it today.
How an OEE monitoring system works
An OEE monitoring system does four jobs. If one of them is missing, the number on the screen stops being trusted.
- Capture: it collects a running or stopped state and a part count from each machine, through a PLC connection or an added sensor. Where there is no machine signal, the count can come from an AI camera (an add-on in Fabrico) or from operator input.
- Calculate: it compares that data with the shift plan and the ideal cycle time to produce availability, performance, quality and OEE, by machine, line and shift.
- Explain: it asks for the reason behind each stop, so downtime builds up by cause instead of as one large unknown. Our comparison of machine downtime tracking software shows how five tools handle it.
- Show and act: it puts the result where decisions are made: a screen on the line, the shift handover, the daily review and the maintenance queue.
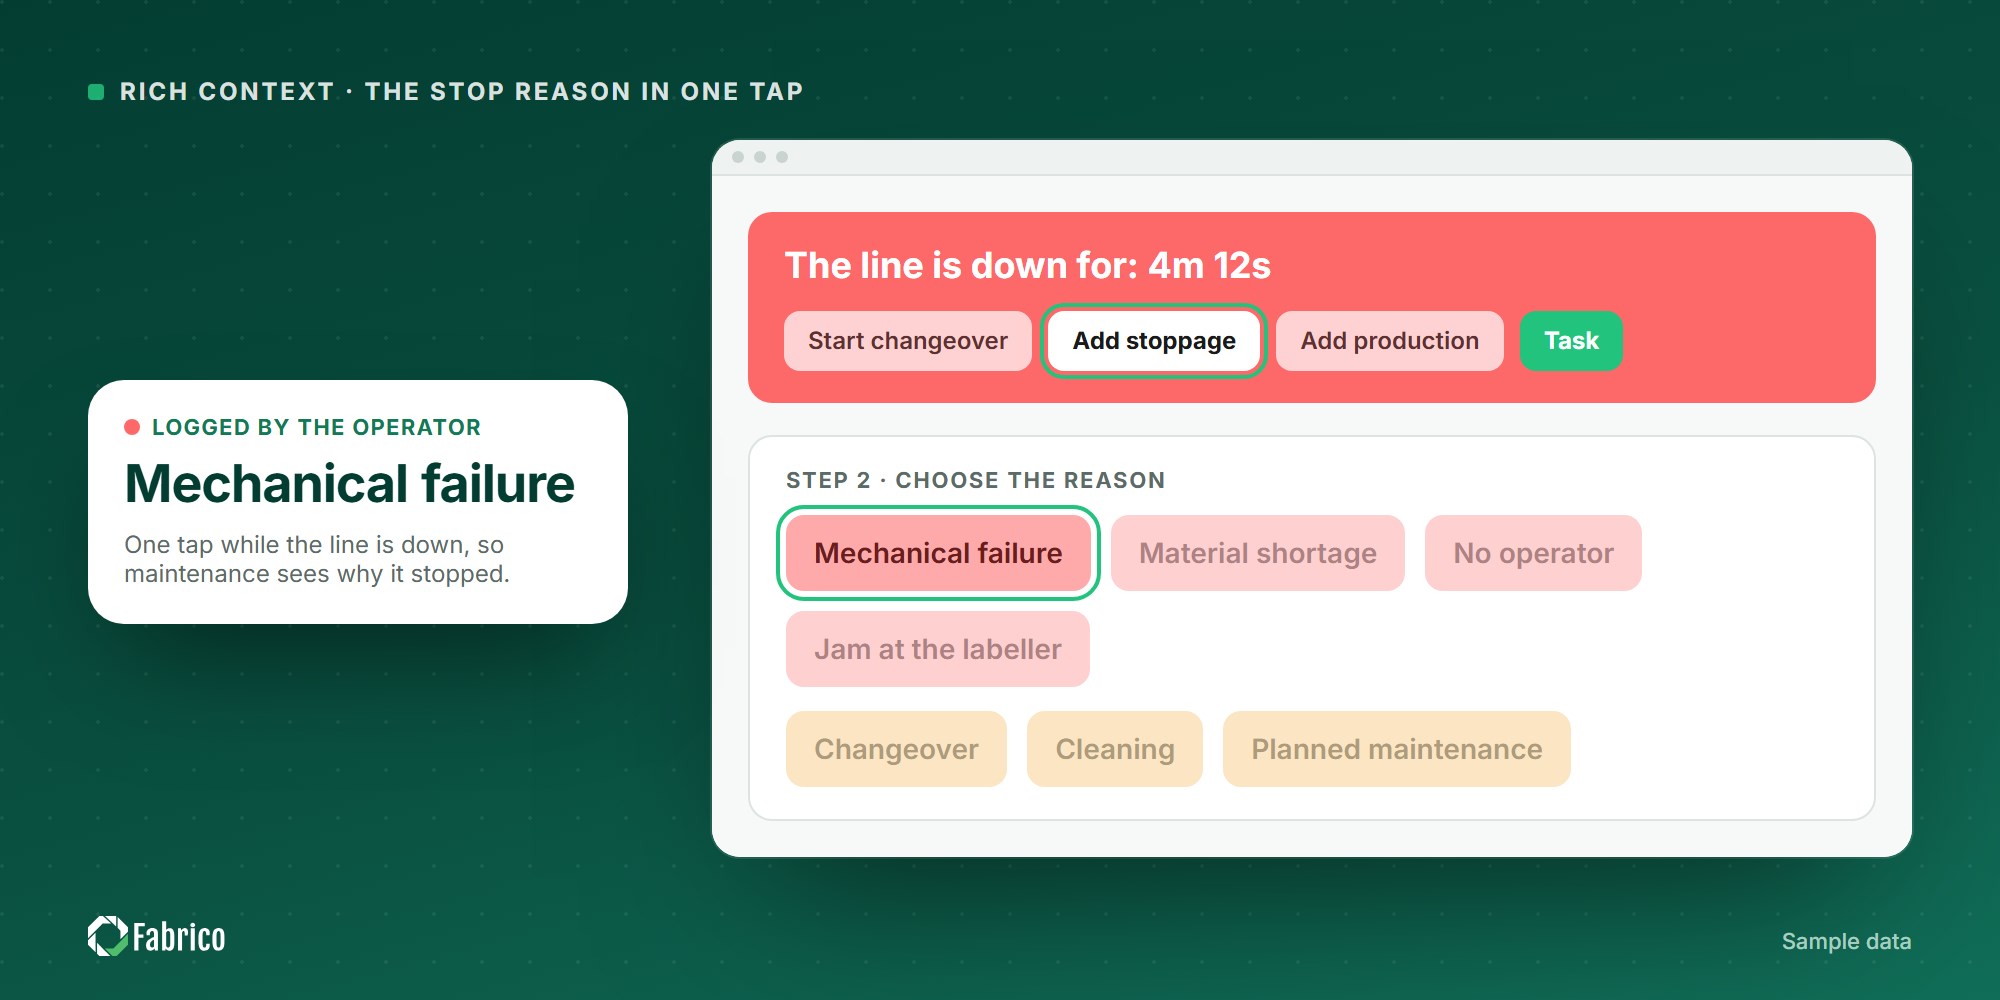
The capture step decides how good everything after it can be, which is why the choice of data source matters more than the dashboard.
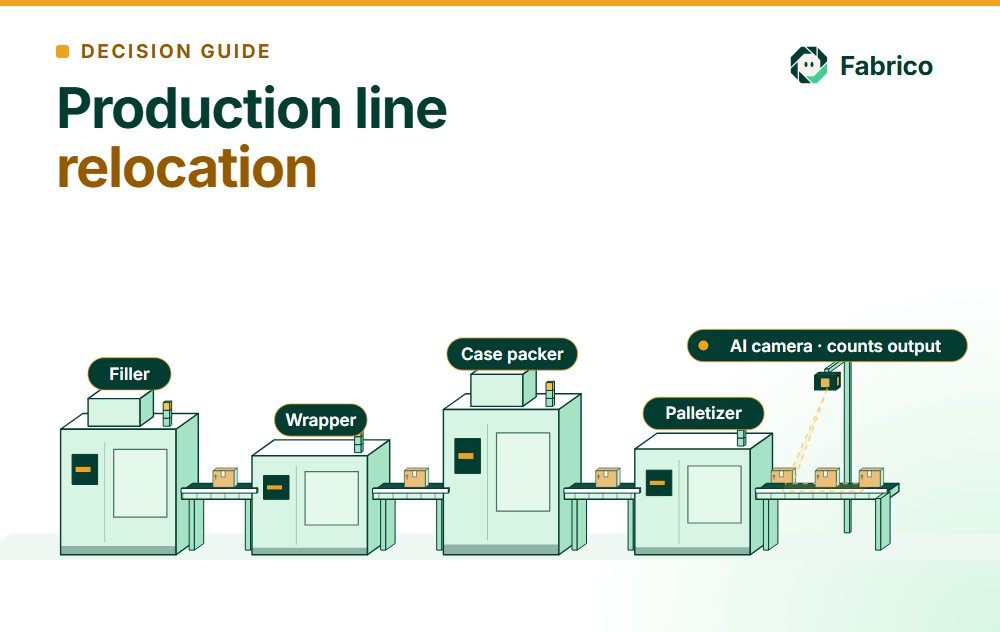
Where a machine gives no signal, the AI camera (an add-on) can count parts. If you are weighing cameras, see the camera buyer checklist, how to connect line cameras to MES downtime codes, how to run a camera OEE pilot and how the Cerrion alternatives compare.
Three ways to connect machines
A plant rarely has one kind of machine, so most OEE monitoring systems support more than one way in. One plant can mix all three. Operators add the stop reason on a tablet or phone whichever route a machine uses.
| Data source | Fits | What it gives you, and what to check |
|---|---|---|
| PLC connection | Modern machines with a controller you can read | Gives: run and stop states, counts and, often, fault codes. Check: who maps the signals, and whether the PLC program has to change. |
| IoT device with sensors | Older machines with no PLC you can read | Gives: running and stopped states and cycles from an external sensor. Check: where the sensor sits, so a cycle is counted once. |
| AI camera (an add-on in Fabrico) | Stations with no machine signal | Gives: a part count. You can open the camera video for that minute on the timeline. Check: camera position. In the standard setup, camera video is streamed, not stored in Fabrico. |
For machines with no PLC at all, our guide to OEE monitoring without a PLC compares sensors and cameras in more detail.
Where cameras fit in OEE monitoring
Machine signals tell you whether a machine is running, and in Fabrico stops come from those signals. The AI camera (an add-on) has a narrower job.
- Output: it counts parts where there is no machine signal.
- The moment of a stop: you can open the camera video for that minute on the line's timeline.
- The reason: the operator gives it, on a tablet or phone. Suggested stop reasons are on our roadmap, not in the product today.
In the standard setup, camera video is streamed, not stored in Fabrico. If any vendor tells you a camera finds stops or their causes, ask to see it on a stop they did not stage. Our explainer on visual intelligence in manufacturing covers the wider use of video on the shop floor.
What an OEE monitoring system should show while the shift runs
- OEE by machine, line and shift, split into availability, performance and quality, so you can see which of the three is pulling the score down.
- Stops with their start time, duration and reason, including micro-stops detected from the signal.
- Slow cycles shown as performance loss, not hidden inside run time.
- Output against target hour by hour, on a screen the line can see.
- The top losses of the shift, ranked, so the handover starts with the biggest one.
- Losses in money as well as minutes, because a stop on the bottleneck costs more than a stop on a machine with spare capacity.
A worked example (sample numbers)
Take one line on an eight hour shift with a 30 minute break, so 450 minutes of planned production time. The monitoring system records 54 minutes of stops: one jam of 14 minutes, a changeover of 22 minutes and a run of short stops that adds up to 18 minutes. The ideal cycle time is 0.2 minutes per part, the line made 1,800 parts and 54 of them were scrap.
- Availability: the jam and the changeover take 36 minutes, so run time is 414 minutes out of 450 = 92%. The short stops stay inside run time.
- Performance: 1,800 parts × 0.2 minutes = 360 minutes of ideal time out of 414 minutes of run time = 87%. The 18 minutes of short stops show up here.
- Quality: 1,746 good parts out of 1,800 = 97%.
- OEE: 0.92 × 0.87 × 0.97 = 77.6%.
The calculation is the easy part. The value of monitoring is that the 18 minutes of short stops appear during the shift as their own loss, with a time stamp. Where an AI camera (an add-on) covers the line, you can open the camera video for that minute. Written down at the end of the shift, they would have been "other". For the formulas behind each factor, see our guide to OEE calculation.
OEE monitoring, OEE software and MES: how they relate
OEE monitoring software is the part closest to the machine: data capture, the live OEE, downtime by cause. A full manufacturing execution system adds functions around it, such as work instructions and traceability. Many plants start with monitoring and downtime on one line and keep routings, BOMs and dispatching in the ERP, which is the idea behind a light MES. If you are weighing the two, our comparison of OEE and MES sets out where each one starts and stops.
How to choose OEE monitoring software
Ask every vendor the same questions, about one specific line in your plant:
- How will each machine on this line report run, stop and count, including the old ones and the manual stations?
- Do micro-stops and slow cycles appear on their own, or are they averaged into run time?
- How does an operator add the reason for a stop, and how long does it take on the floor?
- What happens to a stop nobody classified? Is there a way to see what happened?
- Can the system show the loss in money, with our selling prices and margins?
- Which screens does each role see: the line, the shift lead, the plant manager?
- When a stop needs maintenance, how does the request reach the technician?
- From which day will this line show live data, and what do we need to prepare?
Common mistakes with OEE monitoring
- Starting with the dashboard: a good looking screen fed by unreliable signals loses the team's trust. Start with capture.
- Too many stop reasons: on a long list, people pick the first reason. Keep it short enough to use with gloves on.
- Ignoring short stops: they rarely appear in manual logs, yet they count as performance loss.
- Monitoring without a review: the number only moves when someone owns the top loss each week.
- Connecting every line at once: one line, measured honestly, teaches more than ten lines with gaps in the data.
Where Fabrico fits
Fabrico is a cloud-based OEE and light MES platform. It shows real-time OEE (availability x performance x quality) per line and shift. Machine data comes from the PLC, from a Fabrico IoT device with external sensors on older machines, or from AI cameras (an add-on) that count parts where there is no machine signal. Connected machines report their own stops, including short stops too brief to log by hand, and operators add the stop reason on a tablet or phone.
Losses also show in money: revenue at risk and profit impact per loss, in real time. Maintenance (CMMS) is built in, on the same machine and production data, and a work order is opened from the stop in one step, linked to the line. EU clients are hosted on AWS in Frankfurt, Germany.
Installing the devices and connecting the machines takes about one month. Full rollout across the lines you choose takes 3 to 4 months. Quoted per plant. Start with a one-line pilot.
Book a demo to see Fabrico on lines like yours, or contact us with a question.
Frequently asked questions
Which OEE monitoring software should we choose?
The one that can report run, stop and count from every machine on your line, shows short stops and slow cycles on their own, and gets a stop reason from the operator quickly. Test those three before you compare dashboards.
What is the difference between OEE tracking and OEE monitoring?
OEE tracking is the record of runs, stops and counts over time. OEE monitoring is the live view built on that record, so the shift can react to a loss while it is still happening.
What is an OEE monitoring system?
It is the combination of data capture on the machines, the OEE calculation, the reasons for each stop and the screens and reviews that turn the numbers into action.
Can I monitor OEE on machines without a PLC?
Yes. Older machines can be fitted with an IoT device and external sensors, and AI cameras (an add-on) can count parts at stations with no machine signal. Operators give the stop reasons.
Do I need an MES to monitor OEE?
No. OEE monitoring is often the first step. A light MES covers machine data collection, production monitoring, OEE and downtime analytics, and leaves routings, BOMs, dispatching and genealogy in the ERP.
Does Fabrico keep camera video?
In the standard setup, camera video is streamed, not stored in Fabrico. You can open the camera video for that minute from the line's timeline.
How long does it take to start OEE monitoring with Fabrico?
Two stages. Installing the devices and connecting the machines takes about one month. Full rollout across the lines you choose takes 3 to 4 months.
See Fabrico on lines like yours.
Book a demoRelated articles

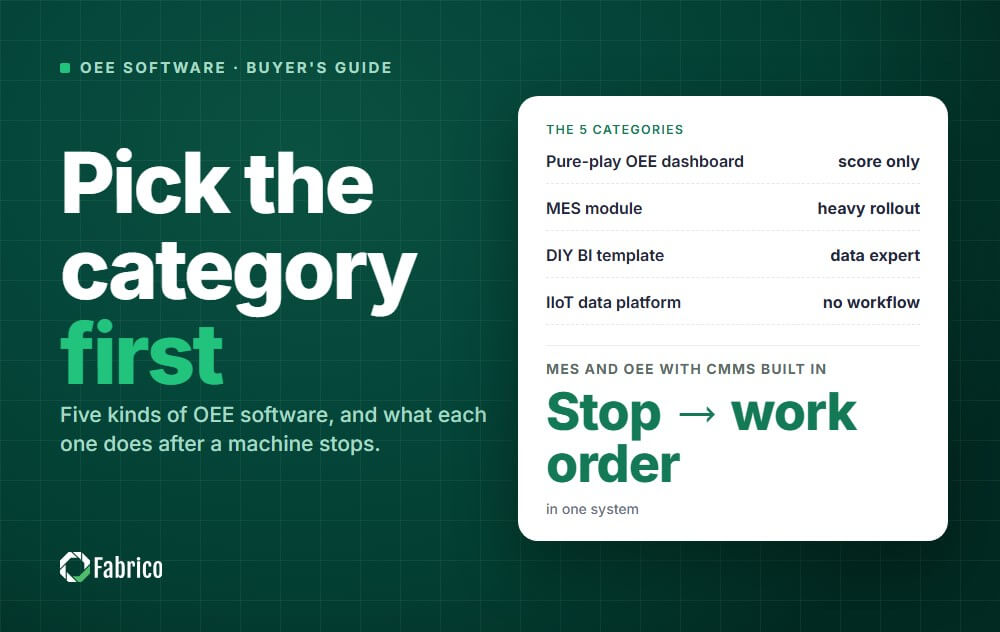


Real Fabrico tiles, sample data.