


 Login
 Blog
Computer Vision for Sauce and Condiment Lines: Jars, Bottles, Sachets

In short: computer vision on a sauce or condiment line earns its place where the count is weak or a stop is too quick to explain: case packers you cannot read, catering and promotion packs packed by hand, and the filler, capper and labeller, where you open the video of a stop.
- Fill weight, caps and vacuum, labels, codes, glass and metal are inspection jobs. They go to checkweighers, dud detectors, X-ray, metal detectors and vision systems, from makers such as Mettler-Toledo, Cognex or Keyence.
- The minutes go to product changes and allergen cleans, hot fill start-ups, nozzle wipes on thick product, cap feed jams and label faults.
- Where the filler and capper PLC already reports running, stopped and a count you trust, use that. Put cameras where it does not, and where a capper stop needs a picture.
- Fabrico's camera add-on gives a sauce line counts from stations with no signal and the video behind any minute of the shift. Operators pick the stop reason.
Ketchup, mayonnaise, mustard, dressings, pasta sauce, soy and hot sauce: one plant may fill them all, into glass jars, squeeze bottles, catering tubs and sachets. The product is thick or hot, often both, and the recipes carry different allergens.
This guide is for plant managers and engineers at sauce and condiment plants who are buying cameras and OEE software. Sauces retorted in cans or pouches follow the pattern in computer vision for canned food lines.
Below: which sauce stations earn a camera, which ones the filler signal already covers, and eight questions to put to vendors. We are one of those vendors, so apply the same questions to this page.
Computer vision for sauce and condiment lines: two different jobs
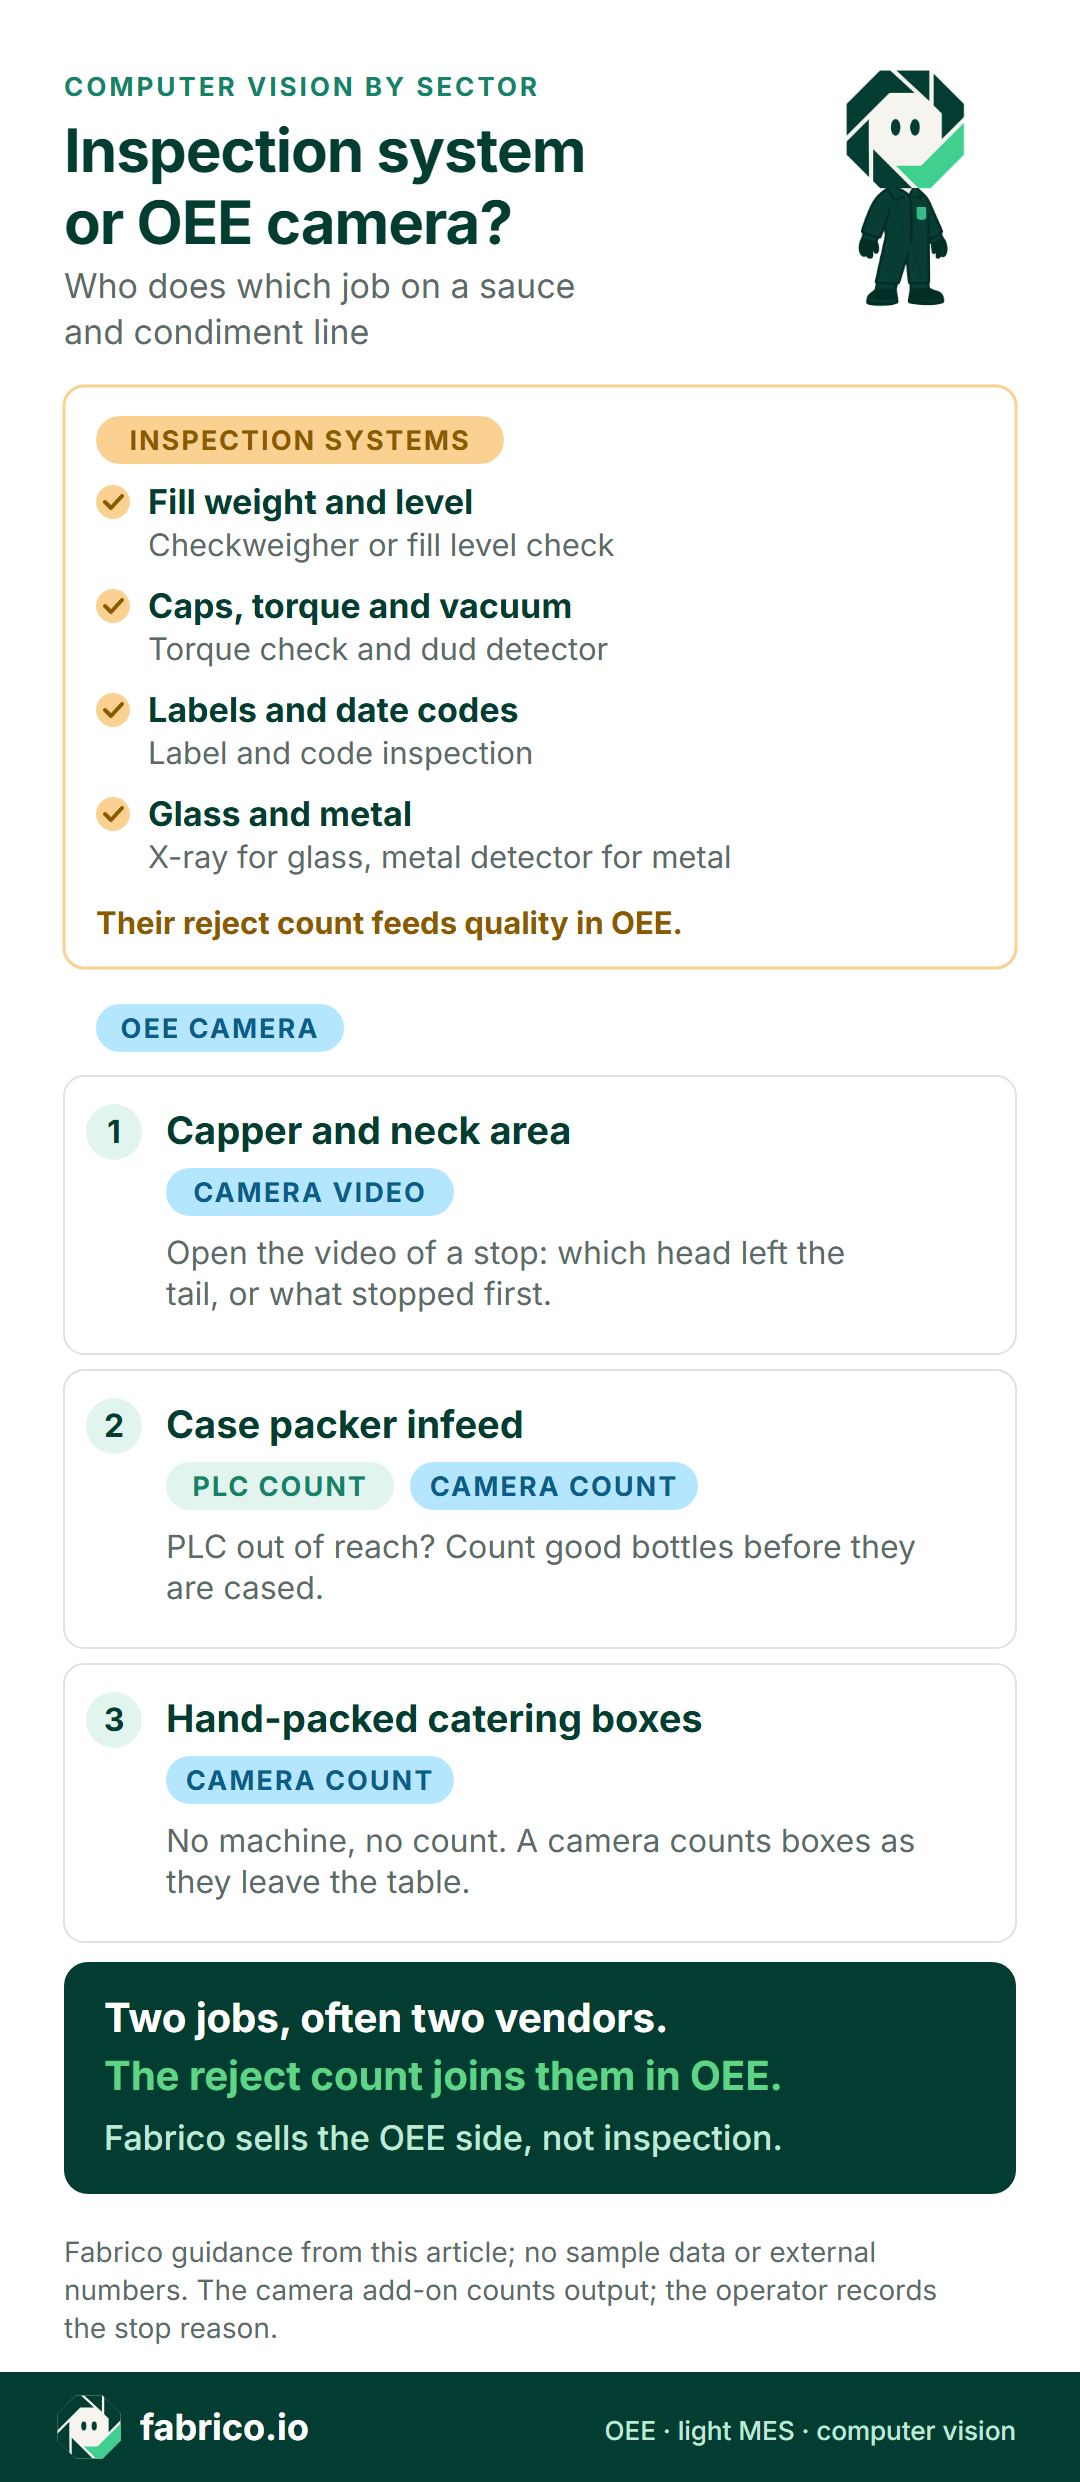
On a sauce line, vision can mean two systems. An inspection system looks at every jar or bottle and throws out the bad ones. An OEE camera counts what reaches a station and lets you replay the minute a line stopped. They are usually separate purchases, so spec them separately.
| Job on a sauce line | Inspection system | OEE camera |
|---|---|---|
| Fill weight and level | Checkweigher or fill level check | No |
| Cap, torque and vacuum | Torque check or dud detector | No |
| Label and date code | Label and code inspection | No |
| Glass and metal | X-ray for glass, metal detector for metal | No |
| Jars, bottles or boxes counted | Counts what it inspects | Yes, including hand tables |
| A capper or filler stop | Images of rejected items | Video of the minute it stopped |
| Reaches OEE as | Rejects, through quality | The good count |
Looked for machine vision for sauce bottling and found only inspection kit? This page is about counting.
The two meet in the quality figure. When the dud detector or the checkweigher sends its reject signal to OEE, each bad jar is counted once. For the boundary, see label and code vision vs an OEE camera.
Where a camera helps on a sauce line, and where it does not
Our page on OEE for sauce and condiment lines sets out the OEE rules. Here is where a camera helps, and where it does not.
Product changes and allergen cleans
Sauce plants change recipe often, and recipes on the same filler often carry different allergens. For England, Wales and Northern Ireland, the Food Standards Agency lists 14 allergens that food law requires businesses to declare. Many of them turn up in sauces: egg in mayonnaise (the US mayonnaise standard requires egg yolk), mustard itself, soya and often wheat in soy sauce, sesame in some dressings, milk in creamy sauces.
A change between recipes with different allergens means a validated clean; how to time the clean and the restart around it is on the OEE page. The machine signal and the count time both, and the operator picks the change type, so a camera adds little to the clean itself. See allergen changeover validation.
Hot fill and the start-up
Many sauces are acidic. In US rules, 21 CFR 114.3 defines acid foods as foods with a natural pH of 4.6 or below. It also leaves out of the acidified food rules acid foods, food dressings and condiment sauces among them, that contain small amounts of low-acid food and whose finished equilibrium pH does not differ significantly from that of the predominant acid or acid food. Which rules apply to your recipe, and the fill temperature it needs, is your process authority's or HACCP team's call. OEE software does not set it.
How to code the wait for product to reach temperature is on our page on OEE for sauce and condiment lines. Jars pulled at start-up count against quality, and a camera count of good jars at the case packer makes sure they do.
Heat matters for the camera too. Hot product, and the steam some cappers use to draw a vacuum, fog lenses. Mount cameras clear of the steam, never over open product, in housings rated for the washdown you run. For mounting angles and light, see camera placement and lighting.
Thick product, nozzle wipes and the capper
Mayonnaise is a thick emulsion, and US rules for mayonnaise say it contains not less than 65% vegetable oil by weight. Thick product leaves tails on necks, and the wipes that follow are too short for a paper log, so they hide in performance. Cap chute jams and torque faults stop the capper, and the filler stops behind it.
The PLC logs the stop. With a camera over the filler and capper, you open the video for that minute and see what the alarm could not tell you: which head left the tail, or whether the cap chute or the starwheel stopped first. The operator still adds the reason. See filler and capper stops.
Labels on sauced jars and bottles
Sauce on the outside of a jar or bottle makes labels skew, wrinkle or fail to stick. The labeller logs its own faults, and the video shows whether the cause came from the filler. See labeller OEE.
Glass breakage
A broken jar triggers the plant's breakage procedure, which runs as written. OEE records the minutes and the cause, and the video can show where the jar broke. It never replaces the procedure.
Sachets, catering boxes and hand packing
Portion sachets and stick packs run on multi-lane machines with their own loss pattern, from reel changes to a lane closed for half a shift. Our page on sachet and stick pack machine OEE covers it.
On some lines, sachets go into catering boxes by hand, and promotion packs and gift sets are packed at a table. Nothing counts them there. A camera over the table gives it an hourly count on the shift timeline, so a slow hour is visible while the shift is still running, and the crew there explain it. The camera spotting stops by itself is roadmap. See OEE at a manual packing station.
Where a camera goes on a sauce line
One example: a jar or squeeze bottle line with a case packer nobody can read, and a sachet room with a catering box table.
Machines not shown here are in camera or sensor for OEE, machine by machine.
Camera, sensor or operator: station by station
How a sauce and condiment plant usually splits it. Check each machine before you copy it.
| Station | Count and stops from | What a camera adds |
|---|---|---|
| Kitchen, hold tank, heat exchanger | Process control: temperature and level | Little. Use the signal. |
| Piston filler | Filler PLC | Video of nozzle wipes and neck tails at a stop |
| Capper | Capper PLC and torque | Video of the cap chute and the neck at a stop |
| Labeller or sleever | Labeller PLC | Video when sauce on the pack causes faults |
| Checkweigher, dud detector, X-ray, code check | Its own reject count | Nothing. Feed rejects to quality. |
| Sachet and stick pack machine | Machine PLC, by lane if you can | Video of film and seal stops |
| Case packer, shrink wrapper | PLC, if you can reach it | Count good bottles at the infeed if you cannot |
| Hand-packed catering and promo boxes | Nothing at a hand table | A count of boxes or packs where nothing counts |
| Stop reasons, all lines | The operator, on a tablet or phone | Video to settle a disputed reason |
Start where the count is weakest, then where short stops have no explanation.
Book a demo and bring your station list and a week of stop sheets from the filler and capper; we will go through them station by station.
Worked example: what the case packer camera adds
A filler count cannot see what the labeller and the checkweigher throw out after it. The shift below uses example numbers, not data from any plant.
An inline piston filler fills 400 ml squeeze bottles, mayonnaise first and an egg-free dressing after an allergen change, both at an ideal 70 bottles a minute. Its PLC reports running or stopped and counts the bottles it fills. The case packer's PLC is out of reach, so a camera at its infeed counts the bottles that reach it. Planned production time is 480 minutes.
Stops over the 2-minute cutoff took 96 minutes, most of them the allergen change and its restart, so availability is 384 of 480, or 80.0%. At 70 a minute, 384 minutes could make 26,880 bottles. The filler counted 22,848, so performance is 85.0%: 57.6 minutes of wipes, short stops and slow running.
The camera counted 21,938 good bottles. The other 910 went to reject at the labeller and the checkweigher, so quality is 96.0%. OEE is 80.0% x 85.0% x 96.0% = 65.3%, the same as 21,938 good bottles of 33,600 possible.
Without the camera, those 910 bottles get tallied by hand or not at all, quality reads 100% and OEE 68.0%. With it, a jump in label rejects on one SKU shows up in that shift's quality figure, not in next week's waste report.
Eight checks for any sauce line camera or OEE vendor
Ask every vendor these eight, us included, with last week's sauce shift as the test case.
| Ask | How to test the answer |
|---|---|
| How do you book an allergen clean? | Ask to see the validated clean as one step, and the restart to the first good bottle at speed as another. |
| Where do start-up rejects go? | Ask how jars filled too cool or pulled at start-up reach the quality figure, and who counts them. |
| What exactly does the camera count? | Jars, bottles, cases or catering boxes? Ask how cases and boxes convert to units for each SKU, and test it against a hand tally. |
| Does it cope with steam and washdown? | Ask which washdown rating the housing has, whether the lens window is shatterproof for your glass register, and what the count does when the lens fogs. |
| Where does each camera mount? | Ask for each position on a drawing, never above open product, and get QA sign-off first. |
| How do inspection rejects get in? | Ask whether dud detector, checkweigher and X-ray rejects reach quality, so no jar is counted twice. |
| Do nozzle wipes show up? | Ask to see stops under the cutoff in performance, by SKU. |
| Who can open capper video? | Ask where the video lives, who in the plant can open it, and for how long. |
Try it on one filler line before the whole plant. Our guide to a computer vision OEE pilot shows how, and how accurate a camera count is shows how to check the count against a hand tally.
Cameras, privacy and the works council
Fillers, cappers and labellers have operators beside them, and a camera over the capper will catch some of them. Before any camera goes up, tell the crew what it counts, and in many European countries, take it to the works council first.
Aim at the necks, the caps and the packing surface rather than the people. Keep reports at line and shift level, not per person. Then ask every vendor, Fabrico too, which privacy masking is live today and which is roadmap.
Fabrico's camera add-on counts jars and boxes, not people. More in production line cameras without surveillance.
Where Fabrico fits
Fabrico is a cloud platform for OEE and light MES. What it does on a sauce and condiment line today:
- Stops and counts: come from the PLC on the filler, capper or case packer, or from a sensor or counter.
- Stop reasons: the operator picks them on a tablet or phone at the line, so kitchen waits, wipes and cap jams stay apart.
- OEE and losses: OEE, downtime and losses for each line and shift, priced in money, in the browser and on iOS and Android.
- Camera add-on, on request: AI cameras count jars, bottles and boxes where no machine signal can, hand-pack tables included, and you can open the video for any minute on the shift timeline. In the standard setup, the video is streamed when opened and not stored in Fabrico.
- Your data: available through a REST API and webhooks, or as Excel and CSV files.
Roadmap, not live today: the camera finding stops on its own, jam zones on the video, and a camera suggesting the stop reason.
Outside what Fabrico does: inspection, hot fill temperature control and allergen clean validation, which stay with your inspection, process and food safety systems. Their rejects count in Fabrico's quality figure through a reject signal or counter on the line. Production planning is on our roadmap, with no release date. Today Fabrico does not build or schedule your plan: it shows what the lines can do.
The product page is Fabrico's computer vision add-on for OEE. For food and FMCG plants more broadly, read computer vision for food manufacturing and computer vision for FMCG manufacturing, and if you are comparing platforms, our guide to OEE software. The eight checks above apply to Fabrico as much as anyone.
Bring one shift with a product change from a filler and capper line to a demo, and see which of its numbers Fabrico fills and which it leaves blank.
What people ask next
Which station on a sauce line should get the first camera?
Start with the weakest count: a hand-pack table for catering or promotion packs, or a case packer nobody can read. The capper comes next if its short stops have no explanation. A filler whose PLC count you trust can wait.
Can a camera check fill level, caps and labels on sauce jars?
Yes, with an inspection system, which is a different product from an OEE camera. Fill level, caps and vacuum, labels and codes belong to inspection, and glass to X-ray. Fabrico does not sell inspection, but those reject counts can flow into OEE quality.
Does a camera cope with steam on a hot fill line?
It can, if it sits out of the steam path in a housing rated for your washdown, and QA signs off where it mounts. Test the count with a fogged lens before you trust it.
Can a camera count catering boxes packed by hand?
Yes. That is what Fabrico's camera add-on is built for: it counts boxes or packs as they leave the table, and the crew there give the reasons for slow hours. See OEE at a manual packing station.
Should a sauce line count jars or cases?
Count units at the filler for OEE, because it sets the pace, and count good units again before the case packer, so rejects at the labeller and checkweigher reach quality. Cases follow from the units per case for each SKU.
What does computer vision on a sauce line cost?
Each plant gets a quote. On a sauce line the drivers are how many filler and capper pairs and hand tables need a camera, steam and washdown housings, a shatterproof window for the glass register, the network to the hall, and training. Give every vendor the same station list.
Want to see it on a sauce line like yours? Book a demo and bring one shift with a product change in it.
Related articles











Real Fabrico tiles, sample data.